

Technical Parameters and Conveying System Process for Recycled Coke Powder
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of coke powder processing and conveying technology, specializes in providing comprehensive solutions for recycled coke powder handling. The company, operating from Shandong, China, is dedicated to optimizing the technical parameters and operational efficiency of coke powder systems through advanced engineering and material handling expertise.
Key Technical Parameters for Recycled Coke Powder
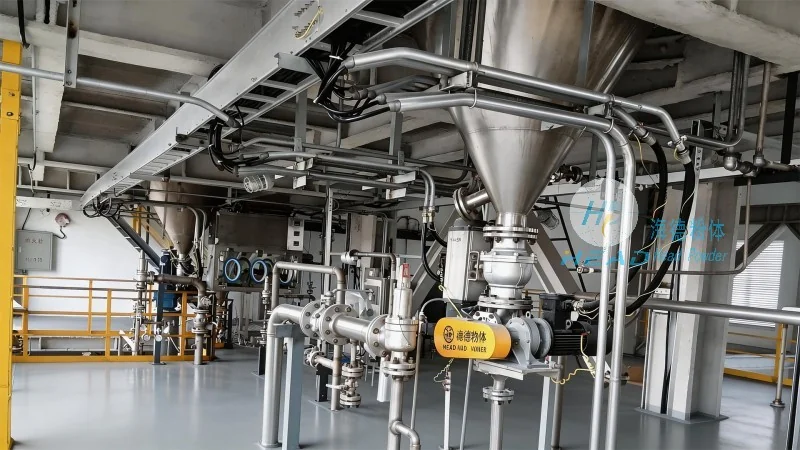
The technical parameters of recycled coke powder are crucial for ensuring the effectiveness and safety of the conveying system. Key parameters include particle size distribution, bulk density, moisture content, and chemical composition. Proper measurement and control of these parameters are essential to prevent blockages, ensure consistent flow rates, and maintain the quality of the coke powder during transportation. The company's engineering team conducts thorough analysis of these parameters to tailor the conveying system design to specific industrial requirements.
Conveying System Design and Components
The conveying system for recycled coke powder typically incorporates several key components to ensure reliable operation. These include feeders, conveyors (such as belt conveyors or pneumatic conveyors), and control systems. The selection of the appropriate conveyor type depends on factors like the volume of material, distance to be conveyed, and the need for dust control. For example, pneumatic conveyors are often used for fine coke powder due to their ability to handle high volumes and maintain low dust emissions. The system also includes safety features such as pressure relief valves and emergency stop mechanisms to protect operators and equipment.
Process Flow and Operational Efficiency
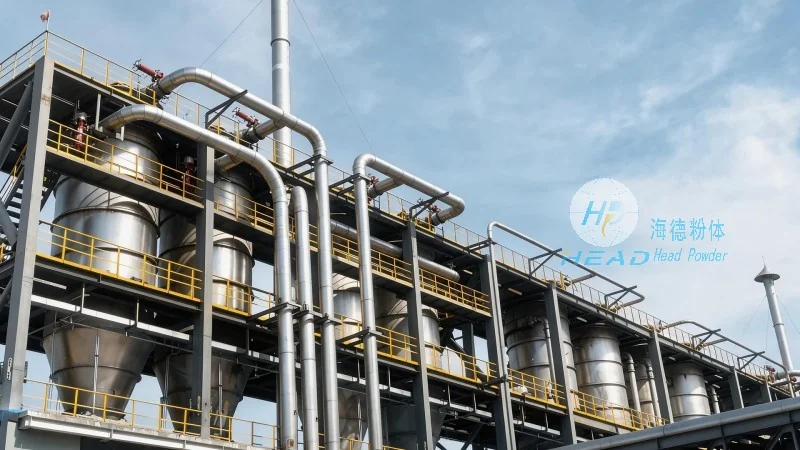
The process flow of the recycled coke powder conveying system begins with material feeding from storage silos or hoppers. The feeder ensures a consistent flow rate, which is critical for maintaining the conveyor's performance. The material then moves through the conveyor system, possibly undergoing temperature or moisture control steps if required. The system is equipped with sensors and monitoring devices to track flow rates, pressure, and other parameters in real-time. This data is used to optimize the process, reduce downtime, and improve overall operational efficiency. The company's advanced control systems allow for automated adjustments, ensuring the system operates at peak performance under varying conditions.
Maintenance and Safety Considerations
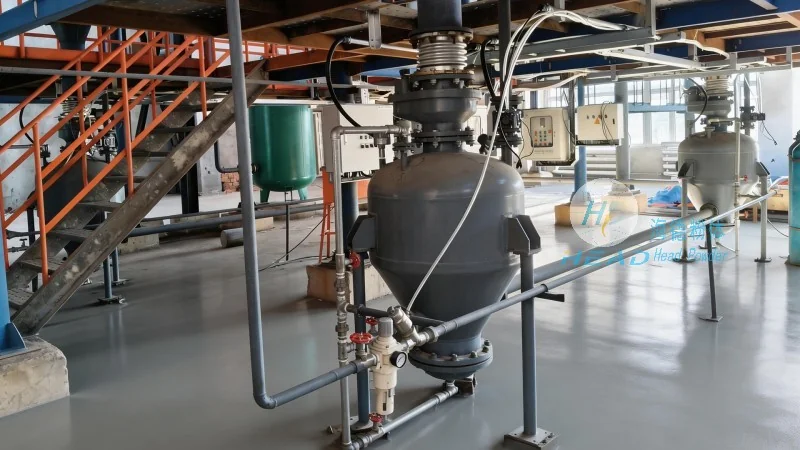
Maintenance of the recycled coke powder conveying system is essential to ensure long-term reliability and safety. Regular inspections of components like bearings, belts, and seals are performed to identify and address potential issues before they cause system failure. The system is designed with easy access points for maintenance personnel, reducing downtime during servicing. Safety considerations are integrated throughout the design, including explosion-proof features for pneumatic systems and proper grounding to prevent electrical hazards. The company provides comprehensive maintenance services and training to clients, ensuring that operators are equipped to handle the system safely and efficiently.
Customization and Application Examples
Shandong HeadPowder Engineering Co., Ltd. offers customized conveying solutions tailored to the specific needs of different industries. For instance, in the steel industry, the system may be designed to handle large volumes of coke powder from blast furnaces, with high-capacity belt conveyors and robust feeding mechanisms. In power plants, the system might focus on efficient dust collection and material transfer for fuel preparation. The company works closely with clients to understand their operational requirements and environmental constraints, providing solutions that meet both performance and regulatory standards. By leveraging their expertise in material handling and engineering, the company delivers systems that enhance productivity and reduce operational costs for their clients.