

Design of a Pneumatic Conveying System for Wet Ammonium Nitrate
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field of bulk material handling solutions, specializes in the design and implementation of advanced pneumatic conveying systems. This article focuses on the design of a specialized system for the efficient and safe transportation of wet ammonium nitrate, a critical component in various industrial applications such as fertilizer production and chemical processing. The system is engineered to address the unique challenges associated with handling wet ammonium nitrate, including moisture management, product stability, and system reliability.
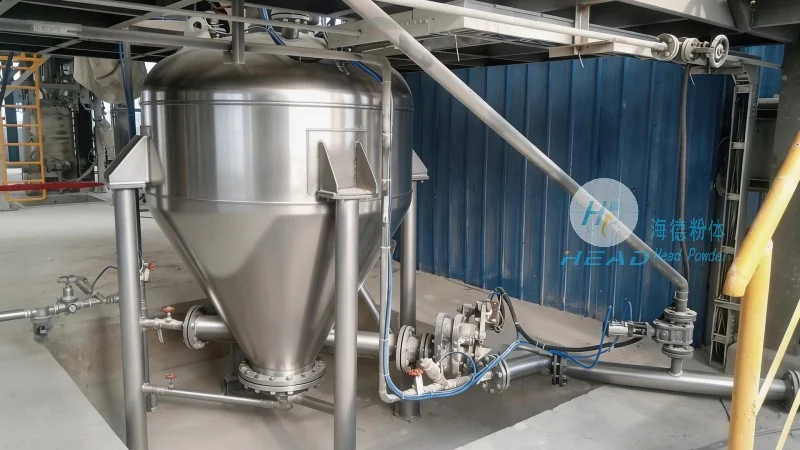
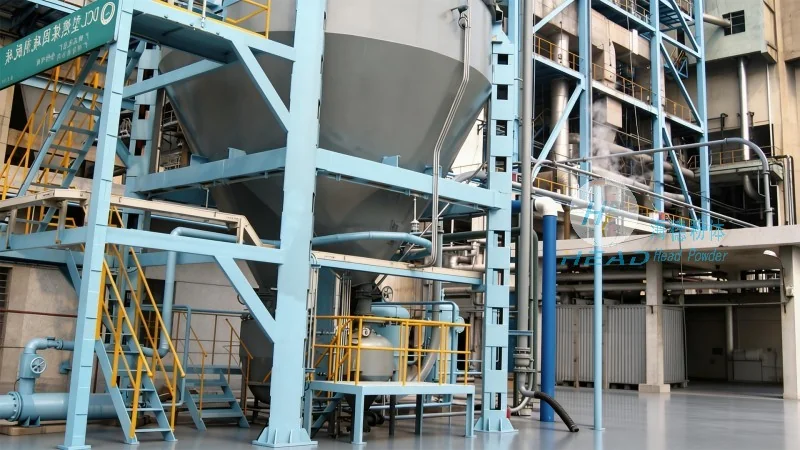
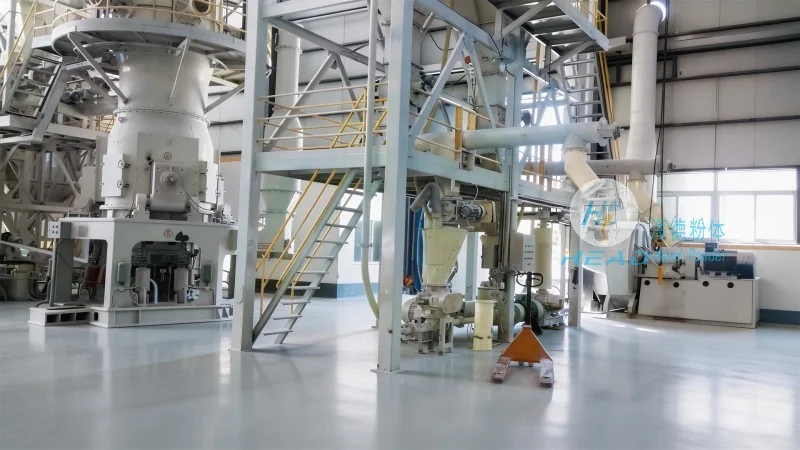
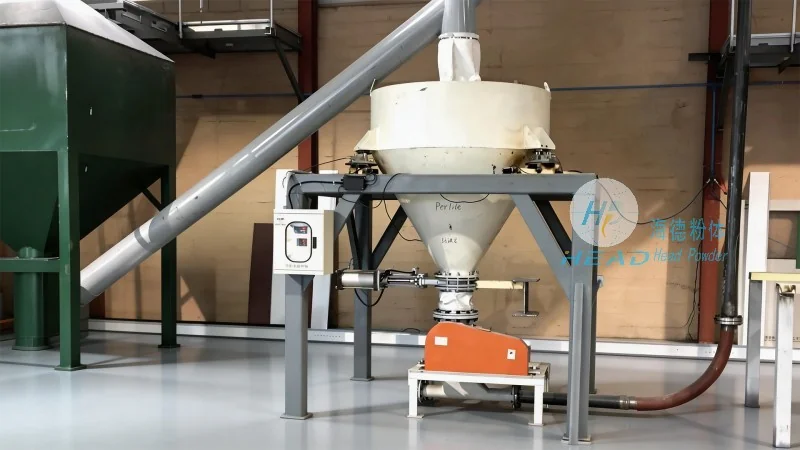
Key Features and Technical Specifications of the Wet Ammonium Nitrate Pneumatic Conveying System
The system designed by HeadPowder incorporates several key features that enhance its performance and adaptability. A robust airlock system is integrated to manage moisture content and prevent product leakage, ensuring that the material is conveyed in a controlled manner. High-capacity blower units are employed to maintain consistent air pressure, which is essential for maintaining the flow of wet ammonium nitrate through the pipeline network. The system also features a flexible pipeline design that can be customized to suit different plant layouts, allowing for easy integration into existing production lines. Advanced control mechanisms, including real-time monitoring of flow rates, pressure, and temperature, are implemented to ensure optimal operation and prevent system failures. These features collectively contribute to the system's high efficiency and reliability in handling wet ammonium nitrate.
Operational Advantages and Application Scenarios
For industries dealing with wet ammonium nitrate, the pneumatic conveying system offers several operational advantages over traditional material handling methods. Unlike belt conveyors or bucket elevators, the system eliminates direct contact between the product and mechanical components, reducing the risk of contamination and product degradation. This is particularly important for wet ammonium nitrate, which is sensitive to moisture and temperature changes. The system also minimizes material handling time and labor costs, as it can transport large volumes of material over long distances with minimal maintenance. This makes it ideal for applications in fertilizer manufacturing plants, where consistent and reliable material flow is essential for production continuity. Additionally, the system's ability to handle wet materials without the need for drying or pre-processing makes it a cost-effective solution for industries looking to streamline their operations.