

[Rice Husk Ash Pneumatic Conveying Solutions]
HeadPowder, a prominent engineering firm headquartered in Shandong, China, specializes in delivering advanced pneumatic conveying solutions for the efficient handling of rice husk ash. This article delves into the innovative technologies and practical applications offered by HeadPowder Engineering Co., Ltd. to address the unique challenges associated with transporting this material, ensuring optimal performance and minimal operational disruptions.
Challenges in Handling Rice Husk Ash and the Role of Pneumatic Conveying
Rice husk ash, a byproduct of rice processing, exhibits distinct physical and chemical properties that make conventional handling methods less effective. Its lightweight, powdery composition, often accompanied by moisture and abrasive particles, can lead to issues such as clogging, material degradation, and reduced system efficiency if not managed properly. Traditional solutions like belt conveyors or manual transport may struggle to maintain the quality of the ash, which is critical for its downstream applications, including use in cement production, as a filler in construction materials, or in other industrial processes. Pneumatic conveying systems, by utilizing air pressure to move material through sealed pipelines, offer a superior alternative by minimizing direct contact with mechanical components and preserving the integrity of the product throughout the transport process.
HeadPowder's Specialized Pneumatic Conveying Solutions
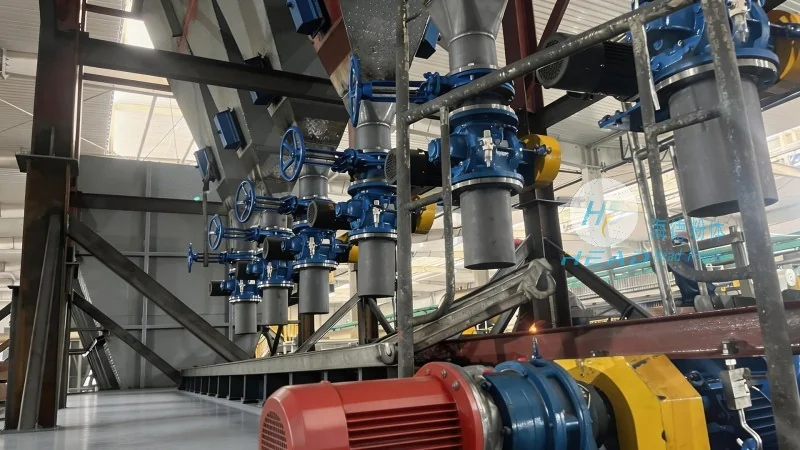
HeadPowder Engineering Co., Ltd. has developed a comprehensive portfolio of pneumatic conveying systems specifically engineered for rice husk ash applications. These solutions are designed to accommodate a wide range of flow rates, from low to high throughput, and are adaptable to diverse plant layouts and operational environments. The company's approach emphasizes the integration of cutting-edge technology with practical engineering solutions to deliver systems that are both efficient and cost-effective. Key components of their pneumatic conveying solutions include:
Technical Specifications and Advantages
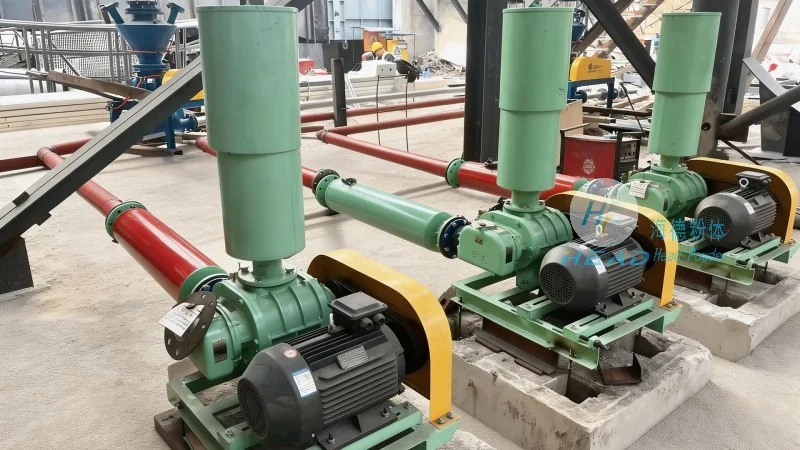
1. **System Configuration**: HeadPowder offers both positive and negative pressure pneumatic conveying systems. Positive pressure systems are ideal for long-distance transport and high-volume applications, where material is pushed through pipelines using air pressure. Negative pressure systems, on the other hand, are suitable for shorter distances and applications requiring material to be drawn from a source, such as from storage silos or hoppers. The choice of system depends on factors like material characteristics, plant layout, and operational requirements.
2. **Material Handling Efficiency**: The systems utilize high-efficiency blowers and airlocks to ensure consistent and reliable material transport. The design minimizes pressure drop along the pipeline, allowing for smooth material flow and reducing the need for frequent maintenance or system adjustments. This results in higher overall system efficiency and lower energy consumption compared to traditional methods.
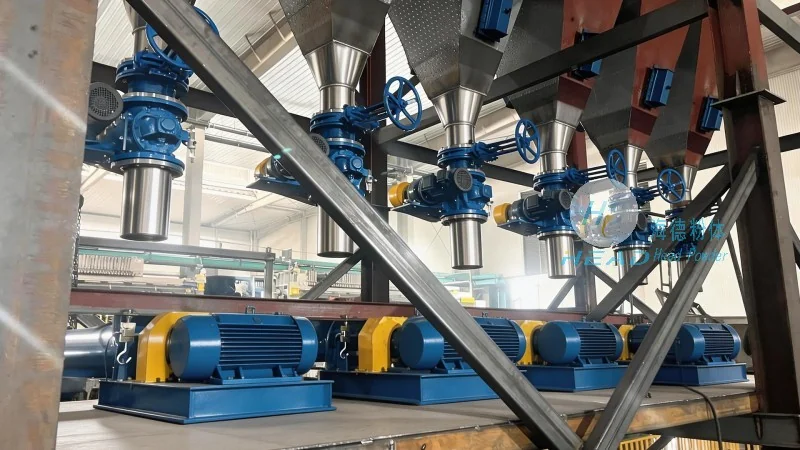
3. **Product Preservation**: Specialized equipment, such as rotary airlock valves and flexible hoses, is employed to prevent material degradation, caking, or contamination during transport. These components are designed to handle the abrasive and moisture-sensitive nature of rice husk ash, ensuring that the material remains in its original state until it reaches its destination. This is particularly important for applications where the ash's purity and quality are critical, such as in cement manufacturing or as a natural additive in food products.
4. **Safety and Compliance**: All pneumatic conveying systems are designed in accordance with international safety standards and regulations. Features like explosion-proof components, dust collection systems, and emergency shut-off mechanisms are integrated to ensure safe operation, protecting both personnel and equipment from potential hazards. The systems are also engineered to minimize dust emissions, contributing to a cleaner and safer working environment.
Real-World Applications and Case Studies
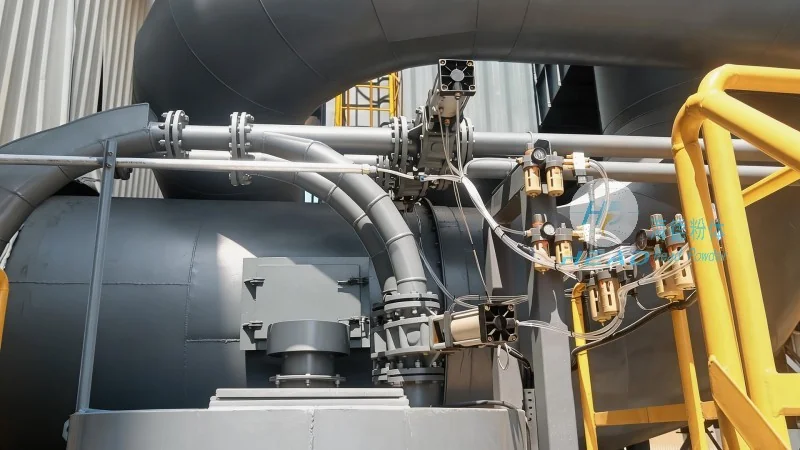
HeadPowder has successfully implemented pneumatic conveying solutions for rice husk ash in various industrial sectors. For example, in a large-scale cement plant, the company provided a positive pressure conveying system that transported rice husk ash from storage silos to the raw material blending area. The system was designed to handle high volumes of material with minimal pressure drop, ensuring a consistent feed to the kiln and improving overall production efficiency. In another case, a food processing facility utilized a negative pressure system to convey rice husk ash for use as a natural additive in organic products, where maintaining product purity and avoiding contamination was paramount. The system's ability to handle fine, powdery material without clogging or degradation was crucial to the success of this application.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd. continues to be a leader in providing reliable and efficient pneumatic conveying solutions for rice husk ash. By leveraging advanced engineering expertise and a customer-centric approach, the company ensures that its clients receive systems tailored to their specific needs, delivering long-term value and operational excellence. With its headquarters in Shandong, China, HeadPowder remains committed to innovation and quality, serving industries worldwide with cutting-edge material handling solutions. For inquiries or to discuss your rice husk ash conveying requirements, please contact HeadPowder Engineering Co., Ltd.