

Calcined Sand Pneumatic Conveying System Solution
HeadPowder, a leading engineering firm based in Shandong, China, specializes in providing comprehensive solutions for industrial material handling, with a particular focus on pneumatic conveying systems for calcined sand applications. This document outlines a detailed system solution designed to efficiently transport calcined sand from storage to processing units, ensuring optimal performance, reliability, and cost-effectiveness for industrial operations.
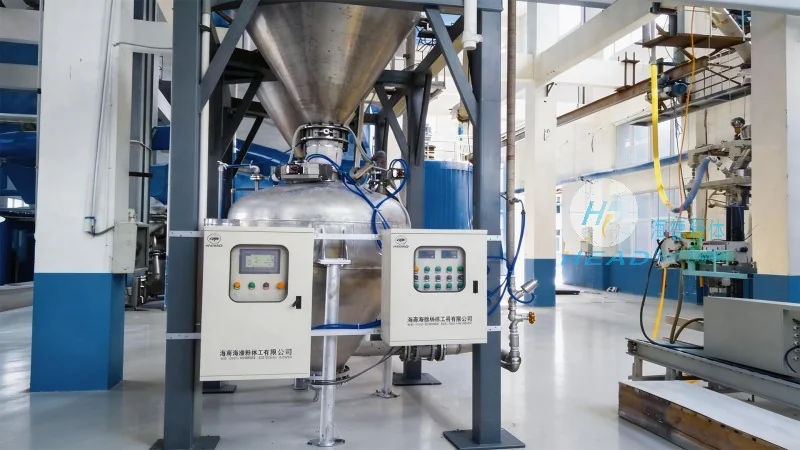
System Overview and Core Components
The calcined sand pneumatic conveying system is engineered to handle the unique properties of calcined sand, such as its density, flow characteristics, and potential dust generation. The solution incorporates several key components to ensure seamless material transport. These include a high-capacity storage silo or hopper for initial material collection, a rotary airlock feeder to control the discharge rate and prevent air leakage, and a positive displacement blower or high-pressure air compressor to generate the necessary airflow. The system also features a pipeline network with appropriate pipe diameters and fittings to minimize pressure drop and ensure consistent flow. Additionally, a dust collection and filtration system is integrated to comply with environmental regulations and maintain air quality within the facility.
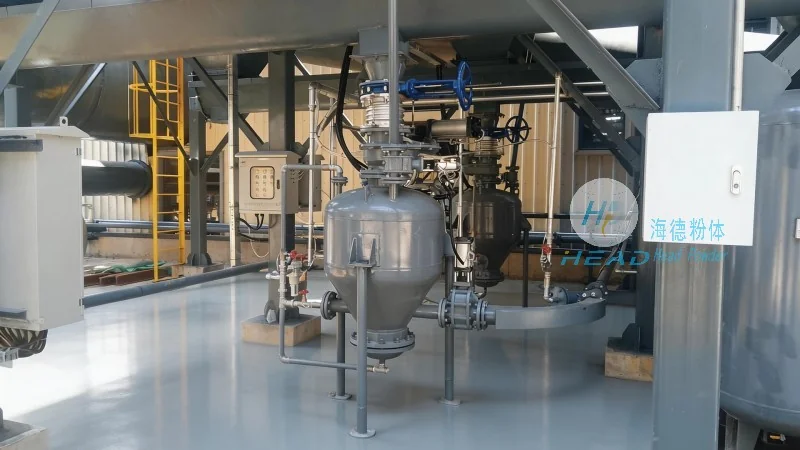
Advantages of the Pneumatic Conveying System
Implementing a pneumatic conveying system for calcined sand offers numerous advantages over traditional mechanical conveying methods. Firstly, it eliminates the need for moving parts in the conveying line, reducing maintenance requirements and downtime. The system is also highly flexible, allowing for changes in material flow rates and routing without major modifications. Another key benefit is the ability to handle calcined sand in a dust-free environment, which enhances worker safety and prevents product contamination. Furthermore, the system can be designed to operate at low or high pressure, depending on the distance and material characteristics, optimizing energy consumption and operational efficiency. The integration of a dust collection system ensures compliance with local air quality standards, making it an environmentally responsible choice for industrial applications.
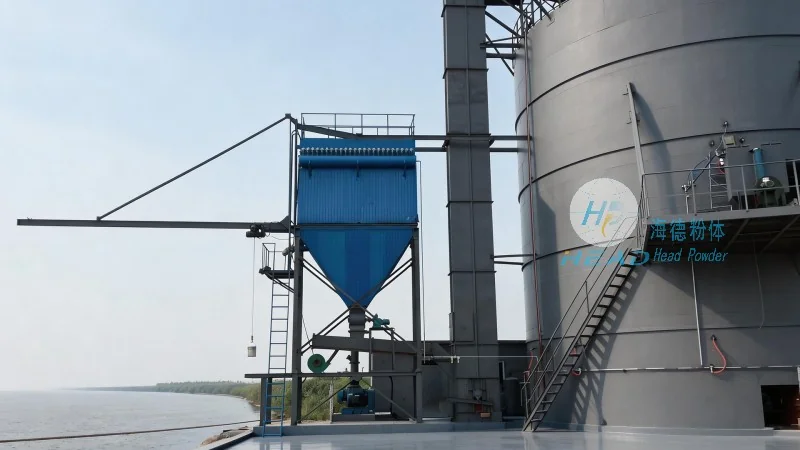
Customization and Scalability
HeadPowder understands that each industrial facility has unique operational requirements. Therefore, the calcined sand pneumatic conveying system is designed to be highly customizable and scalable. The system can be tailored to accommodate varying calcined sand volumes, from small-scale laboratory applications to large-scale industrial production lines. The components, such as the blower capacity, pipe diameter, and feeder size, can be adjusted to match the specific needs of the client. Additionally, the system can be integrated with existing infrastructure, minimizing the need for new construction or major renovations. This flexibility ensures that the system not only meets current operational demands but also supports future growth and expansion.
Installation and Maintenance Considerations
Proper installation and regular maintenance are crucial for the long-term performance and reliability of the calcined sand pneumatic conveying system. HeadPowder provides comprehensive installation services, including site assessment, system layout planning, and equipment installation. The installation process adheres to industry best practices to ensure optimal performance and safety. Regular maintenance is essential to prevent system failures and extend the lifespan of components. The maintenance plan includes routine inspections of the blower, feeder, and pipeline, as well as cleaning of the dust collection system. HeadPowder also offers maintenance contracts to ensure that the system remains in optimal condition, minimizing downtime and maximizing operational efficiency.
Conclusion and Contact Information
HeadPowder's calcined sand pneumatic conveying system solution is a reliable and efficient option for industrial material handling. By leveraging advanced engineering and customization, the system addresses the unique challenges of calcined sand transport while providing numerous benefits, including reduced maintenance, improved safety, and environmental compliance. For more information or to discuss how this system can meet your specific operational needs, please contact HeadPowder at its headquarters in Shandong, China.