

Pneumatic Conveying Solutions for Stone Powder and Limestone
Efficient material handling is crucial in industrial processes, especially when dealing with bulk materials like stone powder and limestone. Pneumatic conveying systems offer a reliable and effective method to transport these materials over long distances, ensuring minimal dust, reduced labor costs, and enhanced safety. This article explores the specialized solutions provided by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, focusing on the technical aspects, benefits, and applications of pneumatic conveying for stone powder and limestone.
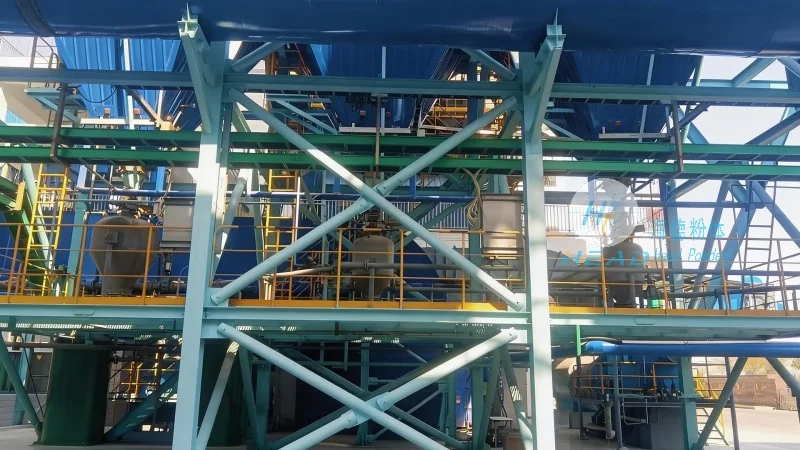
Understanding Pneumatic Conveying Systems
Pneumatic conveying involves the use of air to transport solid materials through a pipeline. Unlike traditional methods such as belt conveyors or bucket elevators, this system utilizes air pressure to move the material, making it ideal for handling fine powders and granular materials. The core components of a pneumatic conveying system include a hopper, a blower or compressor, a pipeline network, and a discharge point. The system operates by creating a vacuum or pressure differential to draw or push the material through the pipeline. For stone powder and limestone, which are often abrasive and can cause wear on equipment, specialized materials and designs are essential to ensure longevity and efficiency.
Key Features of Stone Powder and Limestone Pneumatic Conveying
When designing pneumatic conveying systems for stone powder and limestone, several key features must be considered to optimize performance and durability. First, the material's properties, such as particle size, density, and moisture content, significantly impact the system's design. Larger particles may require higher air velocities to prevent blockages, while finer powders need more precise control to avoid clogging. Second, the system must be constructed from materials resistant to abrasion and corrosion, as stone powder and limestone can be harsh on equipment. Stainless steel, high-chrome alloys, and specialized coatings are commonly used to extend the lifespan of components like the hopper, pipeline, and blower. Third, the system's layout and configuration are critical for efficient material flow. Properly sized pipelines, appropriate bends, and effective dust collection systems are essential to maintain consistent performance and minimize maintenance.
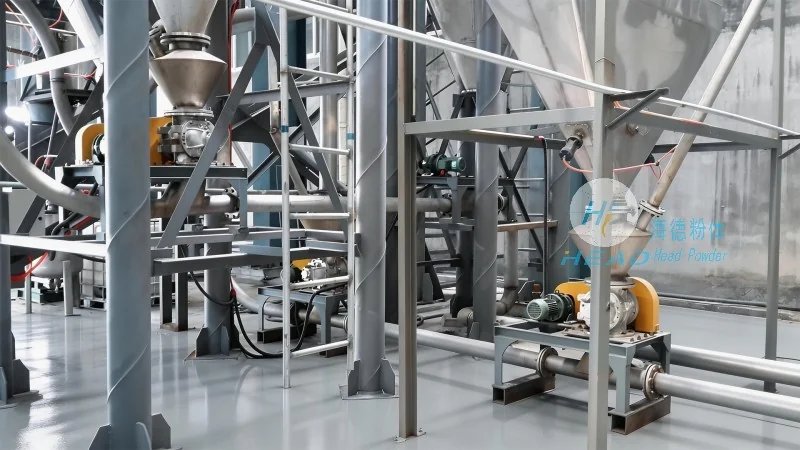
Benefits of Implementing Pneumatic Conveying Solutions
Adopting pneumatic conveying solutions for stone powder and limestone processing offers numerous advantages. One of the primary benefits is the reduction in dust exposure, which enhances workplace safety and compliance with environmental regulations. Unlike open-air handling methods, pneumatic systems contain the material within a closed pipeline, preventing dust from spreading into the environment. This not only improves air quality but also reduces the risk of respiratory issues for workers. Additionally, pneumatic conveying reduces labor costs by automating the material transport process. Manual handling of bulk materials is time-consuming and labor-intensive, while a well-designed pneumatic system can handle large volumes with minimal human intervention. The system also improves operational efficiency by enabling continuous material flow, which is particularly beneficial in high-demand production environments. Furthermore, the compact design of pneumatic conveying systems allows for easier integration into existing facilities, minimizing the need for extensive construction or modifications.
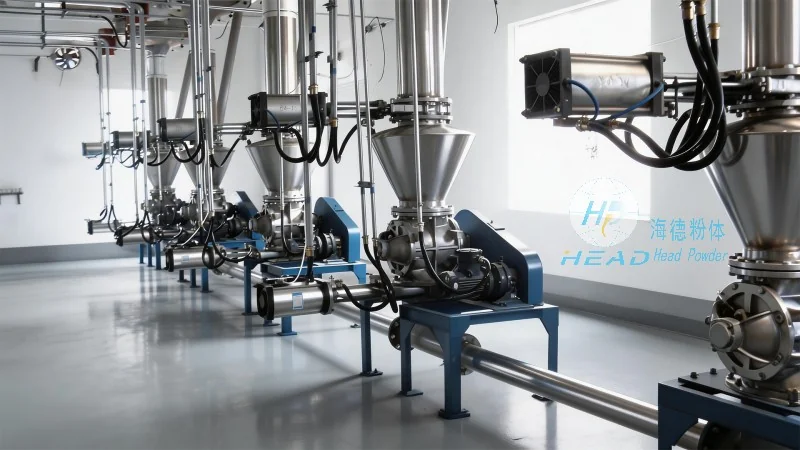
Shandong HeadPowder Engineering Co., Ltd.: Your Trusted Partner in Pneumatic Conveying
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of advanced pneumatic conveying solutions tailored for stone powder and limestone applications. HeadPowder is headquartered in Shandong, China, and has established itself as a trusted partner in the industry with years of experience in designing, manufacturing, and installing customized systems. The company's team of engineers and technicians work closely with clients to assess their material handling requirements, provide technical consultations, and deliver tailored solutions that enhance productivity and reduce operational costs.
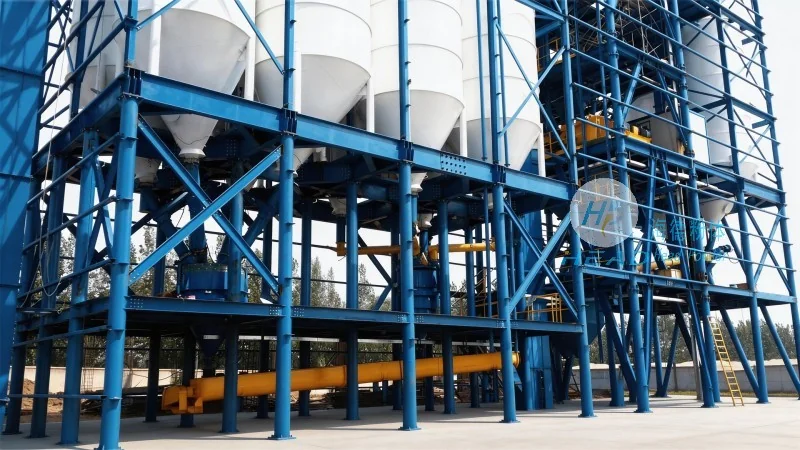
Customized Solutions for Diverse Applications
HeadPowder recognizes that each industrial application has distinct requirements, and therefore, offers a range of customized pneumatic conveying solutions. Whether the application involves transporting stone powder from a storage silo to a processing plant or limestone from a quarry to a cement production facility, the company can design a system that optimizes material flow and efficiency. The solutions are adaptable to various scales, from small-scale operations to large industrial plants, ensuring that clients receive a system that fits their specific needs and budget. The company also provides comprehensive after-sales support, including maintenance services, spare parts supply, and technical assistance, to ensure the long-term reliability and performance of the installed systems.
Conclusion: Enhancing Efficiency with Pneumatic Conveying
In conclusion, pneumatic conveying solutions for stone powder and limestone are a vital component in modern industrial operations. By leveraging the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., industries can achieve efficient, safe, and cost-effective material handling. The benefits of reduced dust, automated processes, and improved operational efficiency make pneumatic conveying an attractive option for businesses looking to enhance their productivity and compliance with environmental standards. With a focus on quality, innovation, and customer satisfaction, HeadPowder continues to be a trusted partner in providing reliable pneumatic conveying solutions for stone powder and limestone applications.