

Introduction to Soda Ash Pneumatic Conveying Equipment: Structure and Working Principles
For industries dealing with soda ash, efficient material handling is crucial for maintaining production efficiency and operational safety. Pneumatic conveying systems have emerged as a reliable solution, and this article provides an overview of soda ash pneumatic conveying equipment, focusing on its structural design and operational principles. By understanding the mechanics behind these systems, businesses can make informed decisions about integrating such technology into their processes.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of material handling solutions, specializes in the design, development, and supply of pneumatic conveying equipment. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for industries requiring robust and efficient material transport systems. HeadPowder’s expertise lies in tailoring equipment to meet specific operational needs, ensuring optimal performance and longevity. The company’s headquarters is located in Shandong, China, where it leverages advanced engineering capabilities to deliver cutting-edge solutions.
Structural Components of Soda Ash Pneumatic Conveying Systems
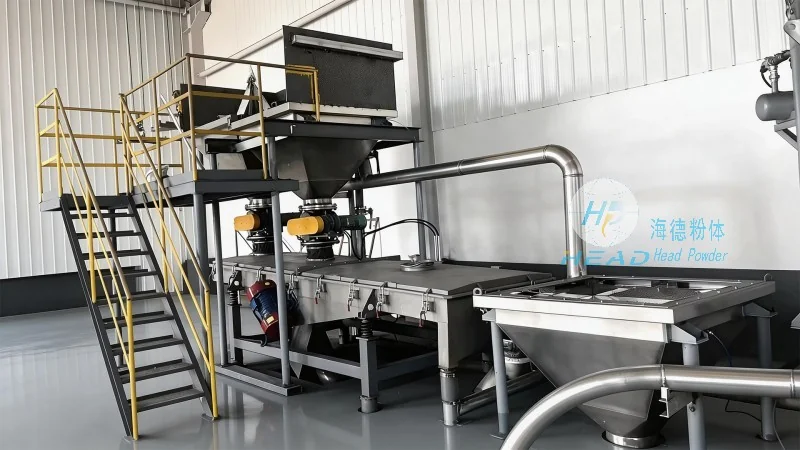
A typical soda ash pneumatic conveying system comprises several key components that work in harmony to transport material. The primary elements include the material feed hopper, which holds the soda ash and regulates the flow into the system. The hopper is equipped with a feeder mechanism, such as a rotary valve or a screw feeder, to control the discharge rate and prevent blockages. The conveying line, often made of stainless steel or other corrosion-resistant materials, is designed to withstand the chemical properties of soda ash and ensure durability. The system also includes a blower or air compressor that generates the necessary air pressure to move the material through the pipeline. Additionally, a filter and separator unit is integrated to remove dust and debris from the air stream, maintaining air quality and preventing system contamination. The control panel, equipped with sensors and monitoring devices, allows operators to adjust parameters like air pressure and flow rate, ensuring precise control over the conveying process.
Working Principles of Pneumatic Conveying for Soda Ash
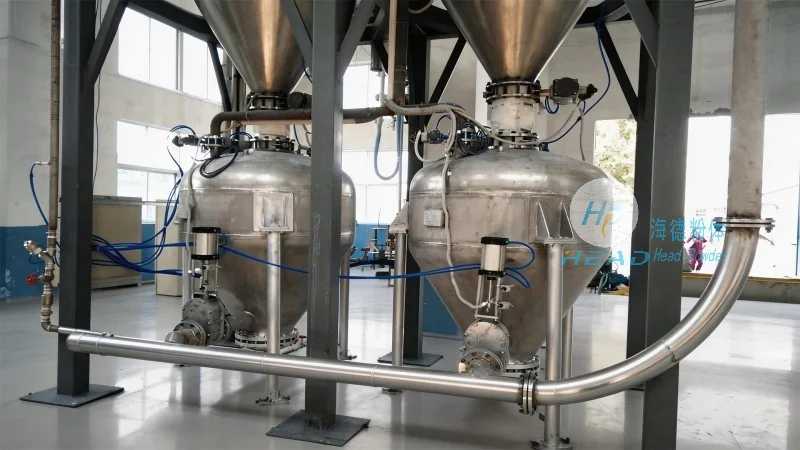
The operation of a soda ash pneumatic conveying system relies on the principle of air movement to transport bulk material. The process begins with the material being fed from the hopper into the conveying line. As the blower generates high-pressure air, it creates a vacuum or positive pressure within the system, depending on the configuration. This air stream propels the soda ash particles through the pipeline, carrying them to the discharge point. The velocity of the air and the size of the particles determine the efficiency of the conveying process. Proper design of the system ensures that the air velocity is sufficient to prevent material settling or blockages, while minimizing energy consumption. The filter and separator unit plays a critical role by capturing any fine particles that may escape the conveying line, preventing them from entering the environment or damaging downstream equipment. This not only maintains air quality but also extends the lifespan of the system components.
Advantages of Using Pneumatic Conveying for Soda Ash Handling
Implementing pneumatic conveying systems for soda ash offers numerous advantages over traditional methods like belt conveyors or bucket elevators. One of the key benefits is the ability to handle material in a closed system, which reduces dust exposure and improves workplace safety. This is particularly important for soda ash, which can be a respiratory irritant if inhaled. The closed system also prevents contamination from external sources, ensuring the purity of the material. Another advantage is the flexibility of the system, as it can be easily reconfigured or expanded to accommodate changes in production volume or layout. Pneumatic conveying systems are also more energy-efficient compared to mechanical systems, as they require less maintenance and have lower operational costs. Additionally, the system can handle materials with varying particle sizes and moisture content, making it suitable for diverse industrial applications. The ability to transport material over long distances without the need for multiple transfer points further enhances operational efficiency.
Applications and Industries Benefiting from Soda Ash Pneumatic Conveying
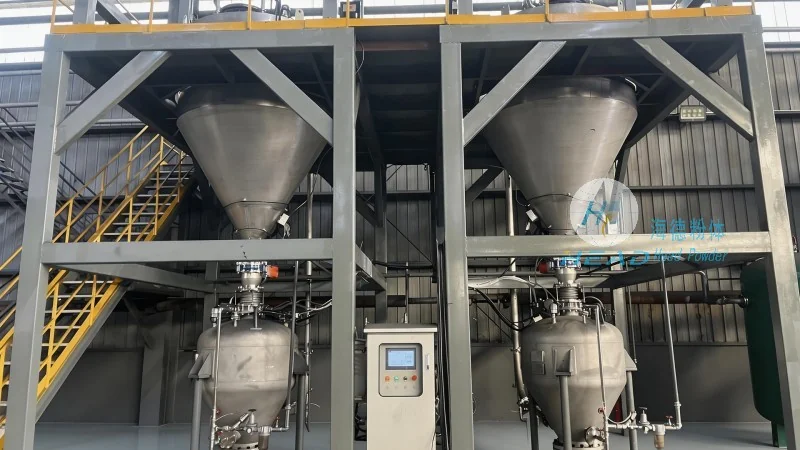
Soda ash pneumatic conveying equipment is widely used across various industries that rely on soda ash as a raw material. The chemical industry, for instance, utilizes soda ash in the production of glass, detergents, and paper. The food and beverage industry also benefits from this technology, as soda ash is used as a food additive and in the processing of beverages. In the pharmaceutical sector, the closed system ensures the purity of the material, which is critical for manufacturing quality drugs. The construction industry uses soda ash in the production of cement and other building materials. By providing a reliable and efficient means of material transport, pneumatic conveying systems support the smooth operation of these industries, ensuring consistent supply of soda ash to production lines.
Conclusion: Enhancing Efficiency with HeadPowder's Pneumatic Conveying Solutions
As industries continue to seek more efficient and sustainable material handling solutions, pneumatic conveying systems for soda ash have become an indispensable part of modern operations. HeadPowder, with its expertise in designing and manufacturing high-quality equipment, offers tailored solutions that meet the specific needs of clients. By leveraging advanced structural designs and operational principles, these systems enhance productivity, reduce operational costs, and improve workplace safety. The integration of such technology not only optimizes material transport but also contributes to the overall sustainability of industrial processes. For businesses looking to upgrade their material handling capabilities, HeadPowder’s pneumatic conveying equipment provides a reliable and effective solution, backed by years of industry experience and commitment to excellence.