

Principle and Working Scene Characteristics of Bulk Bag Breakage Powder Pneumatic Conveying
Bulk bag breakage powder pneumatic conveying is a critical technology in material handling, particularly for industries dealing with bulk powders and granules. This system efficiently transfers materials from bulk bags into processing equipment, storage silos, or other destinations without the need for manual handling. The process involves breaking open the bulk bag, feeding the material into a hopper or feeder, and then using compressed air or other gas to transport the powder through a pipeline network. Understanding the principles behind this technology and its application in various working scenes is essential for optimizing material flow and improving operational efficiency.
Principle of Bulk Bag Breakage and Pneumatic Conveying
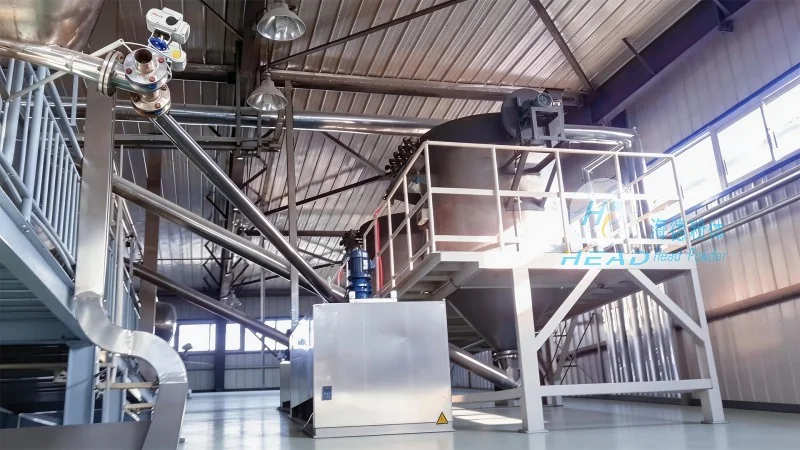
The core principle of bulk bag breakage powder pneumatic conveying is the combination of mechanical and pneumatic forces to handle bulk materials. The process typically begins with the bulk bag being placed on a discharge valve or a hopper with a bag breaker attachment. The bag is then opened, and the material is released into the hopper. A feeder, such as a rotary valve or a screw feeder, then meters the material into the conveying line. Compressed air, often supplied by a blower or a positive displacement pump, is introduced at the inlet of the conveying line, creating a pressure differential that propels the powder through the pipeline. The conveying system may include components like filters, cyclones, or dust collectors to ensure the material is transported efficiently and without contamination. The entire process is designed to minimize material degradation, reduce dust emissions, and maintain product quality throughout the transfer.
Working Scene Characteristics and Applications
Bulk bag breakage powder pneumatic conveying is widely used in various industrial applications where bulk powders need to be transferred from storage to processing units. In the chemical industry, for example, this system is used to handle chemicals, pigments, and other fine powders that require precise control over dust and contamination. The food and beverage industry also utilizes this technology for transferring ingredients like flour, sugar, and spices, ensuring hygienic and efficient handling. In the pharmaceutical sector, the system is adapted to handle active pharmaceutical ingredients (APIs) and other sensitive materials, with strict controls on particle size, moisture content, and contamination. Additionally, in the mining and minerals industry, bulk bag breakage pneumatic conveying is used to transport ores, minerals, and other bulk materials from storage to processing plants. The working scene characteristics include high throughput, low maintenance requirements, and the ability to handle a wide range of material properties, from fine powders to coarse granules. The system is also suitable for applications where space is limited, as it can be installed in compact configurations and integrated with existing processing equipment.
Key Components and Their Functions
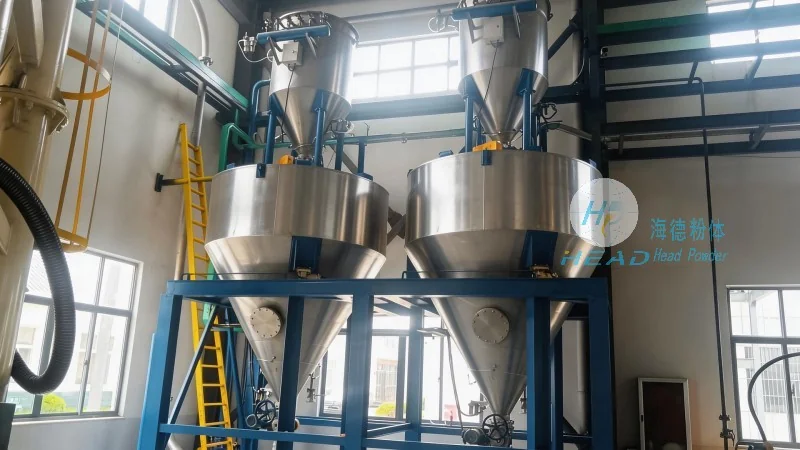
The effectiveness of bulk bag breakage powder pneumatic conveying depends on several key components working in harmony. The bag breaker is a critical component that safely and efficiently opens the bulk bag without damaging the material inside. It may include features like a cutting blade or a mechanical gripper that secures the bag before opening. The discharge valve or hopper is designed to collect the material from the bag and feed it into the conveying system. The feeder, such as a rotary valve or a screw feeder, regulates the flow rate of the material into the pipeline, ensuring consistent and controlled conveying. The blower or compressor provides the necessary air pressure to move the material through the pipeline. Filters and dust collectors are essential for maintaining air quality and preventing dust accumulation in the system. These components work together to ensure the material is conveyed efficiently, with minimal loss and contamination.
Advantages and Benefits of the System
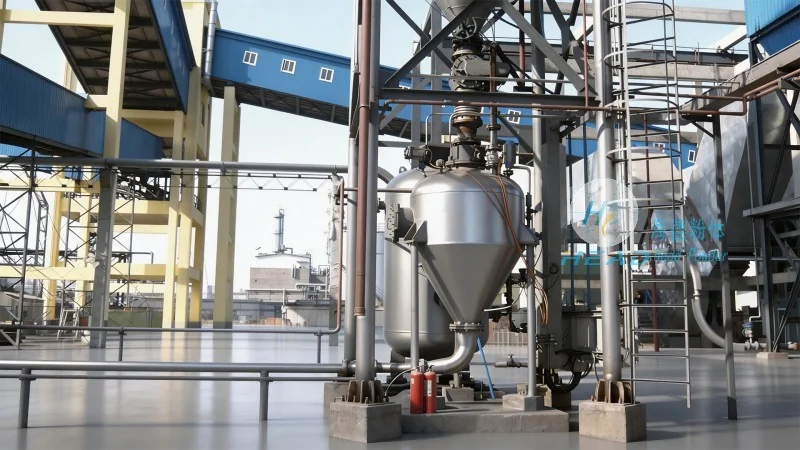
Bulk bag breakage powder pneumatic conveying offers several advantages over traditional material handling methods. One of the primary benefits is the reduction in manual labor, as the system automates the process of transferring bulk materials from bags to processing equipment. This not only improves safety by minimizing exposure to dust and hazardous materials but also increases operational efficiency by reducing downtime and labor costs. The system also minimizes material degradation, as the material is handled gently and without the need for excessive vibration or impact. This is particularly important for sensitive materials like pharmaceuticals or food ingredients, where particle size and quality are critical. Additionally, the system reduces dust emissions and improves air quality, contributing to a safer and more environmentally friendly workplace. The compact design of the system allows for easy integration into existing facilities, making it a cost-effective solution for upgrading material handling processes. The system also offers flexibility in terms of material handling, as it can be adapted to handle a wide range of bulk powders and granules with varying properties.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of bulk bag breakage powder pneumatic conveying systems and related material handling solutions. With a focus on innovation and quality, the company specializes in designing and manufacturing customized conveying systems tailored to the specific needs of various industries. HeadPowder's expertise lies in understanding the unique challenges of material handling and developing solutions that optimize efficiency, safety, and product quality. The company's products are designed to meet the highest standards of performance and reliability, ensuring long-term operation and minimal maintenance. HeadPowder serves a wide range of industries, including chemicals, food and beverage, pharmaceuticals, mining, and minerals, providing comprehensive material handling solutions that enhance operational productivity. The company's commitment to customer satisfaction and technical excellence has established it as a trusted partner in the material handling industry.