

Principles and Application Scenarios of Air-Driven Powder Transport for Aggregates
HeadPowder, a leading engineering company based in Shandong, China, specializes in advanced powder transport solutions tailored for the aggregate industry. The company's expertise lies in air-driven systems that efficiently handle sand, gravel, and other fine particulate materials, ensuring reliable and cost-effective material transfer in various industrial applications.

Principles of Air-Driven Powder Transport
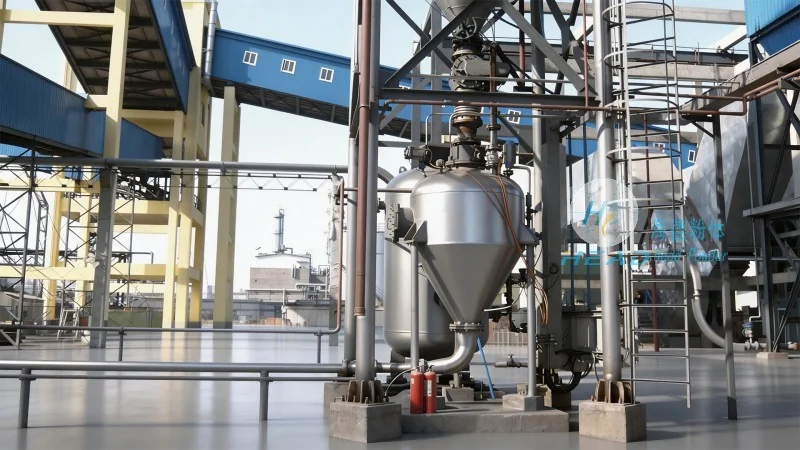
The core principle of air-driven powder transport, also known as pneumatic conveying, involves the use of compressed air to move bulk materials through a pipeline. This method relies on the creation of a pressure differential between the material source and the destination. By introducing air into the conveying line, the material is suspended and carried along the pipeline. The system typically consists of a hopper for material storage, a blower or compressor to generate the necessary air pressure, and a pipeline network that connects the source to the processing or storage point. The choice of conveying method—such as dilute phase or dense phase—depends on the material characteristics, distance, and required flow rate. Dilute phase systems use lower air-to-material ratios, suitable for fine powders over short to medium distances, while dense phase systems employ higher air-to-material ratios, ideal for handling abrasive or sensitive materials over longer distances.
Key Features and Advantages of Air-Driven Systems
HeadPowder's air-driven powder transport systems offer several advantages that make them a preferred choice in the aggregate industry. Firstly, these systems provide a dust-free and enclosed environment, reducing the risk of material contamination and improving workplace safety. Unlike traditional belt or bucket elevators, pneumatic conveying eliminates the need for open handling, which is particularly beneficial for handling fine powders that can cause respiratory issues or environmental pollution. Secondly, the systems are highly flexible and can be easily integrated into existing production lines or expanded to accommodate future growth. The modular design allows for customization based on specific operational requirements, such as varying material flow rates or changing processing needs. Thirdly, air-driven systems offer energy efficiency compared to other bulk material handling methods. By optimizing the air pressure and flow rate, the systems minimize energy consumption while maintaining consistent material transport performance. This efficiency translates into lower operational costs and reduced environmental impact, aligning with modern industrial sustainability goals.
Application Scenarios in the Aggregate Industry
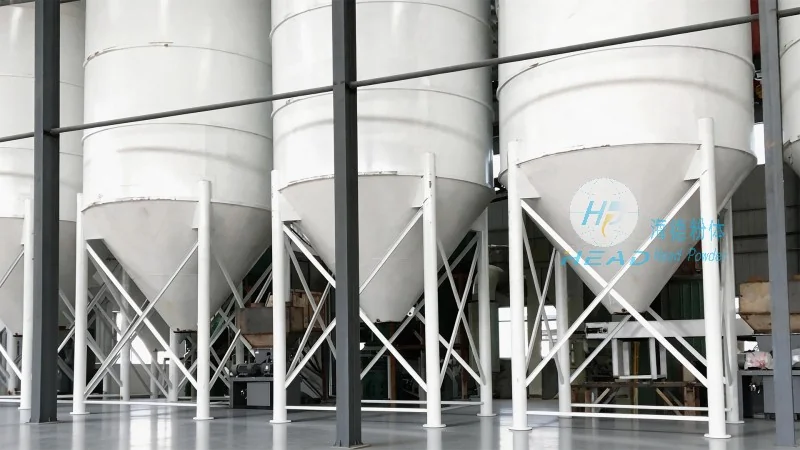
HeadPowder's air-driven powder transport solutions are widely applied in various scenarios within the aggregate industry. One common application is in concrete batching plants, where sand and gravel are transported from storage silos to the mixing area. The enclosed pneumatic system ensures that the materials remain dry and free from contamination, which is critical for maintaining the quality of concrete. Another key application is in mining operations, where crushed rock and ore are conveyed from processing facilities to storage or transport vehicles. The robust design of the air-driven systems can handle the abrasive nature of these materials, extending the lifespan of the equipment and reducing maintenance costs. Additionally, in construction sites, these systems are used to transport sand and gravel to different work areas, improving operational efficiency and reducing the need for manual handling. The flexibility of the system allows for easy reconfiguration based on the changing needs of the construction project, ensuring smooth material flow throughout the entire process.
Customization and Integration Capabilities
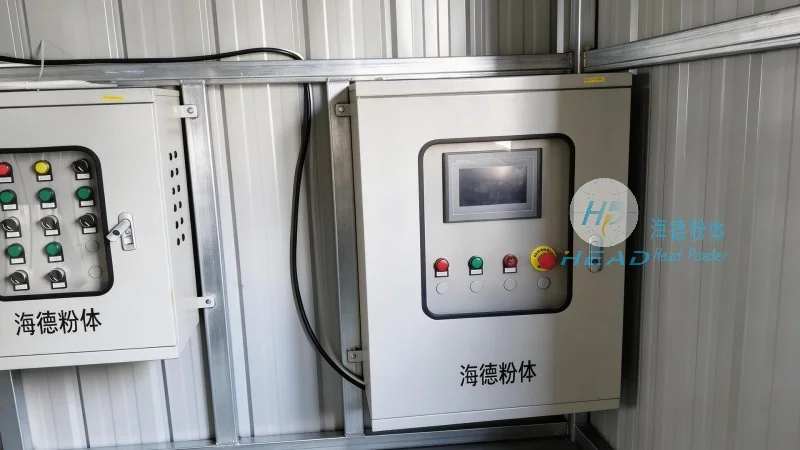
HeadPowder understands that each aggregate operation has unique requirements, and the company offers tailored solutions to meet these needs. The air-driven powder transport systems can be customized in terms of pipeline layout, material handling capacity, and control systems. For example, the system can be designed with multiple inlets and outlets to handle materials from different sources or to distribute materials to various destinations. The control systems can be integrated with existing plant management software, enabling real-time monitoring and adjustment of the conveying process. This integration enhances operational efficiency and allows for proactive maintenance, reducing downtime and increasing overall productivity. Furthermore, HeadPowder provides comprehensive after-sales support, including installation, commissioning, and ongoing maintenance services. The company's technical team works closely with clients to ensure that the system is optimized for their specific operational conditions, ensuring long-term reliability and performance.