

Principle and Working Scene Characteristics of Cement Granular Material Conveying System Equipment
Understanding the core principles and operational characteristics of cement granular material conveying systems is essential for optimizing material handling processes in industrial applications. These systems are designed to efficiently transport bulk cement and similar granular materials with precision and reliability, playing a critical role in various manufacturing and construction environments.
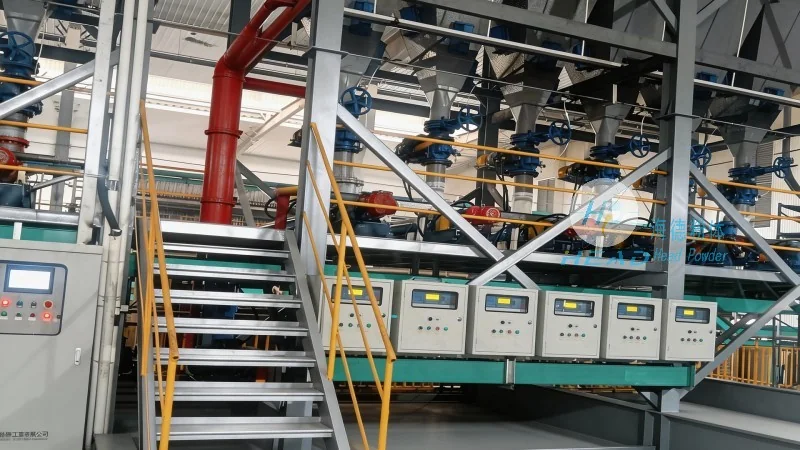
Core Principles of Cement Granular Material Conveying Systems
The fundamental principle behind cement granular material conveying systems lies in the use of specialized machinery to move bulk materials from one location to another. These systems typically incorporate components such as feeders, conveyors, and control mechanisms that work in tandem to ensure smooth and continuous material flow. The design of these systems is tailored to handle the specific physical properties of cement, including its density, flowability, and potential for dust generation, which are crucial factors in optimizing performance and safety.
Key operational principles include the use of mechanical or pneumatic conveying methods. Mechanical systems often rely on screw conveyors, belt conveyors, or bucket elevators, which utilize physical force to move materials. Pneumatic systems, on the other hand, employ air pressure to transport materials through pipelines, offering advantages in terms of flexibility and reduced maintenance compared to mechanical alternatives. The choice between these methods depends on factors such as the distance of material transport, the required throughput, and the environmental constraints of the application.
Working Scene Characteristics of Cement Granular Material Conveying Systems
Cement granular material conveying systems are widely used in diverse industrial settings, each presenting unique characteristics that influence system design and operation. In cement production facilities, these systems are integral to the transportation of raw materials and finished products, ensuring seamless integration between different stages of the production process. The high throughput requirements in such environments demand robust and high-capacity conveying solutions that can handle large volumes of material efficiently.
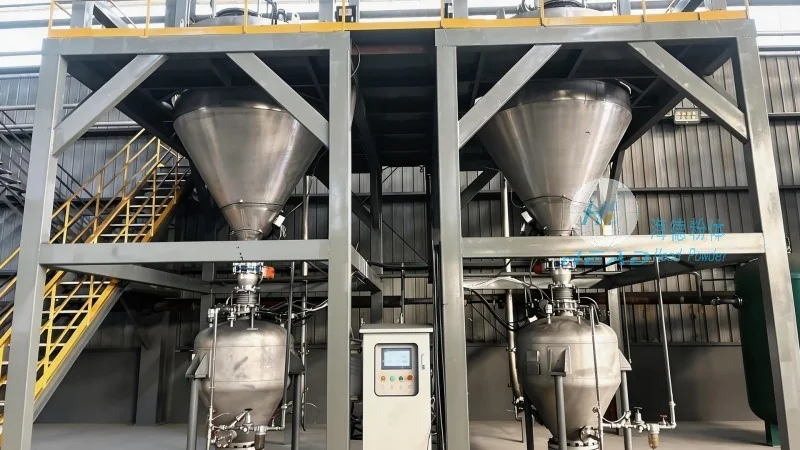
In construction sites and building material distribution centers, the systems are utilized to transport cement to various work areas, supporting the needs of on-site projects. The working scene characteristics in these environments often involve variable material loads, frequent start-stop operations, and the need for compact and space-efficient designs to accommodate limited site space. Additionally, the systems must be capable of handling different types of cement, such as Portland cement or blended cements, without compromising performance or causing material degradation.
In industrial plants involved in the production of concrete products, such as precast concrete elements or ready-mix concrete, the conveying systems play a vital role in supplying raw cement to mixing operations. The working scene in these facilities is characterized by continuous production cycles and the need for precise material dosing to maintain consistent product quality. The systems must also be equipped with features like dust suppression and material separation to ensure environmental compliance and operational safety.
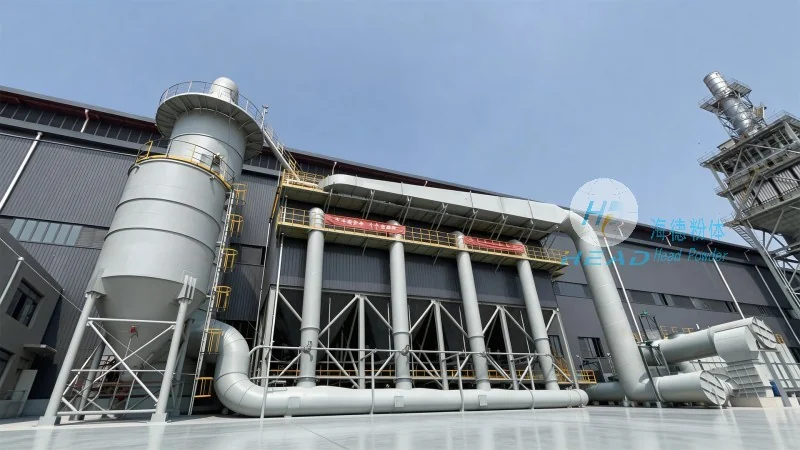
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading provider of industrial material handling solutions, specializes in the design, manufacturing, and installation of cement granular material conveying systems. With a strong presence in China, particularly in Shandong province, the company has established itself as a trusted partner for businesses seeking reliable and efficient material transport solutions. HeadPowder's expertise lies in understanding the unique challenges of cement handling and developing customized systems that meet the specific needs of each client.
The company's commitment to quality and innovation is reflected in its state-of-the-art manufacturing facilities and rigorous quality control processes. By leveraging advanced engineering techniques and materials, HeadPowder ensures that its conveying systems are durable, low-maintenance, and capable of withstanding the demanding conditions of cement processing environments. The company's team of experienced engineers and technicians provides comprehensive support, from system design and installation to ongoing maintenance and troubleshooting.
HeadPowder's operations are based in Shandong, China, a region known for its robust industrial infrastructure and access to key raw material sources. This location allows the company to efficiently serve a wide range of clients across the country and beyond, while maintaining close proximity to manufacturing and logistics networks. The company's dedication to customer satisfaction and technical excellence has earned it a reputation as a leading supplier of cement granular material conveying systems in the industry.