

Principle and Working Scene Characteristics of Rice Husk Ash Material Conveying System Equipment
The rice husk ash material conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., is a specialized device designed for the efficient transportation of rice husk ash. This system is engineered to handle the unique physical properties of rice husk ash, ensuring reliable and continuous material flow in industrial applications. The equipment integrates advanced mechanical and control technologies to meet the demands of various processing environments.
Principle of Operation
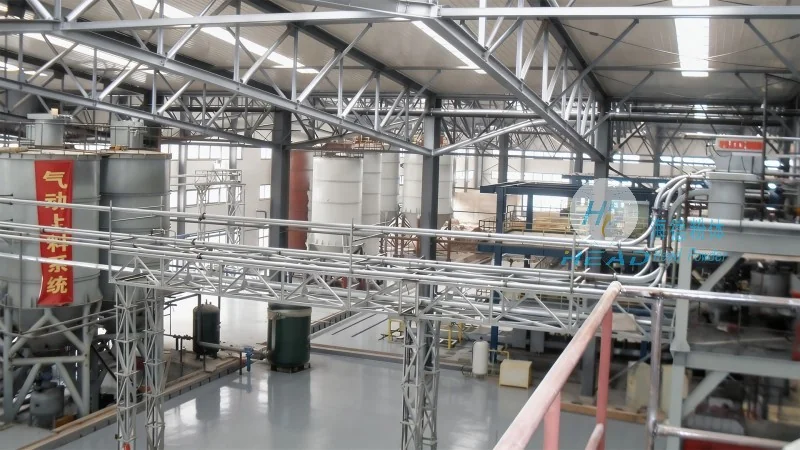
The core principle of the rice husk ash material conveying system is based on the use of a closed-loop or semi-closed-loop conveying mechanism. The system typically employs a combination of screw conveyors, pneumatic conveyors, or a hybrid approach to transport the material from the source to the destination. The screw conveyor, for instance, uses rotating helical blades to move the material forward, while the pneumatic conveyor utilizes air pressure to push or pull the material through a pipeline. The selection of the conveying method depends on factors such as the material's bulk density, moisture content, and the required conveying distance. The system is equipped with sensors and control panels to monitor the flow rate, pressure, and temperature, ensuring optimal performance and preventing blockages or overloading.
Working Scene Characteristics
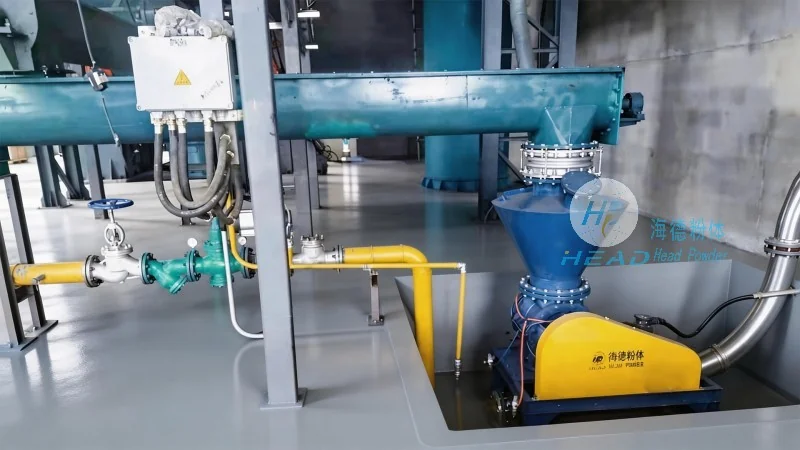
The rice husk ash material conveying system is widely used in industrial settings where rice husk ash is a byproduct of rice processing. The equipment is designed to operate in environments with varying temperatures and humidity levels, making it suitable for both indoor and outdoor installations. The system's compact design allows for easy integration into existing production lines, reducing the need for extensive modifications to the facility. In addition, the system is built with durable materials, such as stainless steel and high-quality plastics, to withstand the abrasive nature of rice husk ash and resist corrosion from moisture or other environmental factors.
Application Examples
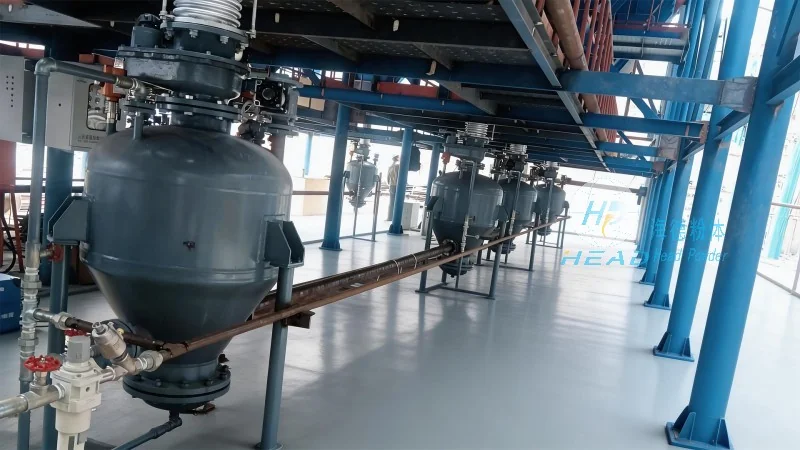
One common application of the rice husk ash material conveying system is in the production of rice husk ash-based products, such as activated carbon or biofuels. The system efficiently transports the ash from the storage silos to the processing units, ensuring a consistent supply of raw material. Another application is in the power generation industry, where rice husk ash is used as a fuel additive in boilers. The conveying system helps maintain a steady flow of ash to the combustion chamber, improving the efficiency of the power generation process. Additionally, the system is used in environmental remediation projects, where rice husk ash is utilized as a soil amendment or for wastewater treatment. The reliable operation of the conveying system is crucial in these applications, as any disruption in the material flow can impact the overall effectiveness of the treatment process.
Advantages and Benefits
The rice husk ash material conveying system offers several advantages over traditional conveying methods. First, it provides a closed system, which helps prevent dust emissions and improves workplace safety. The enclosed design also reduces the risk of material contamination, ensuring the quality of the transported product. Second, the system is energy-efficient, with adjustable speed controls that optimize power consumption based on the material flow rate. This results in lower operational costs and reduced environmental impact. Third, the system is easy to maintain, with accessible components and simple maintenance procedures. Regular inspections and lubrication of the moving parts are sufficient to keep the system running smoothly, minimizing downtime and maintenance expenses.
Conclusion
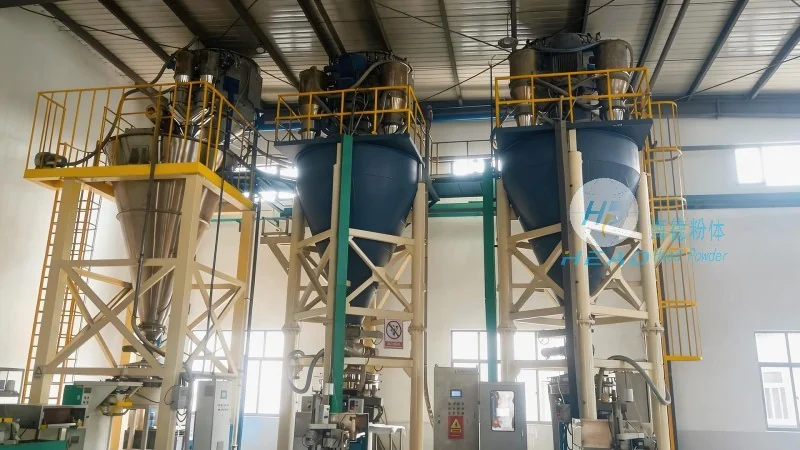
Shandong HeadPowder Engineering Co., Ltd. has developed a reliable and efficient rice husk ash material conveying system that meets the needs of various industrial applications. The system's advanced design and robust construction ensure consistent performance and durability, making it a valuable asset for companies involved in rice husk ash processing. By integrating this equipment into their production lines, businesses can improve operational efficiency, reduce costs, and enhance workplace safety. The rice husk ash material conveying system is a testament to the company's commitment to providing high-quality engineering solutions for the material handling industry.