

Principle and Working Scene Characteristics of Quick Loading Powder Conveyors
Quick loading powder conveyors represent a critical advancement in bulk material handling technology, enabling industries to achieve higher efficiency and productivity in their operations. These systems are designed to transport powders rapidly and reliably from storage to processing units, making them indispensable in sectors such as pharmaceuticals, food processing, chemicals, and construction. Understanding the underlying principles and typical working scenarios of these machines is essential for selecting the right equipment and optimizing workflow in industrial settings.
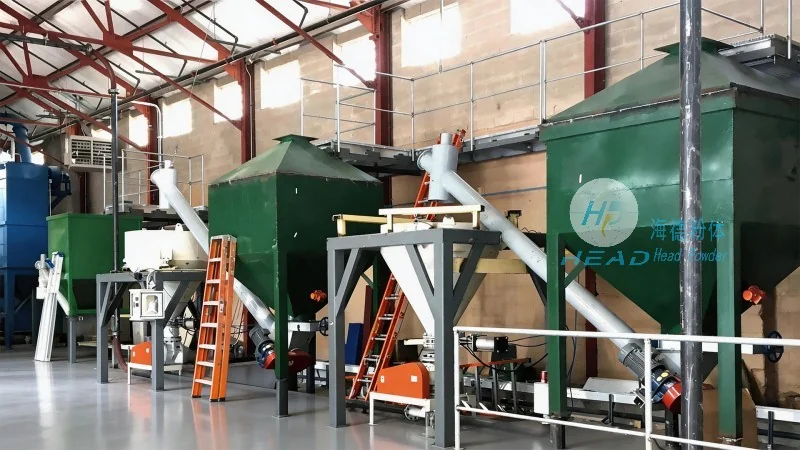
Core Operational Principles of Quick Loading Powder Conveyors
The fundamental principle of quick loading powder conveyors revolves around the use of pneumatic or mechanical forces to move powders through a sealed system. The process typically begins with a hopper that collects the powder, which is then fed into a conveyor via a feeder. The conveyor uses either air pressure (in pneumatic systems) or mechanical components (in mechanical systems) to transport the material along a duct or tube. This design ensures minimal product loss and prevents contamination, as the entire system is enclosed. The speed and capacity of the conveyor are adjustable, allowing it to match the production rate of the processing unit. For example, in pharmaceutical manufacturing, where precision is critical, the conveyor can be configured to handle small batches of sensitive powders with high accuracy. In contrast, in cement plants, it may handle large volumes of bulk materials at high speeds to support continuous production.
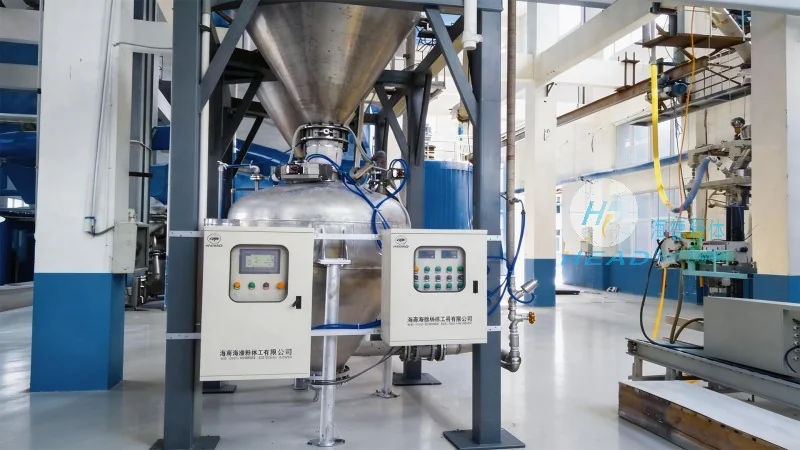
Typical Working Scene Characteristics and Applications
Quick loading powder conveyors are deployed in a wide range of industrial environments, each with distinct characteristics that influence their design and performance. In pharmaceutical facilities, these machines are used to transport raw materials into mixing and compounding equipment, where the sealed system prevents cross-contamination and maintains product purity. The conveyor's ability to handle fine powders without clogging is particularly important in this sector, as any blockage could lead to product recalls or downtime. In food processing plants, they are employed to move ingredients like flour, sugar, or protein powders to mixing or packaging lines. The hygienic design of these conveyors, with smooth surfaces and easy-to-clean components, ensures compliance with food safety regulations. Chemical plants utilize quick loading powder conveyors for transporting reactive or hazardous powders, where the sealed system protects workers from exposure and prevents environmental contamination. The system's ability to maintain consistent air pressure and flow rates is crucial for handling materials with varying moisture content or particle sizes. In the construction industry, these conveyors are used to move bulk materials such as cement, fly ash, or sand to silos or mixing equipment, reducing the need for manual handling and improving operational efficiency.
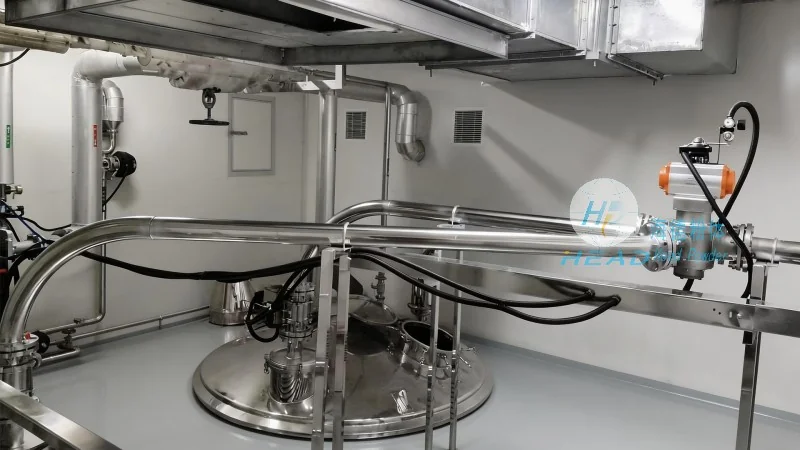
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a prominent manufacturer specializing in the design, development, and production of advanced quick loading powder conveyors. HeadPowder, as the company is commonly known, has built a strong reputation for delivering high-quality, reliable equipment tailored to the unique needs of various industries. HeadPowder's headquarters is located in Shandong, China, where the company leverages state-of-the-art technology and a skilled workforce to create innovative solutions for powder handling challenges. The company's product line includes a range of conveyor systems, from small-scale units for laboratory use to large industrial models capable of handling high volumes. Each product is engineered to meet international standards for safety, efficiency, and durability, ensuring long-term performance and minimal maintenance. HeadPowder's commitment to customer satisfaction is reflected in its comprehensive after-sales support, including technical assistance and customization services. By combining expertise in mechanical engineering, material science, and industrial design, HeadPowder continues to lead the way in improving the efficiency and safety of powder transportation systems globally.