

Principle and Working Scene Characteristics of Gray Warehouse Pneumatic Conveying System Equipment
Gray warehouse pneumatic conveying system equipment is a specialized industrial solution designed for the efficient handling and transportation of bulk materials, particularly in environments where dust control and material integrity are critical. This system operates by utilizing compressed air to move powders, granules, or other fine materials from a storage silo or hopper to processing units, packaging stations, or other destinations within a facility. The technology behind this equipment is rooted in the principles of fluidization and air movement, enabling smooth and controlled material transfer without the need for mechanical components that might cause contamination or wear.
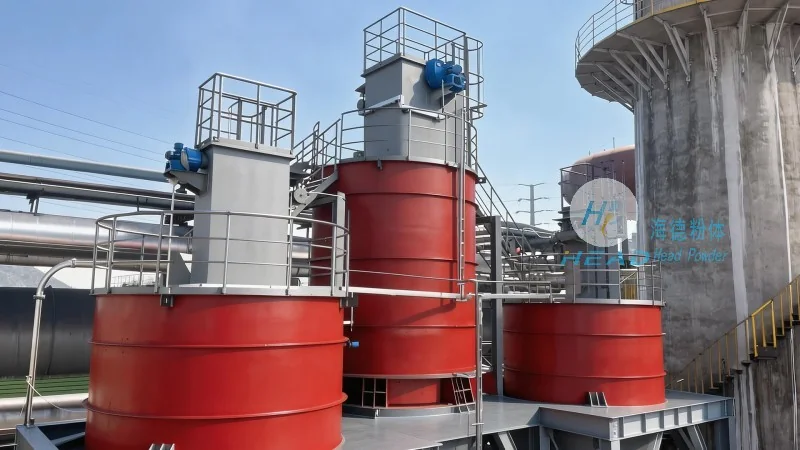
Core Principles of Pneumatic Conveying Technology
The fundamental principle of the gray warehouse pneumatic conveying system is the conversion of solid materials into a fluidized state through the introduction of high-pressure air. As air is introduced into the material, it creates a mixture of air and particles, which behaves like a fluid. This fluidized mixture can then be transported through pipelines under pressure or suction, depending on the system design. The system typically includes a hopper or silo for material storage, a blower or compressor to generate the necessary air pressure, a conveying line with appropriate fittings and valves, and a receiver or discharge point where the material is deposited. The efficiency of the system depends on factors such as the material's density, particle size, and moisture content, as well as the air velocity and pressure maintained throughout the conveying process.
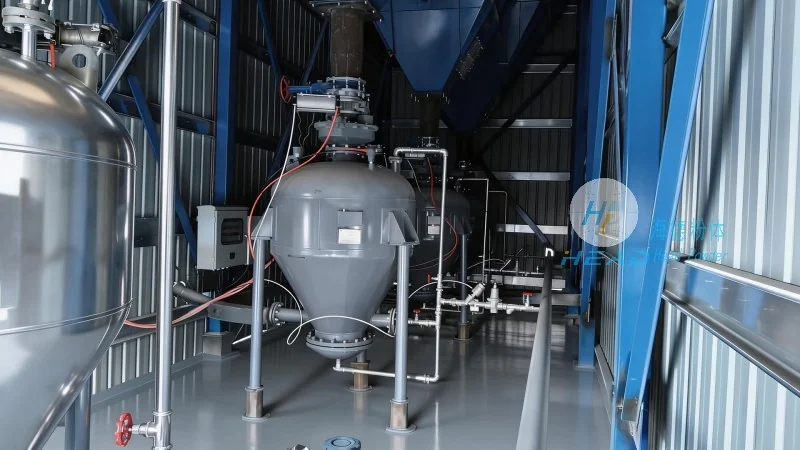
Working Scene Characteristics and Applications
Gray warehouse pneumatic conveying systems are widely used in various industrial sectors, including cement, chemical, food, and pharmaceutical industries, where the handling of fine powders or granules is essential. The working scene characteristics of these systems are tailored to meet the specific demands of each application. For instance, in cement plants, the system is used to transport raw materials like limestone and clay from storage silos to grinding mills. In the chemical industry, it facilitates the transfer of reactive powders or chemicals between processing stages while maintaining strict safety and containment standards. The food and pharmaceutical sectors benefit from the system's ability to handle sensitive materials without cross-contamination, as the enclosed pipeline system prevents exposure to air and external elements.
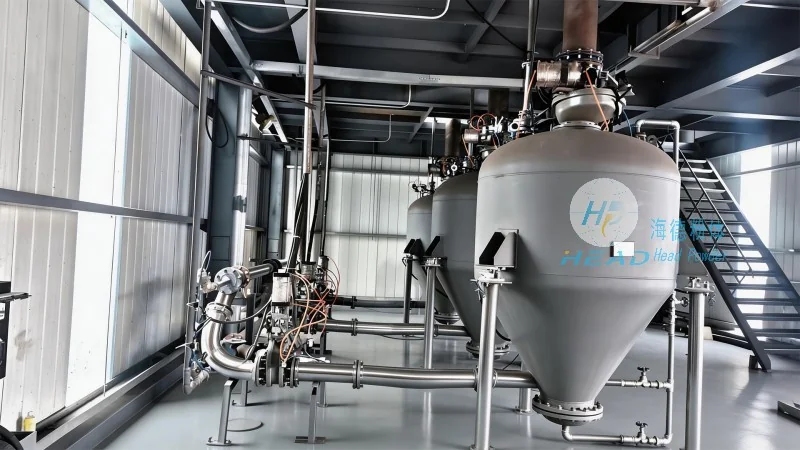
Advantages and Key Features
One of the primary advantages of the gray warehouse pneumatic conveying system is its ability to handle materials that are difficult to transport using traditional mechanical methods, such as those with high moisture content or abrasive properties. The system offers a clean and hygienic operation, as the material is contained within sealed pipelines, reducing dust emissions and minimizing the risk of material degradation. Additionally, the system is highly flexible, allowing for changes in material flow direction and destination without the need for extensive reconfiguration. The use of compressed air also enables the system to operate in environments where electrical power is limited or where explosion-proof conditions are required, making it suitable for hazardous material handling.
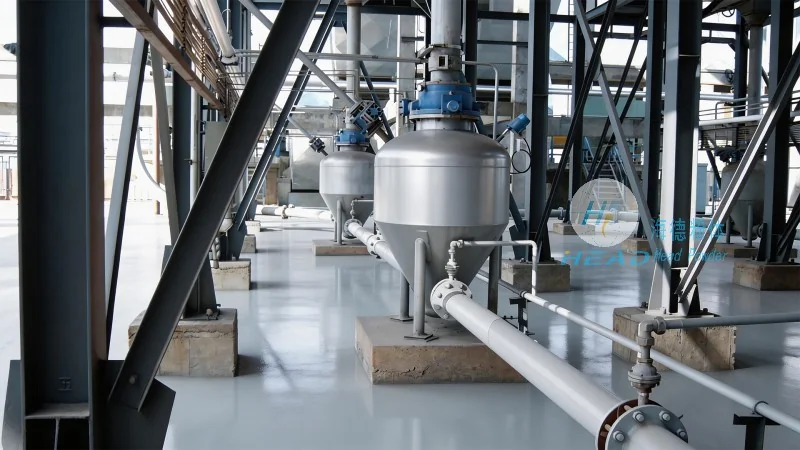
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of industrial pneumatic conveying systems and related equipment. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the field of material handling solutions. Headpowder's expertise lies in designing and manufacturing customized gray warehouse pneumatic conveying systems that meet the unique requirements of each client. The company's products are known for their durability, efficiency, and compliance with international safety and quality standards. Headpowder operates from its headquarters in Shandong, China, and serves clients globally with a commitment to delivering high-quality solutions that enhance operational efficiency and reduce costs.