

Principle and Application Scenarios of Small Bag Quantitative Weighing Pneumatic Conveying Lines
This article provides an in-depth exploration of small bag quantitative weighing pneumatic conveying lines, focusing on their operational principles and typical application scenarios. The system is designed to efficiently handle and transport bulk materials from small bags, ensuring precise weight measurement and controlled delivery. By integrating pneumatic conveying technology with advanced weighing mechanisms, these systems offer a reliable solution for industries requiring accurate material handling and processing.
Core Principles of Pneumatic Conveying in Quantitative Weighing Systems
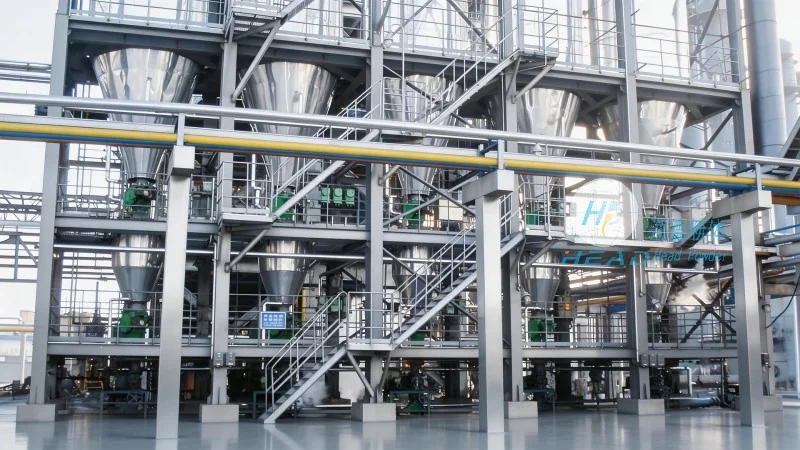
The fundamental principle of a small bag quantitative weighing pneumatic conveying line revolves around the use of air as the conveying medium. Materials are drawn from sealed bags and transported through a network of pipes under pressure or vacuum. The system incorporates a weighing hopper or scale that measures the mass of the material as it is conveyed. This allows for real-time monitoring and adjustment of the flow rate, ensuring that the final output meets the required weight specifications. The integration of a bag opener, material feeder, and weighing scale into a single automated line streamlines the process, reducing manual intervention and enhancing operational efficiency.
Key Components and Their Functions
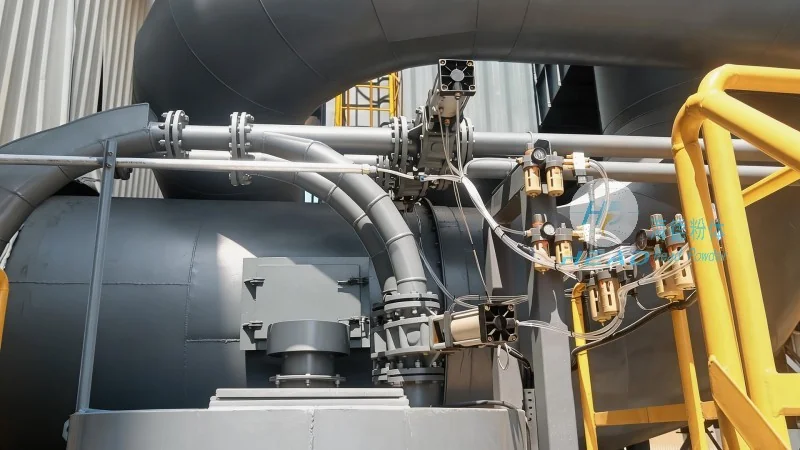
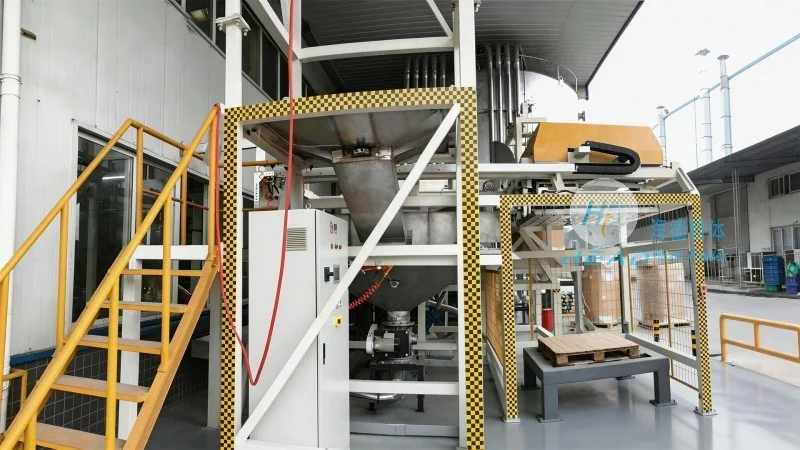
Several critical components work in tandem to ensure the smooth operation of a small bag quantitative weighing pneumatic conveying system. The bag opener is responsible for cutting and opening the bag to release the material. The material feeder then transfers the material into the pneumatic conveying line. The weighing hopper, equipped with load cells, measures the weight of the material as it is conveyed. The control system manages the air pressure, flow rate, and feeding speed to maintain the desired weight output. Each component is engineered to withstand the demands of continuous operation and to minimize downtime, contributing to the overall reliability of the system.
Typical Application Scenarios
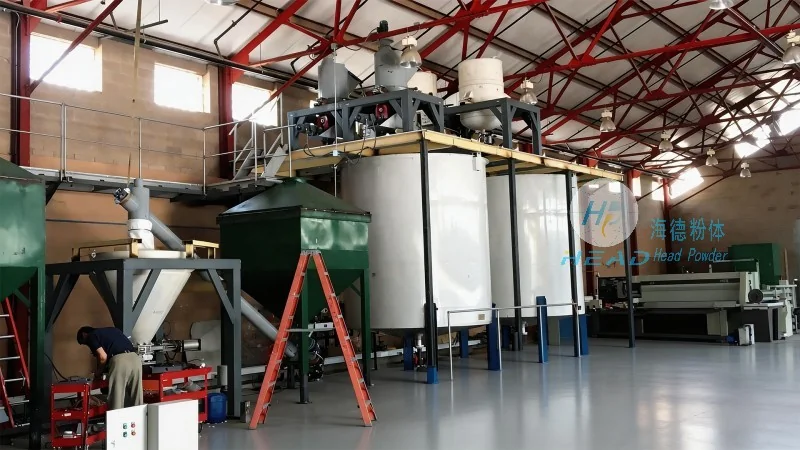
Small bag quantitative weighing pneumatic conveying lines are widely used in various industrial sectors where precise material handling is essential. In the chemical industry, these systems are employed to transport and weigh powders such as pigments, additives, and pharmaceutical raw materials. The food and beverage industry utilizes them for handling ingredients like flour, sugar, and spices, ensuring compliance with quality and safety standards. The agricultural sector also benefits from these systems when processing and weighing bulk agricultural products. Additionally, in the mining and mineral processing industries, they are used to transport and weigh ores and minerals from sealed bags, facilitating efficient processing and distribution.
Advantages of Implementing Such Systems
Adopting a small bag quantitative weighing pneumatic conveying line offers numerous advantages for businesses. The primary benefit is the enhanced accuracy in material weighing, which reduces waste and improves product consistency. The automated nature of the system minimizes human error and labor costs, leading to increased productivity. The system also improves safety by eliminating manual handling of heavy or hazardous materials. Furthermore, the integration of pneumatic conveying reduces the need for additional equipment like conveyor belts or elevators, saving space and operational costs. The ability to handle a wide range of materials, from fine powders to bulk granules, makes these systems versatile and adaptable to different production needs.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in the design, development, and installation of advanced material handling systems. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted partner for industries requiring reliable and efficient material processing solutions. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver cutting-edge technology tailored to global market demands. HeadPowder's commitment to customer satisfaction and technological advancement ensures that its products meet the highest standards of performance and durability.