

Working Principle and Features of Fully Automatic Powder Pneumatic Conveying Systems
For industrial applications requiring efficient and reliable material handling, fully automatic powder pneumatic conveying systems offer a sophisticated solution. These systems are designed to transport bulk powders and granular materials through an enclosed pipeline using air as the conveying medium. Understanding the working principle and key features of such systems is essential for selecting the right equipment for specific operational needs.
Working Principle of Fully Automatic Powder Pneumatic Conveying Systems
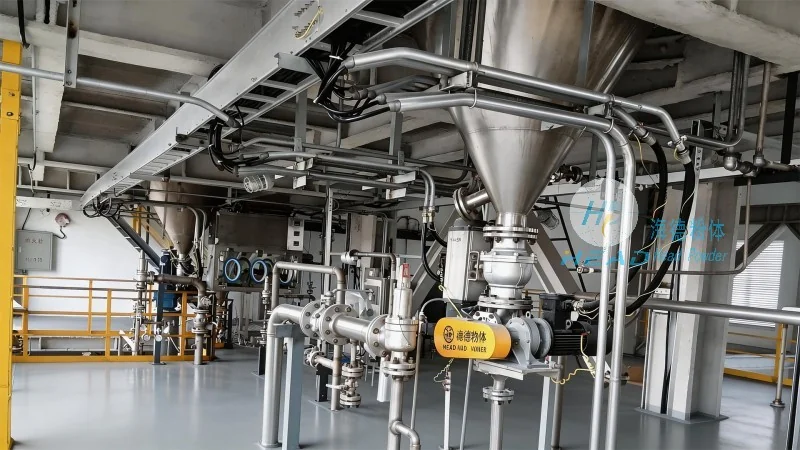
The core mechanism of fully automatic powder pneumatic conveying systems involves the use of compressed air to create a flow that propels the material through the pipeline. The process typically begins with the material being fed into a hopper or feeder, where it is then introduced into the conveying line. Compressed air, generated by a blower or compressor, is introduced at the inlet of the pipeline, creating a pressure differential that draws the material along with the air stream. As the material travels through the pipeline, it is carried by the air flow, which can be either positive pressure (where air pushes the material) or negative pressure (where air pulls the material). The system is equipped with various components such as airlocks, cyclones, and filters to control the flow and separate the material from the air. The entire operation is automated, allowing for consistent and continuous material transport without manual intervention.
Key Features of Fully Automatic Powder Pneumatic Conveying Systems
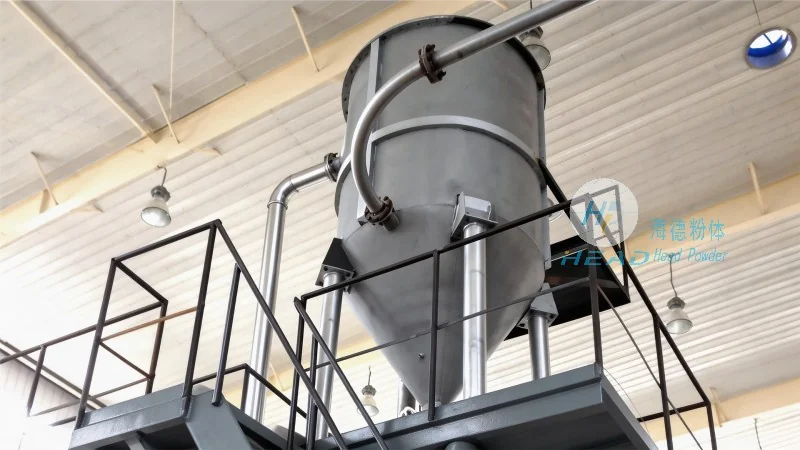
One of the primary advantages of fully automatic powder pneumatic conveying systems is their high efficiency in material handling. These systems can transport materials over long distances with minimal loss and contamination, making them suitable for applications in pharmaceuticals, food processing, and chemical industries. The automation aspect ensures consistent performance, reducing the risk of human error and improving operational reliability. Additionally, these systems are designed for easy maintenance and cleaning, which is crucial for industries with strict hygiene standards. The use of enclosed pipelines prevents dust emissions, contributing to a safer working environment and compliance with environmental regulations. Another notable feature is the flexibility in handling different types of powders, from fine powders to bulk granules, by adjusting the air pressure and flow rate. This adaptability makes the systems versatile for various industrial processes.
Applications and Benefits in Industrial Settings
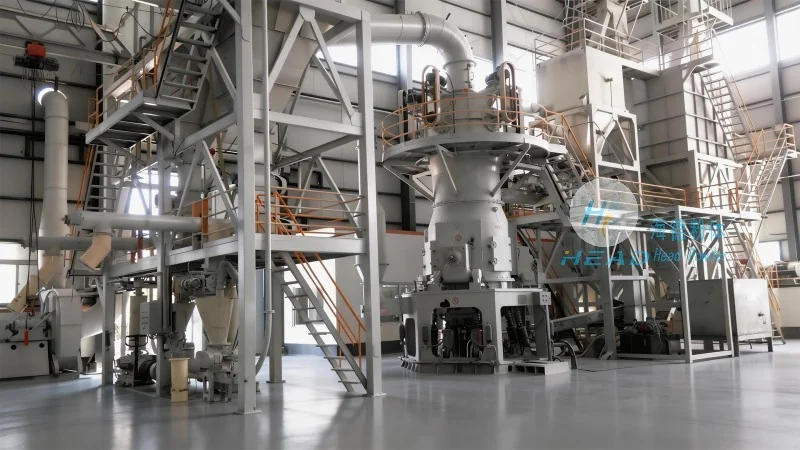
Fully automatic powder pneumatic conveying systems are widely used in industries where material transport needs to be precise and controlled. In the pharmaceutical sector, these systems ensure the safe and hygienic handling of active pharmaceutical ingredients (APIs) and excipients, maintaining product integrity and meeting regulatory requirements. In the food industry, they are employed to transport ingredients like flour, sugar, and spices, preserving the quality and freshness of the products. The chemical industry also benefits from these systems when handling powders such as pigments, catalysts, and reagents, where contamination control is critical. The benefits extend beyond operational efficiency to include cost savings through reduced labor and lower material waste. By minimizing the need for manual handling, these systems also enhance workplace safety by eliminating exposure to dust and hazardous materials.
Customization and Integration with Existing Systems
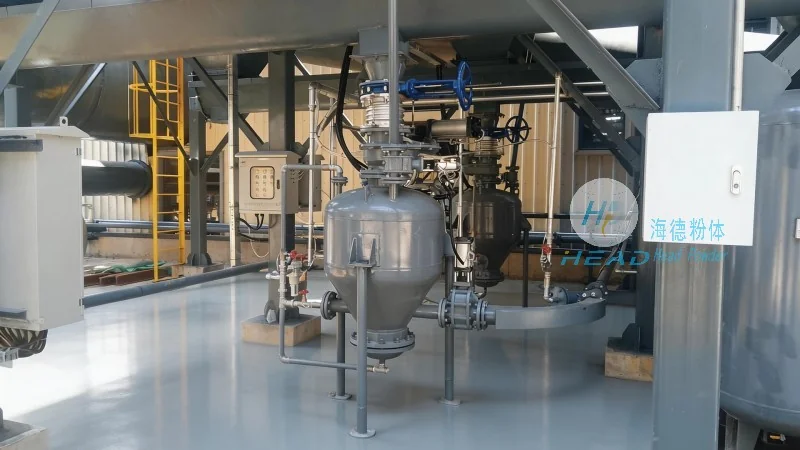
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, offers fully automatic powder pneumatic conveying systems tailored to meet specific customer requirements. The company specializes in designing and manufacturing customized solutions that integrate seamlessly with existing industrial setups. Their expertise lies in understanding the unique needs of each application, ensuring that the conveying systems are optimized for performance and reliability. The systems can be integrated with various feeding mechanisms, such as screw feeders or vibratory feeders, and connected to downstream processing equipment like mixers or reactors. This integration allows for a streamlined workflow, enhancing overall production efficiency. Additionally, the company provides comprehensive support, including installation, commissioning, and after-sales service, to ensure that the systems operate at peak performance. With a focus on quality and innovation, Shandong HeadPowder Engineering Co., Ltd. delivers solutions that meet the highest industry standards, making them a trusted partner for businesses seeking reliable material handling solutions.