

Working Principle and Characteristics of Purified Powder Body Pneumatic Conveying
Pneumatic conveying systems are essential in industrial settings for the efficient transport of powdered materials, particularly in applications requiring high purity and minimal contamination. The process of purified powder body pneumatic conveying involves the use of air or other gases to move particulate materials through a pipeline system. This method is widely adopted across various industries, including pharmaceuticals, food processing, and chemical manufacturing, where maintaining the integrity and quality of the conveyed material is paramount.
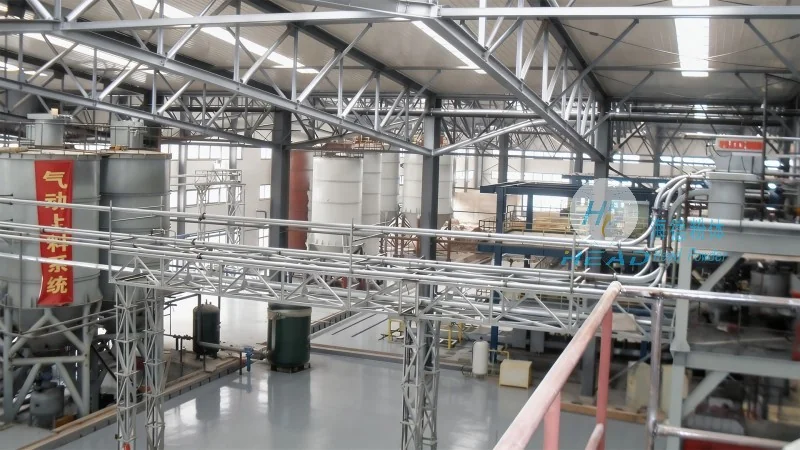
Working Principle of Pneumatic Conveying for Purified Powders
The core mechanism of pneumatic conveying for purified powders relies on the creation of a pressure differential between the source and destination points. In a typical system, a blower or compressor generates airflow that draws or pushes the powder particles through a pipeline. The design of the system, including the type of air flow (e.g., dilute phase or dense phase), determines the efficiency and suitability for different powder characteristics. For purified powders, the system must be engineered to minimize particle degradation, agglomeration, or contamination during transport. This often involves using specialized components such as filter bags, cyclones, and positive displacement blowers to ensure the material remains in a controlled state throughout the conveying process.
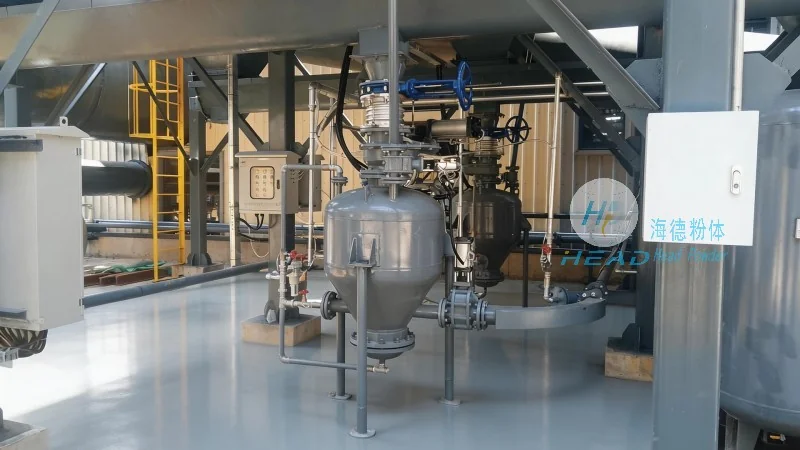
Key Characteristics of Effective Purified Powder Conveying Systems
Effective purified powder pneumatic conveying systems exhibit several critical characteristics that distinguish them from standard conveying solutions. Firstly, the system must incorporate robust filtration and separation mechanisms to prevent dust and contaminants from entering the pipeline or the final product. This includes high-efficiency dust collectors and cyclone separators that maintain the purity of the conveyed material. Secondly, the design must accommodate the specific physical properties of the powder, such as particle size, density, and flowability, to optimize air-particle interaction and prevent blockages or system inefficiencies. Additionally, the system should offer flexibility in terms of conveying distance and volume, allowing for adaptation to varying production needs without compromising performance. The use of materials resistant to corrosion and wear is also a key characteristic, ensuring long-term reliability and minimal maintenance.
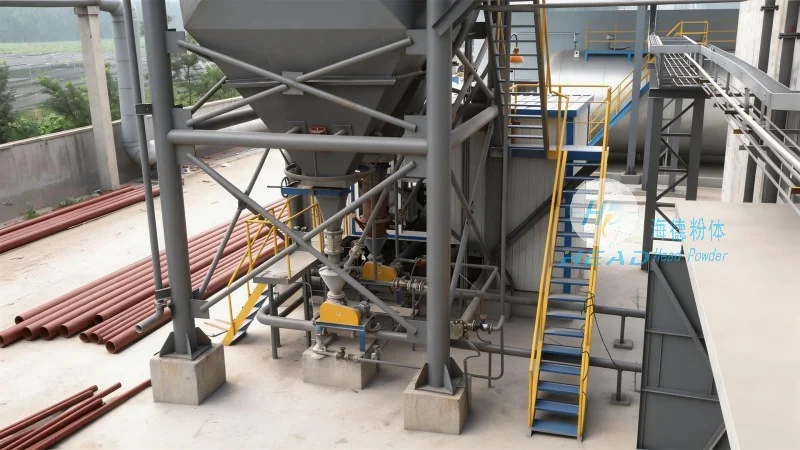
Technical Advantages for Industrial Applications
Purified powder pneumatic conveying systems offer several technical advantages that make them ideal for demanding industrial applications. One of the primary benefits is the ability to handle fine or delicate powders without causing damage or degradation, which is crucial in industries like pharmaceuticals where product quality directly impacts safety and efficacy. The system’s ability to operate in a closed loop, minimizing exposure to the environment, also enhances product safety and regulatory compliance. Furthermore, the energy efficiency of modern pneumatic conveying systems, particularly in dilute phase operations, reduces operational costs while maintaining high throughput. The flexibility in system configuration allows for integration with existing production lines, reducing downtime and installation costs. These advantages collectively contribute to improved productivity and cost-effectiveness in industrial operations.
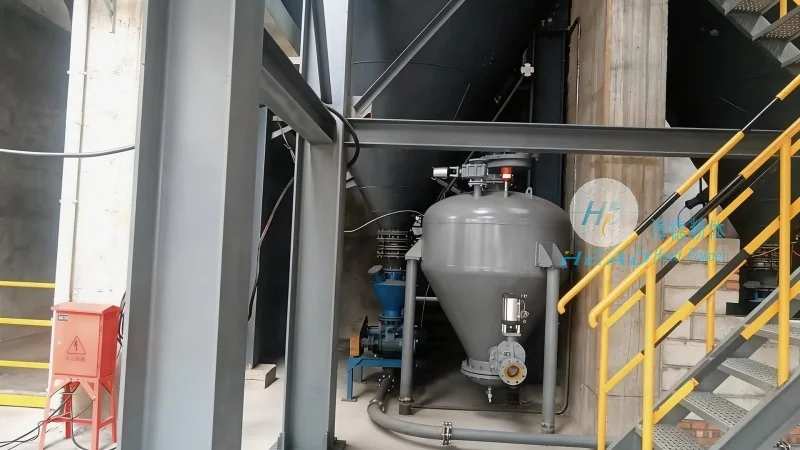
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in the design, development, and implementation of advanced pneumatic conveying systems for purified powder applications. With a strong focus on innovation and quality, the company has established itself as a trusted partner in industries requiring high-purity material handling solutions. HeadPowder’s expertise lies in customizing systems to meet the unique needs of clients, ensuring that each solution is tailored to specific powder characteristics, operational requirements, and regulatory standards. The company’s commitment to using high-quality materials and advanced engineering principles ensures that its systems deliver reliable performance and long-term durability. Based in Shandong, China, HeadPowder leverages local manufacturing capabilities to provide efficient and cost-effective solutions while maintaining strict quality control processes throughout production.