

Working Principle and Features of Manganese Carbonate Powder Handling Equipment
For industries dealing with manganese carbonate powders, efficient and reliable handling equipment is crucial for maintaining production efficiency and product quality. Manganese carbonate, a key raw material in various industrial applications, requires specialized equipment to ensure safe and effective transport. This article explores the working principle and key features of manganese carbonate powder handling equipment, providing insights into how such systems operate and the advantages they offer.
Company Information
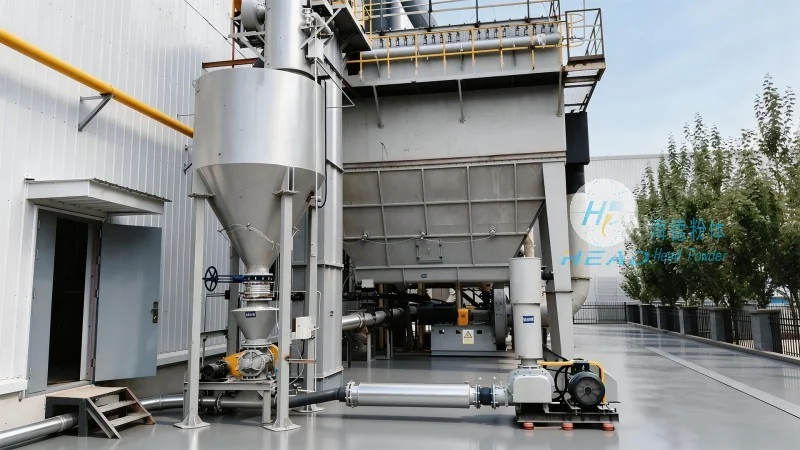
HeadPowder, a leading manufacturer in the field, specializes in providing advanced solutions for powder handling. Based in Shandong, China, the company combines expertise in material science and engineering to develop equipment tailored to the unique properties of manganese carbonate. Their products are designed to meet the demands of modern industrial processes, ensuring durability, efficiency, and compliance with safety standards.
Working Principle of Manganese Carbonate Powder Handling Equipment
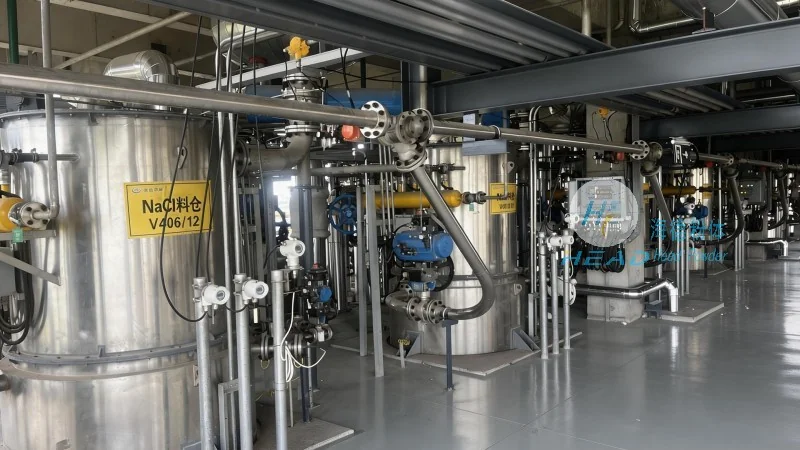
The core working principle of manganese carbonate powder handling equipment revolves around the use of pneumatic or mechanical systems to transport the fine powder. Pneumatic conveying systems, for instance, utilize compressed air to move the powder through pipelines, while mechanical systems may employ screw conveyors, belt conveyors, or bucket elevators. The choice of system depends on factors such as the particle size, moisture content, and the distance the powder needs to be transported. In pneumatic systems, the powder is suspended in the air stream and carried to the destination, often using a combination of positive and negative pressure to control the flow. Mechanical systems, on the other hand, rely on the physical movement of components like screws or belts to move the powder, which is particularly effective for larger particles or when air quality constraints are a concern.
Key Features of Manganese Carbonate Powder Handling Equipment
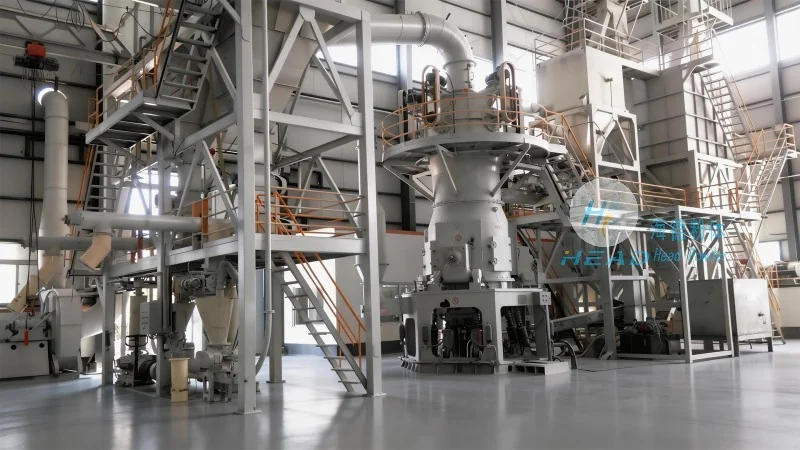
Effective manganese carbonate powder handling equipment exhibits several critical features that enhance performance and safety. Firstly, it must ensure minimal dust generation and proper containment to prevent environmental contamination and health hazards. Advanced equipment often includes dust collection systems and sealed containers to maintain a clean working environment. Secondly, the equipment is designed for high efficiency, minimizing material loss and optimizing throughput. This is achieved through precise control of flow rates and pressure, ensuring that the powder is transported without clogging or degradation. Thirdly, durability is a key consideration, as manganese carbonate can be abrasive and may cause wear on equipment components. High-quality materials and robust construction are essential to extend the equipment's lifespan and reduce maintenance costs. Additionally, safety features such as emergency shut-off valves and overload protection mechanisms are integrated to prevent accidents and ensure operator safety. The equipment also often includes monitoring systems to track performance metrics, allowing for real-time adjustments and maintenance scheduling.
Conclusion
Manganese carbonate powder handling equipment plays a vital role in the efficient processing of this important industrial material. By understanding the working principles and key features of such systems, industries can select the most appropriate equipment to meet their specific needs. HeadPowder, with its expertise and commitment to quality, offers reliable solutions that enhance productivity while maintaining safety and environmental standards. As the demand for manganese carbonate continues to grow, the importance of advanced powder handling technology becomes increasingly evident, making it a critical investment for any company operating in this sector.