

Working Principle and Features of Calcined Ash Powder Conveying Equipment
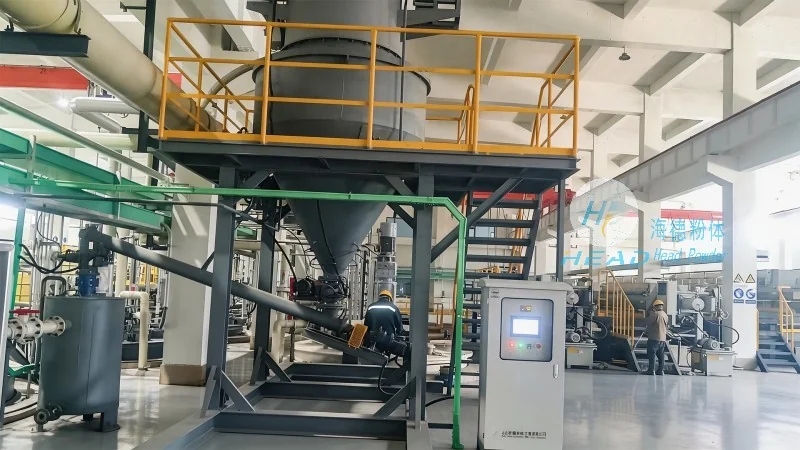
Calcined ash, a byproduct from the combustion of coal in thermal power plants, requires efficient and reliable handling systems for its transport and processing. The calcined ash powder conveying equipment developed by Shandong HeadPowder Engineering Co., Ltd. addresses these needs through a sophisticated design that ensures safe, efficient, and low-maintenance operation. This article explores the working principle and key features of this equipment, highlighting its suitability for industrial applications.
Overview of the Equipment
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in providing advanced solutions for powder handling and material transport. The calcined ash powder conveying equipment is engineered to handle the unique properties of calcined ash, including its fine particle size, potential moisture content, and abrasive nature. The company’s headquarters is located in Shandong, China, where they leverage local expertise and advanced manufacturing capabilities to produce high-quality equipment.
Working Principle of the Calcined Ash Powder Conveying Equipment
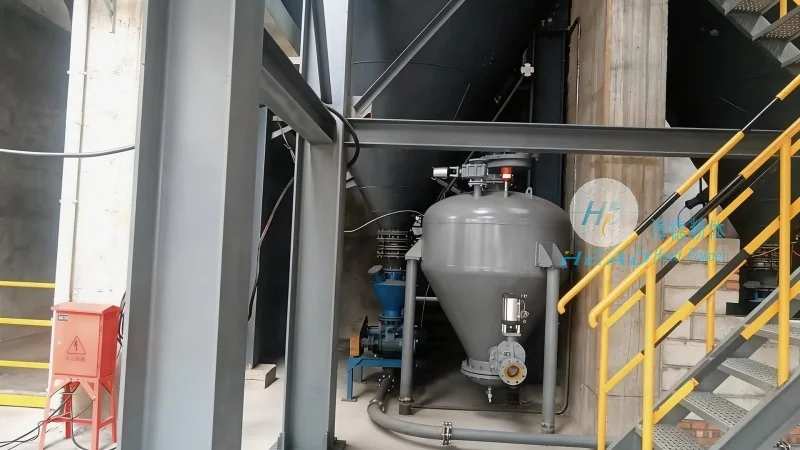
The equipment operates on the principle of pneumatic or mechanical conveying, depending on the specific design and application requirements. For pneumatic systems, the process typically involves the use of a blower or compressor to generate airflow that transports the calcined ash particles through a pipeline. The system includes components such as a hopper for material storage, a feeder to control the flow rate, and a pipeline network that directs the material to the destination. Mechanical systems, on the other hand, utilize screw conveyors, belt conveyors, or bucket elevators to move the ash, often with the addition of air assistance to reduce friction and improve efficiency. The working principle is designed to minimize material degradation, prevent blockages, and ensure consistent flow rates, which are critical for maintaining the quality of the calcined ash and the longevity of the equipment.
Key Features of the Equipment
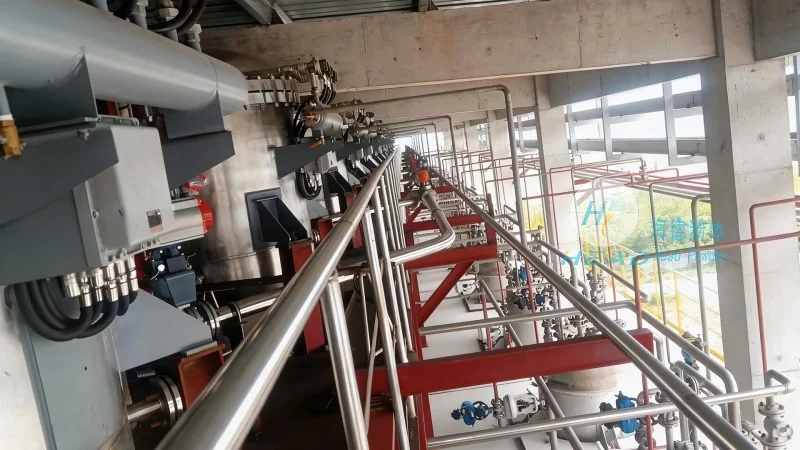
The calcined ash powder conveying equipment from Shandong HeadPowder Engineering Co., Ltd. incorporates several key features that enhance its performance and reliability. One of the primary features is its robust construction, which is built to withstand the abrasive nature of calcined ash and the high pressures associated with pneumatic conveying. The equipment includes wear-resistant components, such as lined hoppers and pipelines, to extend the service life and reduce maintenance costs. Another important feature is the advanced control system, which allows for precise regulation of the material flow rate, pressure, and temperature. This system ensures optimal operation and helps prevent overloading or underloading of the conveyor, thereby improving overall efficiency. Additionally, the equipment is designed for easy maintenance, with accessible components and modular design that facilitate quick repairs and replacements. The company’s commitment to quality is evident in the use of high-grade materials and rigorous testing procedures, ensuring that each unit meets the highest standards of performance and safety.
Advantages in Industrial Applications
The calcined ash powder conveying equipment offers significant advantages in industrial settings, particularly in power plants and waste management facilities. By efficiently transporting calcined ash from storage areas to processing or disposal sites, the equipment helps streamline operations and reduce labor costs. The low maintenance requirements and long service life of the equipment contribute to lower operational expenses over time. Furthermore, the equipment’s ability to handle fine particles without clogging or degradation ensures that the quality of the calcined ash is preserved, which is essential for downstream processes such as cement production or soil amendment. The reliability of the system also minimizes downtime, which is critical for maintaining production schedules and meeting environmental regulations. Overall, the equipment provides a cost-effective and sustainable solution for handling calcined ash, aligning with the industry’s need for efficient and environmentally responsible material transport.
Conclusion
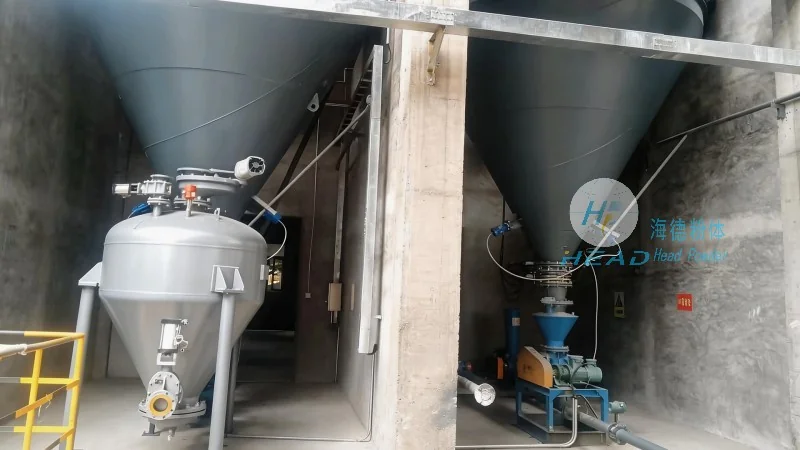
Shandong HeadPowder Engineering Co., Ltd. has developed a highly effective calcined ash powder conveying equipment that combines advanced technology with robust construction. The working principle, which may involve pneumatic or mechanical conveying, is designed to handle the unique challenges of calcined ash, ensuring efficient and reliable transport. Key features such as wear resistance, precise control systems, and easy maintenance make the equipment a preferred choice for industrial applications. With its headquarters in Shandong, China, the company leverages local expertise and manufacturing capabilities to deliver high-quality solutions that meet the demands of modern power and waste management industries. The equipment’s advantages in reducing operational costs, preserving material quality, and minimizing downtime make it an essential component for any facility dealing with calcined ash.