

Working Principle and Features of Multi-Hopper Powder Conveying Systems
Multi-hopper pneumatic conveying systems represent a sophisticated solution for the efficient handling and transportation of bulk powders in industrial settings. As a key component in material processing, these systems are designed to address the challenges associated with moving dry, fine materials over long distances or within complex facility layouts. The core of such systems lies in the multi-hopper design, which allows for the sequential or simultaneous feeding of different powder types, enhancing operational flexibility and system reliability.
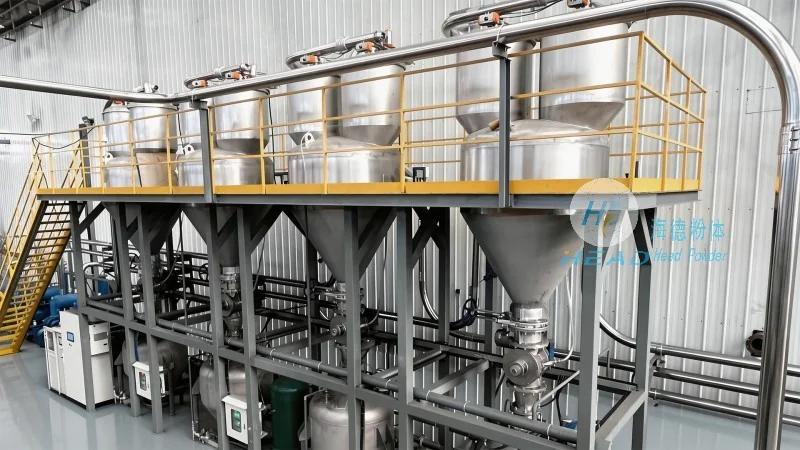
Working Principle of Multi-Hopper Powder Conveying Systems
The operation of a multi-hopper powder conveying system is based on the principles of pneumatic conveying, where air is used as the conveying medium to transport powders through a network of pipes. The system typically consists of multiple hoppers, each containing a distinct type of powder, a feeding mechanism (such as a rotary valve or screw feeder), and a common conveying line. When the system is activated, air is drawn into the hoppers, creating a negative pressure that lifts the powder particles into the conveying line. The air then carries the powder through the pipeline to the discharge point, where the material is deposited. The multi-hopper configuration enables the system to switch between different powders without the need for extensive system modifications, as each hopper can be isolated and controlled independently. This flexibility is achieved through the use of control valves and sensors that monitor the flow rate and pressure within the system, ensuring smooth and consistent operation.
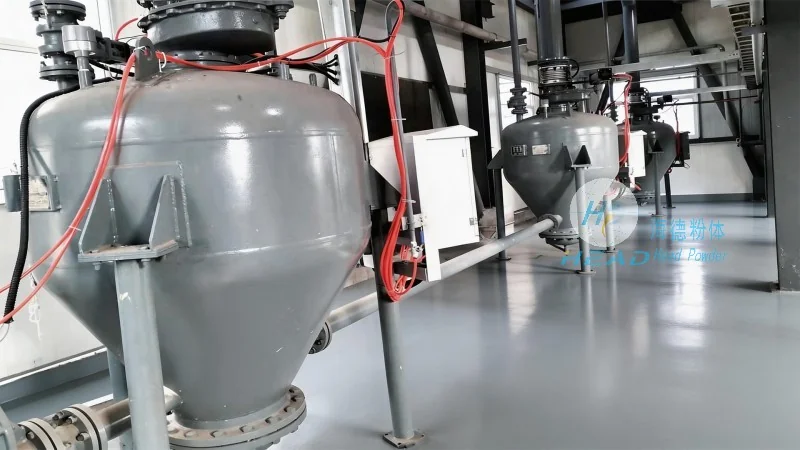
Key Features of Multi-Hopper Powder Conveying Systems
Multi-hopper powder conveying systems offer several distinct advantages that make them ideal for a wide range of industrial applications. One of the primary features is the ability to handle multiple powder types simultaneously, which is particularly beneficial in facilities that process diverse materials, such as chemicals, food products, or pharmaceuticals. This capability reduces downtime and increases overall productivity by eliminating the need to shut down the system for material changes. Another significant feature is the system's high efficiency in terms of energy consumption and material transfer. By using compressed air as the conveying medium, the system minimizes the risk of material degradation and contamination, which is critical for sensitive products. Additionally, the multi-hopper design provides excellent control over the flow rate and pressure, allowing for precise dosing and delivery of powders to downstream processes. This level of control is essential for applications that require consistent material quality and uniformity, such as in the production of coatings, inks, or bulk chemicals.
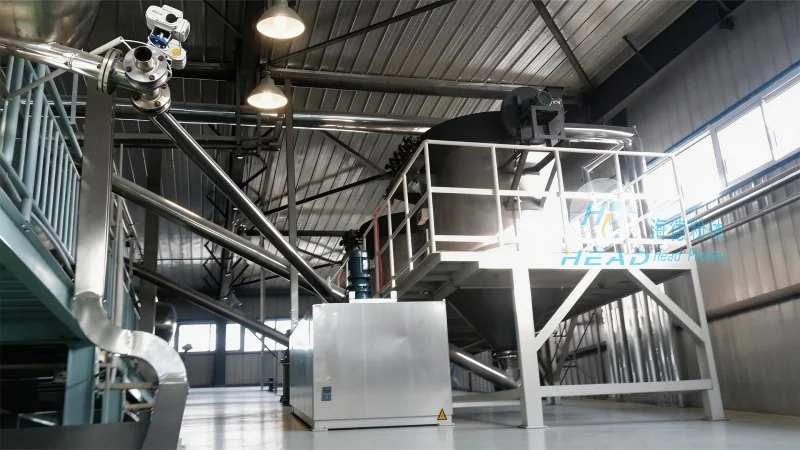
Applications and Benefits in Industrial Settings
Multi-hopper powder conveying systems are widely used in various industries, including chemical manufacturing, food processing, pharmaceuticals, and mining. In chemical plants, these systems are employed to transport raw materials and intermediates between processing units, ensuring a continuous and safe material flow. In the food industry, the systems are used to handle ingredients like flour, sugar, and spices, maintaining hygiene standards and preventing cross-contamination. The pharmaceutical sector benefits from the system's ability to handle sensitive powders, such as active pharmaceutical ingredients (APIs), while preserving their purity and integrity. The mining industry utilizes multi-hopper systems to transport bulk minerals and ores from storage hoppers to processing equipment, improving operational efficiency and reducing labor costs. The benefits of these systems extend beyond material handling, as they also contribute to improved safety by reducing manual handling of powders and minimizing the risk of dust explosions through proper air management.
Technical Advantages and Customization Options
From a technical standpoint, multi-hopper powder conveying systems offer several advantages that enhance their performance and adaptability. The use of multiple hoppers allows for the integration of different conveying technologies, such as pressure and vacuum conveying, within a single system. This flexibility enables the system to handle a broad range of powder characteristics, including varying particle sizes, densities, and flowability. The control systems employed in these systems are typically advanced, incorporating sensors and automation to monitor and adjust the conveying process in real-time. This ensures optimal performance and reduces the likelihood of system failures or material blockages. Additionally, the systems can be customized to meet specific customer requirements, such as the addition of filters, cyclones, or dust collection equipment to meet environmental regulations. The customization options also include the ability to integrate with existing facility infrastructure, minimizing installation time and costs. The result is a system that is not only efficient but also adaptable to changing production needs and evolving industry standards.
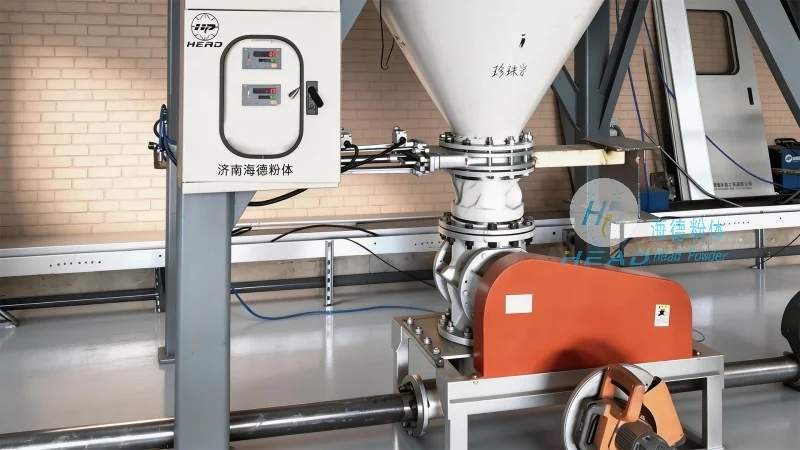
Conclusion and Company Overview
Multi-hopper powder conveying systems represent a highly effective solution for the efficient and reliable transportation of bulk powders in industrial applications. By combining the principles of pneumatic conveying with a multi-hopper design, these systems offer enhanced flexibility, control, and efficiency compared to traditional material handling methods. The key features, including the ability to handle multiple powder types, precise flow control, and energy efficiency, make them a preferred choice for industries that demand high-quality, consistent material handling. As a leading provider of engineering solutions for powder handling, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing these systems to meet the unique needs of its clients. With a focus on innovation and customer satisfaction, the company ensures that its products are built to the highest standards of quality and reliability, providing long-term value and performance for industrial operations.