

What is Cement Raw Material Powder Pneumatic Conveying? What are the Design Principles?
Cement raw material powder pneumatic conveying is a crucial technology in the cement industry, enabling the efficient and safe transportation of bulk powders like raw materials from one location to another. This method involves using air as the conveying medium to move particles through a pipeline system, eliminating the need for mechanical components such as belts or buckets that are common in traditional bulk material handling. The process is widely adopted in cement production facilities due to its ability to handle large volumes of material while maintaining a high level of operational efficiency and flexibility.
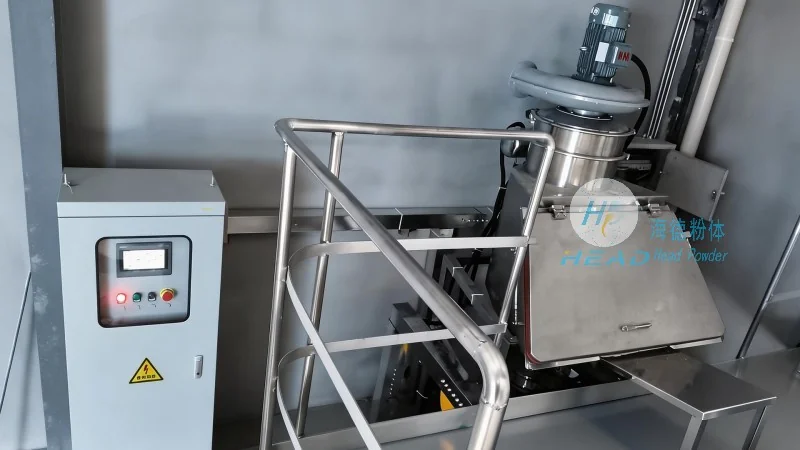
Understanding Cement Raw Material Powder Pneumatic Conveying
Pneumatic conveying systems for cement raw materials operate by creating a pressure differential or using vacuum to move the powder through a pipeline. The system typically consists of a feeding device, a conveying line, a separation or collection unit, and a control system. The feeding device, often a rotary valve or a screw feeder, introduces the raw material into the pipeline. As air is introduced, it lifts and transports the particles, which are then separated from the air at the receiving end. This separation is achieved through cyclones, filters, or other separation equipment, ensuring that the material is delivered to the target location without contamination or loss.
The Core Design Principles of Cement Raw Material Powder Pneumatic Conveying Systems
The design of a cement raw material powder pneumatic conveying system is based on several key principles that ensure optimal performance and reliability. First, the system must be capable of handling the specific properties of the raw material, such as particle size, density, and moisture content. These properties influence the selection of the conveying method—whether it's a positive pressure system (where air is forced into the line) or a negative pressure system (where air is drawn out). The choice of system type depends on factors like the distance to be covered, the volume of material to be conveyed, and the need for dust control. Second, the pipeline design is critical. The diameter and length of the pipeline, along with the number of bends and fittings, must be optimized to minimize pressure drop and prevent particle segregation or blockages. Properly sized and positioned cyclones or filters are essential for efficient separation and to maintain the system's efficiency over time. Third, the system must incorporate safety features to prevent dust explosions, which are a significant hazard in powder handling. This includes explosion-proof components, proper ventilation, and monitoring systems. Finally, the control system plays a vital role in regulating the flow rate, pressure, and other parameters to ensure smooth operation and prevent equipment damage.
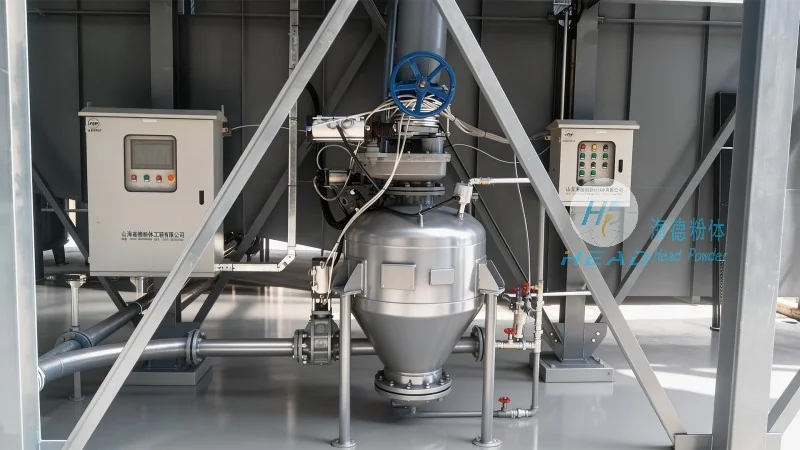
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of engineering solutions for bulk material handling, with a strong focus on cement raw material processing. HeadPowder specializes in the design, manufacturing, and installation of pneumatic conveying systems tailored to the unique needs of the cement industry. The company's expertise lies in understanding the complex requirements of cement production, from raw material storage and feeding to final product handling. HeadPowder's team of engineers and technicians work closely with clients to develop customized solutions that enhance operational efficiency, reduce downtime, and improve overall productivity. The company's commitment to quality and innovation has made it a trusted partner for many cement manufacturers worldwide.
Key Features and Advantages of HeadPowder's Pneumatic Conveying Solutions
HeadPowder's pneumatic conveying systems for cement raw materials offer several advantages that set them apart from traditional handling methods. One of the primary benefits is the elimination of mechanical wear and tear, as there are no moving parts in direct contact with the material. This reduces maintenance costs and extends the lifespan of the equipment. Additionally, pneumatic conveying systems can handle a wide range of particle sizes and shapes, including fine powders and coarse materials, without causing segregation or degradation. The systems are also highly flexible, allowing for easy integration with existing plant layouts and future expansion. Another key advantage is the ability to control dust emissions, which is crucial for maintaining a safe and healthy working environment. HeadPowder's systems incorporate advanced dust collection and filtration technologies to ensure compliance with environmental regulations and to protect personnel from respiratory hazards. Furthermore, the systems are designed for energy efficiency, with optimized air flow and pressure control that minimize energy consumption while maximizing conveying capacity.

Applications and Case Studies
HeadPowder's pneumatic conveying solutions have been successfully implemented in numerous cement production facilities across China and other regions. These systems have been used to transport raw materials such as limestone, clay, and iron ore from storage silos to the raw mill, and from the mill to the kiln. The systems have demonstrated significant improvements in material handling efficiency, with reduced downtime and increased throughput compared to traditional methods. For example, one client reported a 20% increase in production capacity after implementing HeadPowder's pneumatic conveying system, while also reducing maintenance costs by 15%. Another case study involved a cement plant that needed to upgrade its raw material handling system to meet new environmental regulations. HeadPowder's solution included a combination of positive and negative pressure conveying, along with advanced dust control equipment, which helped the plant achieve compliance while maintaining high operational performance.
Conclusion
Cement raw material powder pneumatic conveying is a vital technology in modern cement production, and the design principles behind these systems are critical to their success. Shandong HeadPowder Engineering Co., Ltd. has established itself as a leading provider of high-quality pneumatic conveying solutions, leveraging its expertise and innovative approach to meet the evolving needs of the cement industry. By focusing on efficiency, safety, and customization, HeadPowder helps cement manufacturers optimize their operations and achieve their production goals. As the demand for cement continues to grow, the importance of reliable and efficient material handling systems will only increase, making HeadPowder's solutions more valuable than ever.