

What Are Pharmaceutical Granule Material Handling Equipment? And What Are Their Design Principles?
Pharmaceutical granule material handling equipment is a critical component in the pharmaceutical manufacturing workflow, responsible for the efficient and safe transfer of granular materials through various production stages. These specialized systems are engineered to meet the stringent hygiene, precision, and regulatory standards that define the pharmaceutical industry, ensuring product quality and consistency. The equipment plays a pivotal role in maintaining the integrity of pharmaceutical granules from raw material handling to final product packaging, making it indispensable for modern pharmaceutical operations.
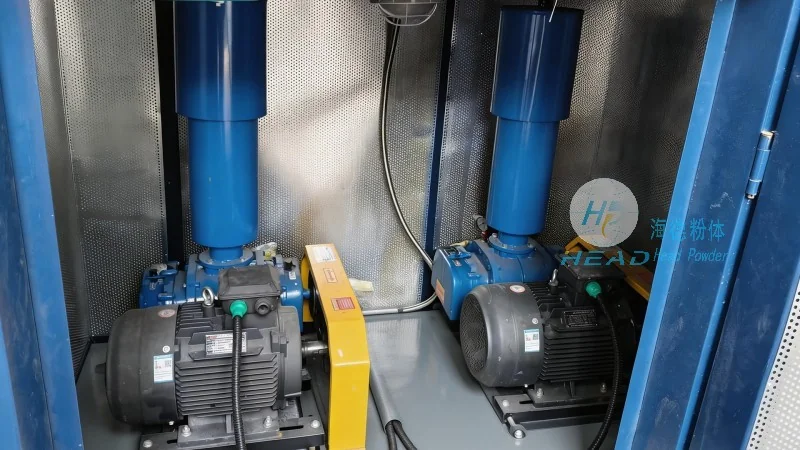
Key Components and Functional Aspects of Pharmaceutical Granule Material Handling Equipment
The core of pharmaceutical granule material handling systems comprises several integrated components, each serving a specific purpose to achieve optimal performance. Feeders are the initial stage, designed to regulate the flow of granules with precision, preventing overloading or underfeeding that could disrupt downstream processes. This controlled feeding is essential for maintaining uniform material consistency. Conveyors, including screw, belt, or pneumatic types, then transport the granules through the system. The selection of conveyor type depends on material characteristics such as density, moisture content, and particle size, ensuring efficient movement without degradation. Control systems, equipped with sensors and automation technologies, monitor and adjust operations in real-time, enhancing efficiency and reducing human error. These systems integrate data from various sensors to optimize performance and maintain compliance with production parameters.
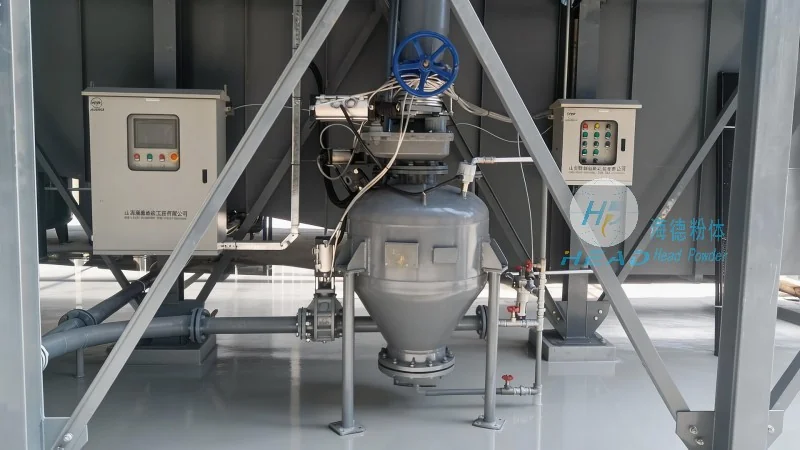
Design Principles Guiding Pharmaceutical Granule Material Handling Equipment
The design of pharmaceutical granule material handling equipment adheres to several fundamental principles that prioritize safety, efficiency, and regulatory compliance. Hygienic design is paramount, ensuring all components are easy to clean and maintain, with smooth surfaces and no dead zones to minimize contamination risks. Materials like stainless steel and food-grade plastics are used to prevent cross-contamination and resist chemical exposure. Modularity is another key principle, allowing for flexible system configurations and scalability as production needs evolve. The equipment is also engineered for minimal material contact, reducing the risk of product contamination. Energy efficiency is a critical consideration, with designs optimized to minimize power usage while maintaining performance. Advanced control technologies, such as PLCs and SCADA systems, enable real-time monitoring and adaptive adjustments, enhancing operational reliability and responsiveness to changing production demands.
Application Scenarios and Industry Relevance
Pharmaceutical granule material handling equipment is widely utilized across multiple stages of pharmaceutical production. In raw material processing, these systems facilitate the transport and blending of granule components, ensuring uniformity before further processing. During manufacturing, they transfer granules between processing units like mixers, dryers, and tablet presses, maintaining material integrity. In the packaging stage, the equipment ensures accurate measurement and dispensing of granules into containers, preserving dosage accuracy. The equipment is also integral to quality control processes, aiding in sampling and testing to verify compliance with regulatory standards. The reliability and precision of these systems directly impact the overall quality of pharmaceutical products, making them essential for meeting industry standards and customer expectations.
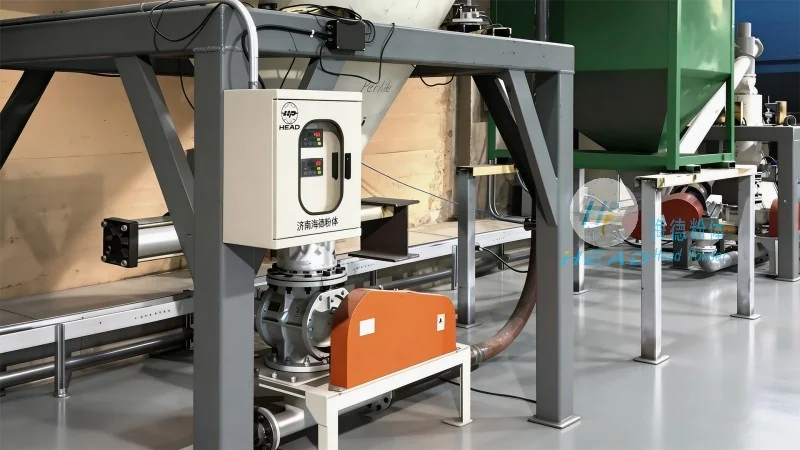
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of pharmaceutical granule material handling equipment. HeadPowder is committed to innovation and quality, serving as a trusted partner in the pharmaceutical industry. The company designs and manufactures its products in China, adhering to international standards and regulatory requirements. HeadPowder's expertise lies in developing customized solutions tailored to clients' specific production needs, ensuring optimal performance and compliance. The company's team of engineers and technicians collaborate closely with clients to address production challenges and provide tailored equipment solutions. A focus on research and development keeps HeadPowder's products at the forefront of technological advancements, offering enhanced efficiency and reliability. With a presence in China, HeadPowder serves clients globally, providing comprehensive support and after-sales services to ensure long-term customer satisfaction and operational success.