

What is Corn Starch Material Handling? And What Are the Design Principles?
Corn starch material handling is a critical aspect of industrial operations, particularly in sectors that rely on this versatile ingredient. The process involves the movement of corn starch from storage silos to processing equipment, and then to packaging or further downstream applications. Efficient handling is essential to maintain product quality, minimize waste, and ensure consistent performance. The design of corn starch handling systems must address several unique challenges, including the fine particle size of the material, which can lead to dust generation and clogging, as well as the need for hygienic and explosion-proof equipment to meet regulatory requirements.
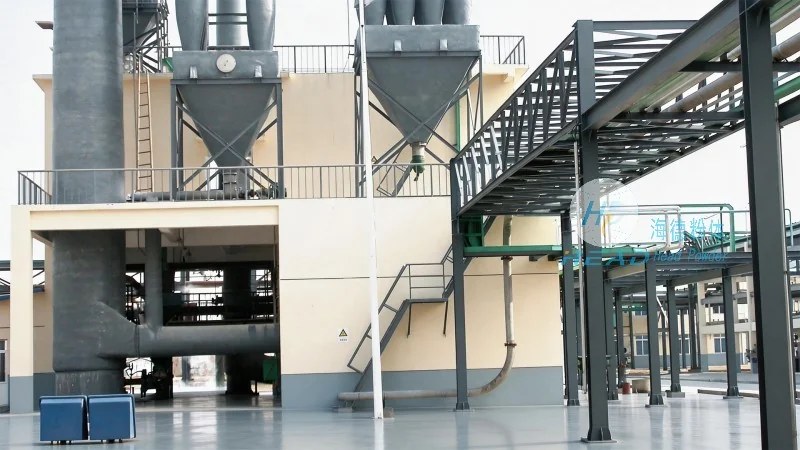
The Core Design Principles for Corn Starch Material Handling Systems
Effective corn starch material handling systems are built on a foundation of key design principles that prioritize safety, efficiency, and durability. The first principle is the implementation of robust dust control measures. Corn starch is a fine powder that can easily become airborne, posing health risks to workers and creating environmental hazards. To mitigate this, systems typically include sealed conveyor lines, aeration systems to prevent material bridging, and advanced filtration equipment such as baghouse or cartridge filters. These measures not only protect personnel but also comply with environmental regulations. The second principle is the selection of appropriate conveying equipment. Screw conveyors are commonly used for horizontal or slight incline transport due to their ability to handle fine powders without causing excessive friction or material degradation. For vertical transport, bucket elevators are preferred, as they can efficiently lift large volumes of corn starch while maintaining a controlled environment. The third principle is the design of airtight and explosion-proof systems. Given the flammable nature of corn starch dust, all components must be constructed to prevent ignition sources and ensure safe operation. This includes the use of non-sparking materials and proper grounding in electrical systems. Finally, the principle of material flow uniformity is critical to prevent clogging and ensure consistent throughput. This is achieved through the use of feeders and metering devices that regulate the flow rate, ensuring that the processing equipment receives a steady supply of material.
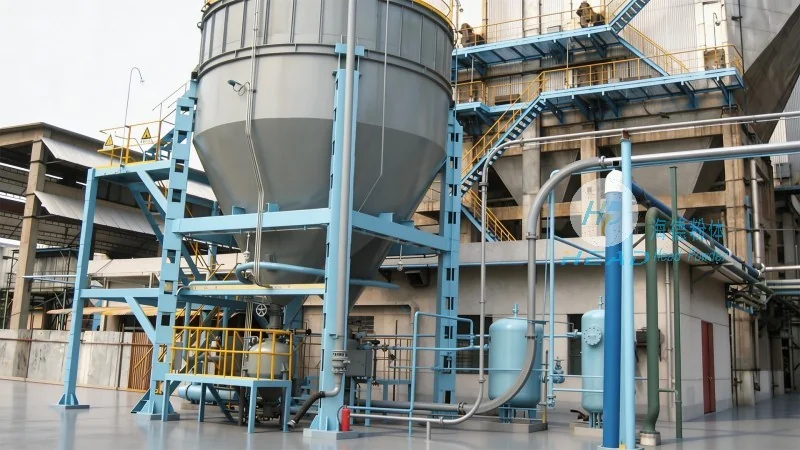
Key Components in Corn Starch Material Handling Systems
Modern corn starch material handling systems consist of several interrelated components that work together to achieve efficient and reliable operation. Storage silos are a primary component, used to store large quantities of corn starch while maintaining a controlled environment. These silos are typically made of stainless steel or other corrosion-resistant materials and are equipped with level sensors to monitor the material level. Aeration systems are often integrated into the silos to prevent material bridging and ensure smooth discharge. The discharge of corn starch from the silos is typically managed using rotary valves or slide gates, which control the flow rate and prevent dust generation. Conveying equipment, such as screw conveyors or pneumatic systems, transport the corn starch from the storage silos to the processing area. Screw conveyors are preferred for horizontal or slight incline transport due to their ability to handle fine powders without causing excessive friction or material degradation. Pneumatic systems, on the other hand, use air pressure to move the material, which is ideal for long-distance or vertical transport. The conveying equipment is often equipped with dust collection systems to capture any particles that escape, ensuring a clean and safe working environment. Additionally, feeding and metering devices, such as vibratory feeders or rotary valves, regulate the flow of corn starch into downstream processes, ensuring precise control over material input. These devices are crucial for maintaining consistent product quality and preventing overfeeding or underfeeding of the processing equipment. Finally, the system includes a dust collection system, which captures any airborne particles and returns them to the process or disposes of them safely. This system typically includes filters and a fan to create a negative pressure environment, preventing dust from escaping into the workplace.
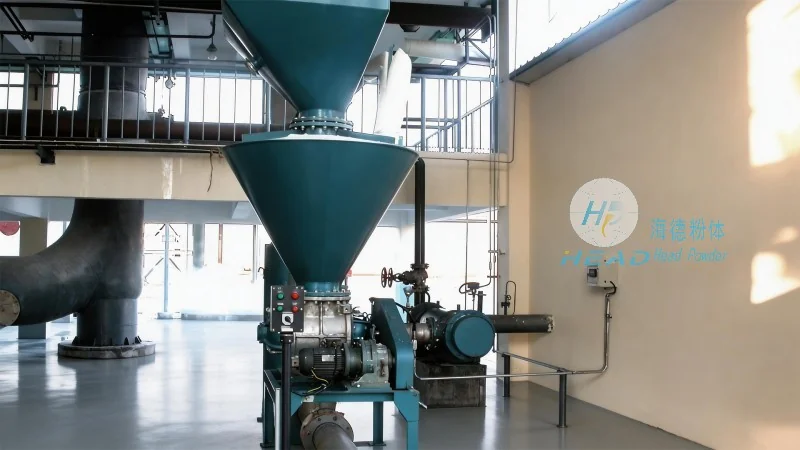
HeadPowder's Expertise in Corn Starch Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as HeadPowder, is a leading manufacturer and supplier of specialized material handling solutions for corn starch processing. With a strong focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner for businesses in the food, pharmaceutical, and chemical industries. The company’s expertise lies in designing and manufacturing custom corn starch handling systems that meet the unique needs of each client. HeadPowder’s team of experienced engineers and technicians works closely with clients to understand their specific requirements, including production capacity, material flow rates, and regulatory compliance. The company offers a range of products, including storage silos, conveyors, feeders, and dust collection systems, all designed to work together as a complete solution. HeadPowder’s systems are built to withstand the harsh conditions of corn starch processing, with materials such as stainless steel and specialized coatings used to prevent corrosion and wear. The company also provides installation and maintenance services to ensure that clients can operate their systems efficiently and safely. HeadPowder’s commitment to quality and reliability has earned it a reputation as a leading provider of corn starch material handling solutions, helping businesses improve their operational performance and reduce costs.