

What Is a Bulk Powder Storage and Conveying Line? And What Are Its Design Principles?
Bulk powder storage and conveying systems are essential industrial solutions for handling, storing, and transporting dry bulk materials. These systems are widely used across various industries, including pharmaceuticals, food processing, chemicals, and manufacturing, to ensure efficient material flow and maintain product quality. A well-designed system not only enhances operational efficiency but also minimizes the risk of material degradation, contamination, and safety hazards. In this article, we will explore the fundamental components of a bulk powder storage and conveying line and delve into the key design principles that ensure optimal performance.
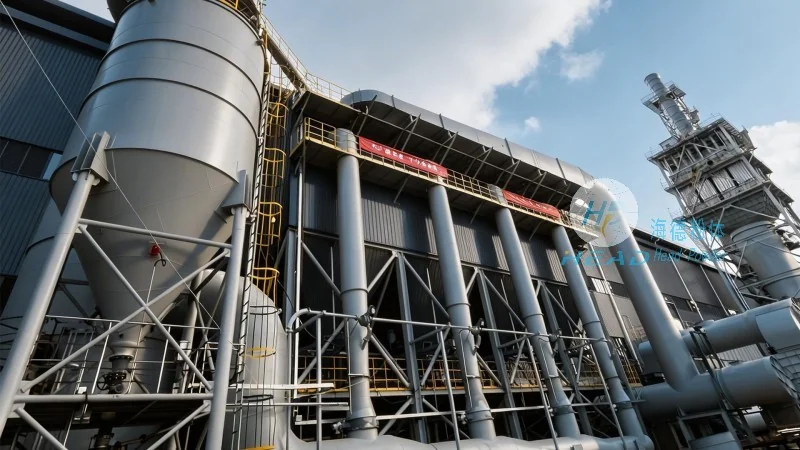
Key Components of a Bulk Powder Storage and Conveying System
The core components of a bulk powder storage and conveying line typically include bulk storage silos or hoppers, material feeders, conveying equipment (such as pneumatic or mechanical conveyors), and control systems. Each component plays a critical role in the overall functionality of the system. The storage silos are designed to hold large quantities of powder, often with features like a conical bottom to facilitate discharge. Material feeders, such as rotary valves or star feeders, regulate the flow of material from the silo to the conveyor. The conveying equipment then transports the powder to the processing or packaging areas. Control systems, including sensors and automation, monitor and adjust the flow rates to maintain consistent performance.
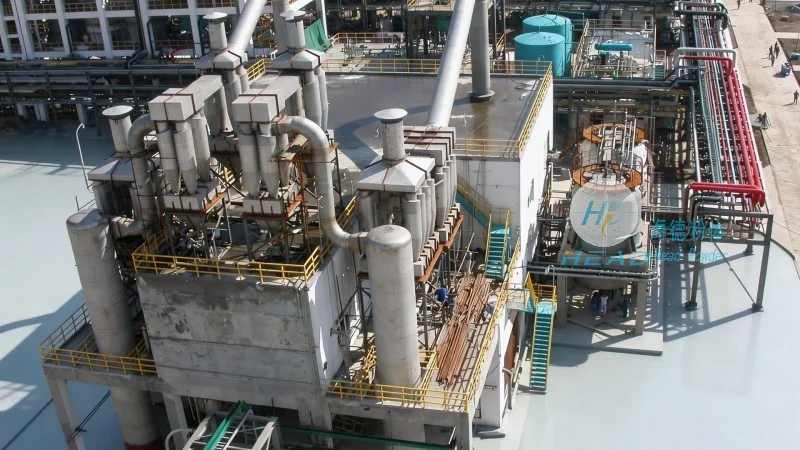
Design Principles for Optimal Performance
The design of a bulk powder storage and conveying line is governed by several critical principles to ensure reliability, efficiency, and safety. First, the system must be tailored to the specific properties of the powder being handled, such as particle size, moisture content, and flowability. This involves selecting appropriate equipment, like the type of hopper and feeder, to prevent issues like bridging or caking. Second, the system should minimize material degradation and contamination. This is achieved through proper sealing, cleaning protocols, and the use of materials that are compatible with the powder. Third, the design must consider the overall flow path and energy efficiency. For example, pneumatic conveying systems may be preferred for long-distance transport due to their ability to handle fine powders without the need for mechanical components that could cause wear and tear. Finally, safety is a paramount consideration. The system should include features like explosion-proof designs, dust collection systems, and emergency shutdown capabilities to protect personnel and equipment.
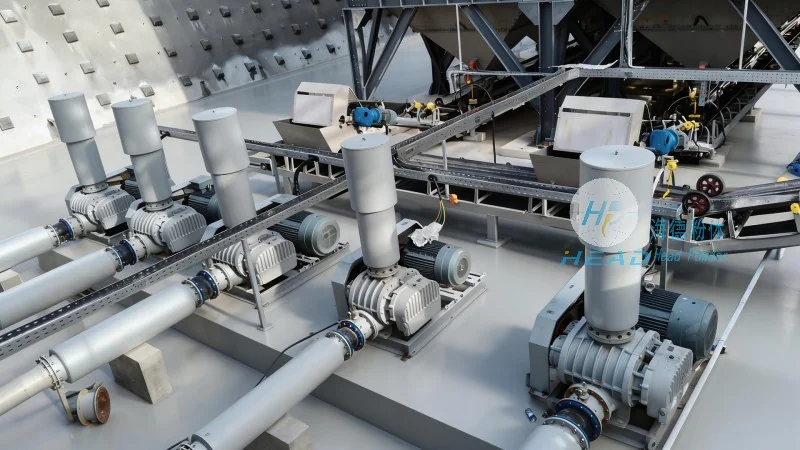
Applications and Industries
Bulk powder storage and conveying lines are versatile and find applications in numerous industries. In the pharmaceutical industry, these systems are used to handle active pharmaceutical ingredients (APIs) and excipients, ensuring precise dosing and preventing cross-contamination. In the food industry, they are employed for processing and packaging dry foods like cereals, snacks, and powders. The chemical industry utilizes these systems for handling raw materials and intermediates, while manufacturing industries rely on them for transporting bulk raw materials to production lines. The adaptability of these systems makes them indispensable in modern industrial operations.
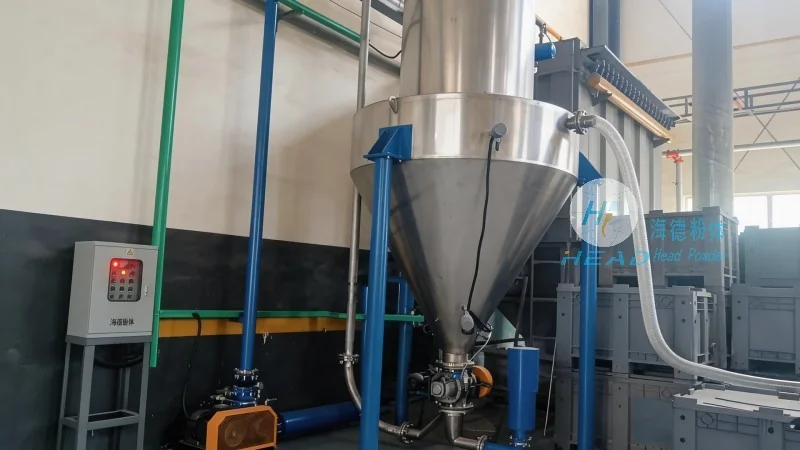
Conclusion
Bulk powder storage and conveying lines are sophisticated industrial systems that combine storage, feeding, and conveying technologies to meet the demands of various industries. The design principles, including material-specific considerations, efficiency, safety, and adaptability, are crucial for ensuring the system operates reliably and effectively. As industries continue to evolve, the importance of well-designed bulk powder handling systems will only grow, making them a vital component of modern manufacturing and processing operations. For those seeking reliable solutions, companies like Shandong HeadPowder Engineering Co., Ltd. specialize in designing and manufacturing customized bulk powder storage and conveying systems to meet the unique needs of their clients.