

What is a Metering Bin Pump Pneumatic Conveying System? And What Are Its Design Principles?
A metering bin pump, also known as a pneumatic conveying system with a bin pump, is a specialized industrial equipment designed for the precise and efficient handling of bulk materials. This system combines the functions of a storage bin, a pump, and a conveying line to transport powders and granules over long distances with high accuracy. The core of the system is the bin pump, which uses compressed air to create a pressure differential that moves material from the storage bin through the pipeline to the destination point. The metering function ensures that the material flow rate is controlled precisely, making it ideal for applications requiring consistent feed rates, such as in chemical processing, food production, and pharmaceutical manufacturing.
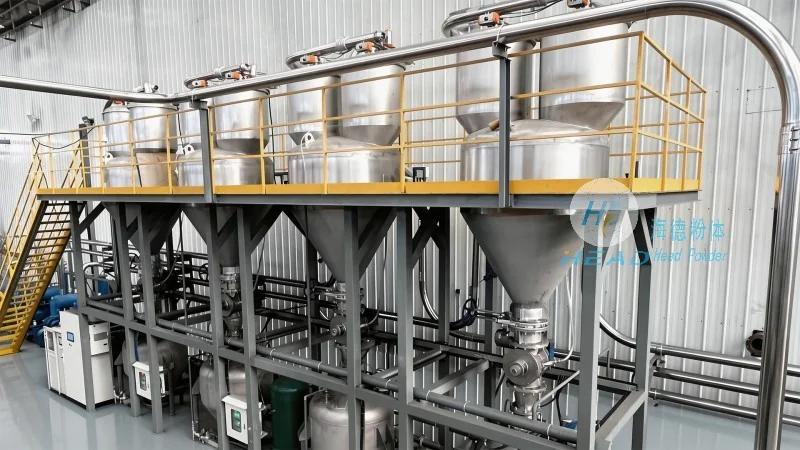
Key Components of a Metering Bin Pump System
The metering bin pump system typically consists of several key components that work together to achieve efficient material handling. The primary components include a storage bin, a bin pump unit, a conveying pipeline, and a control system. The storage bin is used to hold the bulk material, providing a large capacity for continuous operation. The bin pump unit is the heart of the system, responsible for creating the pressure differential needed to move the material. It often includes a hopper, a plunger or diaphragm mechanism, and an air compressor that supplies the compressed air. The conveying pipeline connects the bin pump to the discharge point, and its design (e.g., straight or curved) affects the system's performance and pressure requirements. The control system monitors and adjusts the air pressure, material flow rate, and other parameters to ensure stable operation and prevent issues like blockages or overpressurization.
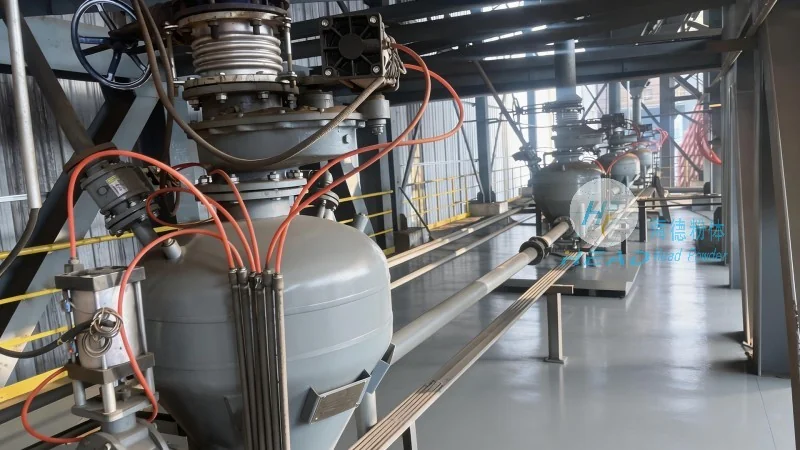
Design Principles and Operational Mechanism
The design of a metering bin pump system is based on several fundamental principles to ensure reliability and efficiency. The most critical principle is the creation of a pressure differential between the storage bin and the discharge point. The bin pump draws material from the bin into its chamber, then seals the chamber and increases the internal pressure using compressed air. This pressure forces the material through the pipeline to the outlet. The metering function is achieved by controlling the timing and duration of the pressure pulses or the stroke of the pump plunger. This allows for precise control of the material flow rate, which is essential for processes that require consistent feed rates. Another key design principle is the prevention of material degradation and contamination. The system is often designed with materials that are resistant to corrosion and wear, and the conveying process is kept at low velocity to minimize particle breakage and dust generation. Additionally, the system includes features like air filtration and moisture control to maintain the quality of the conveyed material.

Applications and Advantages of Metering Bin Pump Systems
Metering bin pump systems are widely used in various industries due to their versatility and efficiency. They are particularly suitable for applications where traditional conveying methods like belt conveyors or screw conveyors are not practical. For example, in the chemical industry, these systems are used to transport powders like pigments, polymers, and catalysts, which are often abrasive and require precise dosing. In the food and pharmaceutical industries, the systems are used to handle sensitive materials like flour, sugar, and active pharmaceutical ingredients (APIs), where contamination and particle size control are critical. The advantages of metering bin pump systems include high accuracy in material flow control, the ability to handle a wide range of materials (from fine powders to coarse granules), long-distance conveying capabilities, and the flexibility to integrate with existing production lines. Additionally, the system can be easily scaled up or down to meet changing production demands, making it a cost-effective solution for many industrial applications.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of metering bin pump pneumatic conveying systems. The company is based in Shandong, China, and has a strong reputation for providing high-quality, reliable equipment tailored to the needs of various industries. HeadPowder's products are designed with advanced technology and rigorous quality control to ensure long service life and minimal maintenance. The company offers a range of solutions, from standard systems to customized designs, to meet the specific requirements of clients. With a focus on innovation and customer satisfaction, HeadPowder has become a trusted partner for many businesses seeking efficient and accurate material handling solutions.