

The Role of Pneumatic Conveying in the Transport of Sodium Stearate
For industries dealing with bulk materials like sodium stearate, efficient and reliable material handling is crucial. Pneumatic conveying emerges as a key technology that addresses the unique challenges associated with transporting such substances. This article explores how pneumatic conveying systems, particularly in the context of sodium stearate transport, enhance operational efficiency, maintain material integrity, and ensure safety in industrial processes.
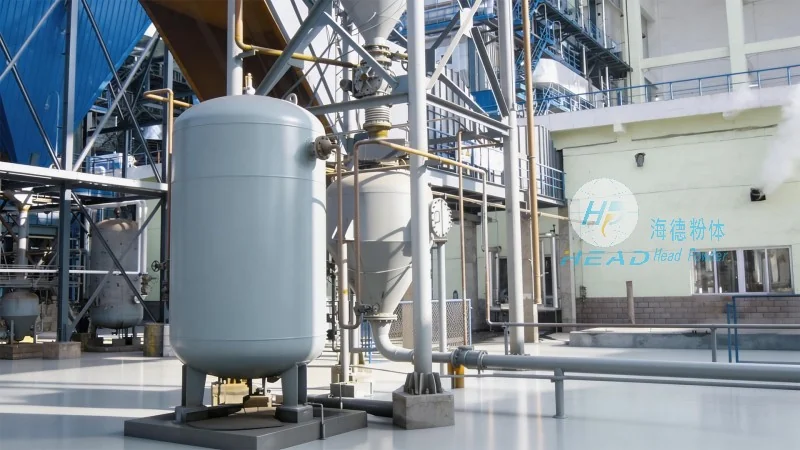
Sodium stearate, a widely used surfactant and emulsifier, is often handled in bulk quantities. Its properties, such as hygroscopic nature and sensitivity to moisture, require specialized handling methods to prevent degradation or clumping. Traditional methods like belt conveyors or bucket elevators may not be suitable due to the risk of material degradation or contamination. Pneumatic conveying offers a solution by using air to transport the material in a closed system, minimizing exposure to external factors and preserving the material's quality.
HeadPowder, a leading provider of engineering solutions, specializes in designing and implementing pneumatic conveying systems tailored to the needs of various industries. With a focus on innovation and customer satisfaction, the company has developed advanced systems that optimize the transport of sodium stearate while adhering to strict quality and safety standards. The company's expertise lies in understanding the material's characteristics and tailoring the conveying system to ensure smooth, efficient, and safe operation.
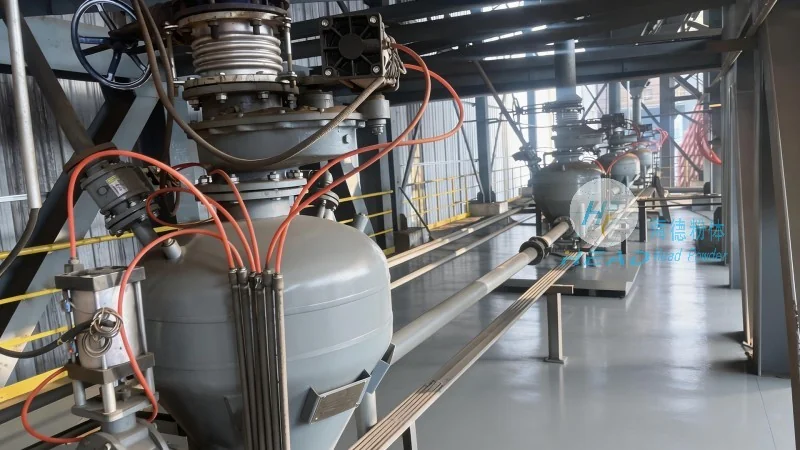
One of the primary advantages of pneumatic conveying in sodium stearate transport is its ability to handle fine powders and prevent agglomeration. The system uses air pressure to move the material through pipelines, reducing the risk of blockages and ensuring consistent flow rates. This is particularly important for sodium stearate, which can easily form lumps if not handled correctly. By maintaining a controlled environment and using appropriate air velocities, the conveying system ensures that the material remains in a free-flowing state throughout the process.
Furthermore, pneumatic conveying systems offer flexibility in material handling. They can be integrated with other processing equipment, such as mixers, reactors, or storage tanks, allowing for seamless material transfer from one stage to another. This integration enhances overall plant efficiency and reduces downtime. HeadPowder's engineers work closely with clients to design custom conveying solutions that fit their specific production requirements, ensuring that the system is optimized for both performance and cost-effectiveness.
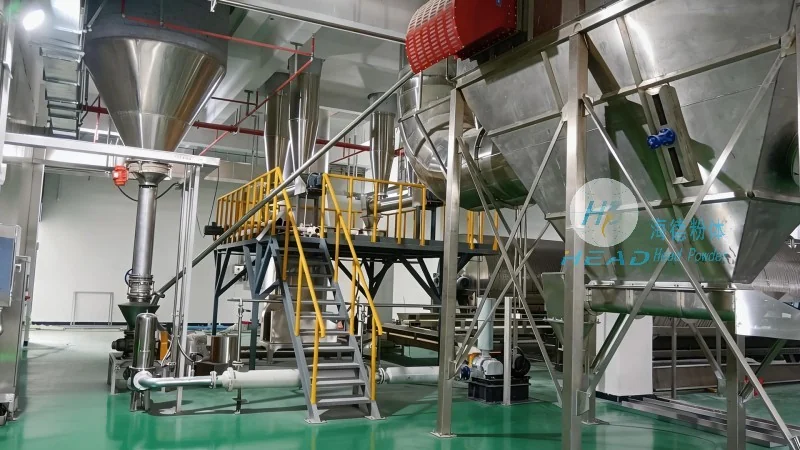
Another critical aspect of pneumatic conveying is its impact on operational safety. By transporting materials in a closed system, the risk of dust exposure and environmental contamination is significantly reduced. This is especially important for sodium stearate, which can be a respiratory irritant if inhaled in large quantities. The enclosed system also helps in maintaining a clean and controlled environment, which is essential for maintaining product quality and compliance with regulatory standards.
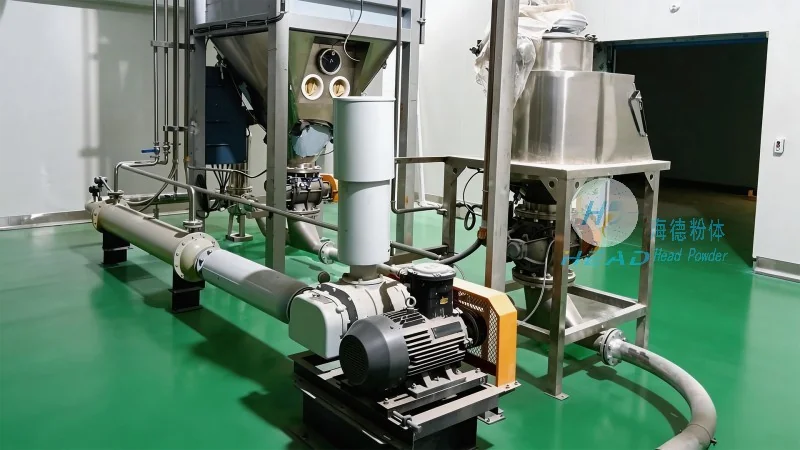
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, has built a strong reputation for delivering high-quality engineering solutions. The company's commitment to excellence is reflected in its state-of-the-art facilities and experienced team of engineers. By leveraging advanced technology and industry expertise, HeadPowder provides tailored pneumatic conveying systems that meet the unique needs of its clients. The company's focus on customer satisfaction and long-term partnerships has made it a trusted name in the industry.
In conclusion, pneumatic conveying plays a vital role in the efficient and safe transport of sodium stearate. By leveraging the advantages of this technology, industries can improve their operational efficiency, maintain product quality, and ensure compliance with safety and environmental regulations. HeadPowder's expertise in designing and implementing such systems makes it an ideal partner for businesses seeking to optimize their material handling processes. With a focus on innovation and customer-centric solutions, HeadPowder continues to lead the way in providing reliable and efficient pneumatic conveying solutions for sodium stearate and other bulk materials.