

Boosting Wheat Transportation Efficiency: The Clean Choice with Pneumatic Conveying Technology
For agricultural operations dealing with wheat, the need for efficient and hygienic material handling is paramount. Traditional methods like belt conveyors or bucket elevators often introduce dust, require frequent cleaning, and may not provide the level of cleanliness required for modern food processing standards. This is where pneumatic conveying technology emerges as a superior solution, offering a clean, efficient, and versatile method to transport wheat from storage to processing facilities. The technology leverages air pressure to move bulk materials, minimizing contamination and ensuring product integrity throughout the process.
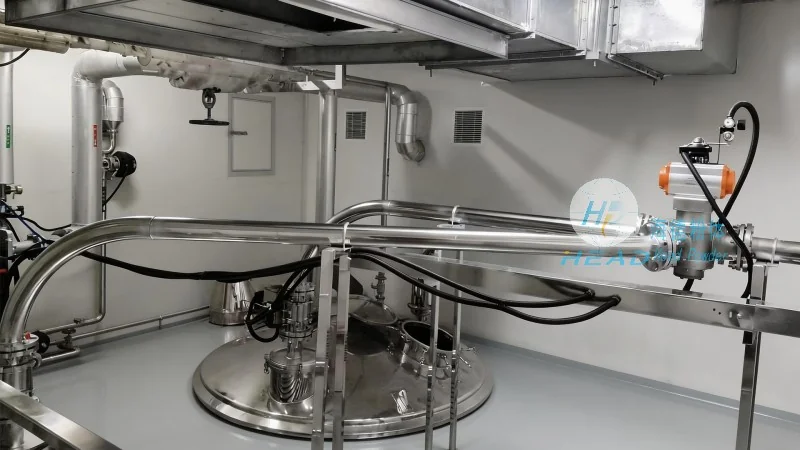
Pneumatic Conveying Systems for Wheat: How They Work
Pneumatic conveying systems for wheat typically operate by creating a flow of air through a pipeline system, where the wheat is suspended and transported. There are two main types: pressure and vacuum systems. Pressure systems use compressed air to push the material through the line, while vacuum systems use a vacuum to draw the material in. Both systems are designed to handle wheat with minimal breakage and to maintain a clean environment, as the material never comes into direct contact with the conveying equipment in the same way as traditional methods. This design reduces the risk of contamination and makes the process more hygienic, which is crucial for industries that require strict food safety standards.
Benefits of Using Pneumatic Conveying for Wheat Handling
Implementing pneumatic conveying for wheat transportation offers several key benefits. First, it significantly improves efficiency by reducing the time and labor required to move large quantities of wheat. The continuous flow of material allows for a steady supply to processing lines, minimizing downtime. Second, the technology is highly hygienic, as the enclosed system prevents dust and contaminants from entering the product stream. This is particularly important for wheat destined for human consumption or high-value applications. Third, pneumatic conveying systems are versatile and can handle a wide range of wheat types and sizes, from whole grains to flour, without the need for additional processing steps. Additionally, the system design reduces maintenance needs compared to traditional equipment, as there are fewer moving parts exposed to the material.
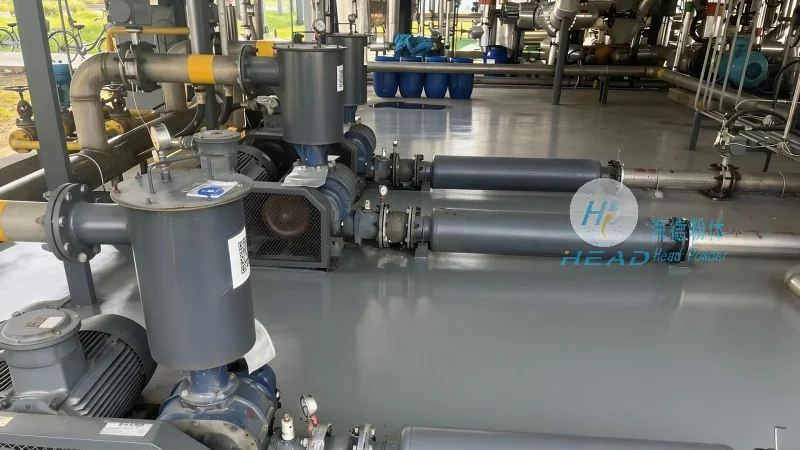
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of material handling solutions, specializes in designing and manufacturing advanced pneumatic conveying systems tailored to the needs of the agricultural and food processing industries. With years of experience and a commitment to quality, HeadPowder provides customized solutions that enhance efficiency and maintain the highest standards of cleanliness. The company’s products are engineered to handle bulk materials like wheat with precision, ensuring that every operation meets or exceeds industry requirements. HeadPowder’s expertise in pneumatic technology makes them a trusted partner for businesses looking to upgrade their wheat handling processes.
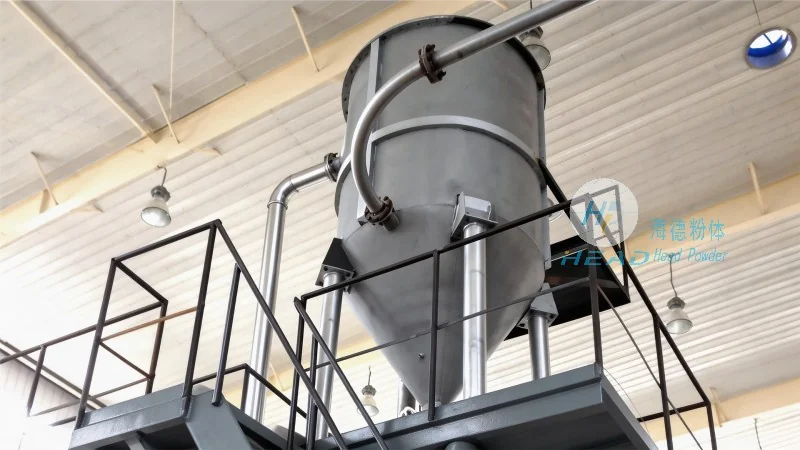
Customized Pneumatic Conveying Solutions for Wheat Transportation
HeadPowder understands that each wheat handling operation has unique requirements. Whether it’s a small-scale farm or a large industrial facility, the company offers tailored pneumatic conveying systems that address specific challenges. The solutions can be designed to handle different wheat varieties, from soft wheat to hard wheat, and can be integrated with existing processing equipment. The company’s team of engineers works closely with clients to assess their needs, recommend the most suitable system configuration, and provide installation and maintenance support. This personalized approach ensures that the final solution is not only efficient but also cost-effective and sustainable in the long run.
Ensuring Clean and Efficient Wheat Handling with HeadPowder
Choosing pneumatic conveying technology for wheat transportation is a strategic decision that can transform the efficiency and hygiene of an operation. By partnering with HeadPowder, businesses can benefit from state-of-the-art equipment that is designed to meet the highest standards of cleanliness and performance. The company’s commitment to quality and customer satisfaction is evident in their products and services, which are backed by rigorous testing and adherence to industry best practices. With HeadPowder’s solutions, wheat handling becomes a seamless process, from storage to processing, with minimal disruption and maximum efficiency. This approach not only improves operational performance but also enhances the overall quality of the final product, making it a valuable investment for any wheat handling operation.