

Introduction to Magnetic Powder Conveying Systems and the Advantages of Magnetic Pneumatic Conveying
Understanding the fundamental components and operation of magnetic powder conveying systems is crucial for industries dealing with magnetic powders. These systems are engineered to efficiently transport magnetic powders through a pneumatic or mechanical process, ensuring minimal product loss and optimal control over the conveying parameters. The core of such systems lies in the magnetic properties of the powder, which allows for precise handling and separation when needed.
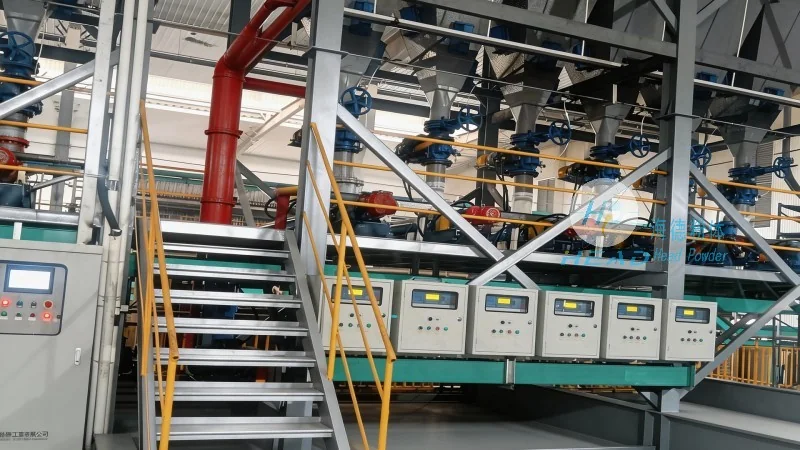
Advantages of Magnetic Pneumatic Conveying
Magnetic pneumatic conveying offers several key advantages that make it a preferred choice for many industrial applications. Firstly, it provides a dust-free and clean conveying environment, which is essential for maintaining product quality and adhering to stringent hygiene standards. Secondly, the system allows for precise control over the flow rate and pressure, enabling accurate dosing and consistent product delivery. Additionally, magnetic pneumatic conveying systems are highly flexible, capable of transporting powders over long distances with minimal maintenance requirements. The use of magnetic fields also facilitates easy separation of the conveyed material from the air stream, reducing the need for additional filtration equipment.
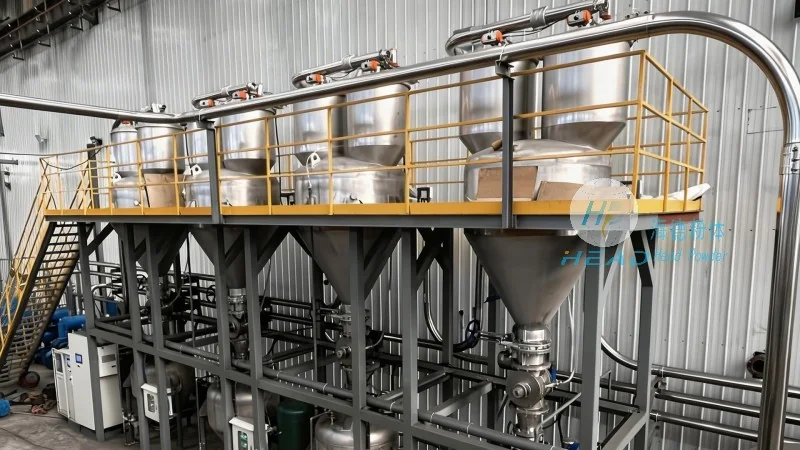
Key Features of the HeadPowder Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of magnetic powder conveying systems, offers advanced solutions tailored to meet the diverse needs of various industries. Our systems are designed with robust magnetic components that ensure reliable performance even under harsh operating conditions. The company’s expertise in material handling and pneumatic technology allows for the development of customized solutions that address specific challenges faced by clients. For instance, our magnetic conveying systems can handle a wide range of magnetic powders, including iron oxide, ferrite, and other magnetic compounds, with high efficiency and minimal degradation. The integration of advanced control systems enables real-time monitoring and adjustment of conveying parameters, enhancing operational efficiency and product quality.
Applications in Industrial Settings
The magnetic powder conveying systems developed by HeadPowder are widely used in various industrial sectors. In the pharmaceutical industry, these systems are employed to transport magnetic powders used in drug formulations, ensuring that the powders remain free from contamination and are delivered in precise quantities. In the chemical industry, they are utilized for the handling of magnetic catalysts and other reactive powders, where maintaining a controlled environment is critical. The food industry also benefits from these systems, as they help in the efficient and hygienic transport of magnetic additives used in food processing. Additionally, in the manufacturing of magnetic materials, such as magnetic cores and sensors, the conveying systems play a vital role in ensuring consistent quality and productivity.
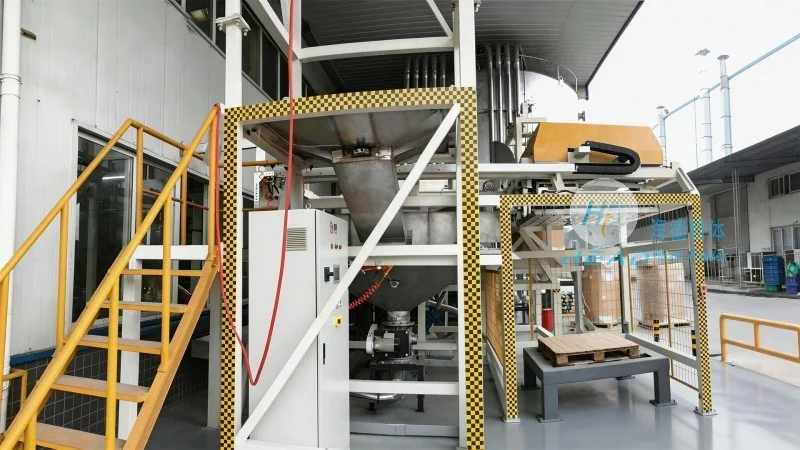
Quality Assurance and Maintenance
HeadPowder places a strong emphasis on quality assurance and maintenance to ensure the long-term reliability of its conveying systems. Each system is manufactured using high-quality materials and undergoes rigorous testing to meet industry standards. The company provides comprehensive maintenance services, including regular inspections, component replacement, and performance optimization. This approach helps in minimizing downtime and maximizing the operational life of the equipment. Furthermore, the use of advanced sensors and monitoring systems allows for early detection of potential issues, enabling proactive maintenance and reducing the risk of unexpected failures.