

[Cocoa Powder Pneumatic Conveying System Analysis]
For industries dealing with cocoa powder, efficient and reliable material handling is crucial to maintaining product quality and operational efficiency. The pneumatic conveying system has emerged as a preferred solution for transporting cocoa powder due to its ability to handle fine powders without the need for mechanical components that could cause contamination or degradation. HeadPowder, a leading provider of engineering solutions, specializes in designing and manufacturing high-quality pneumatic conveying systems tailored to the needs of the cocoa processing industry. With years of experience and a deep understanding of the challenges faced by manufacturers, HeadPowder has developed systems that ensure optimal performance and product integrity.
Understanding the Core Components of a Cocoa Powder Pneumatic Conveying System
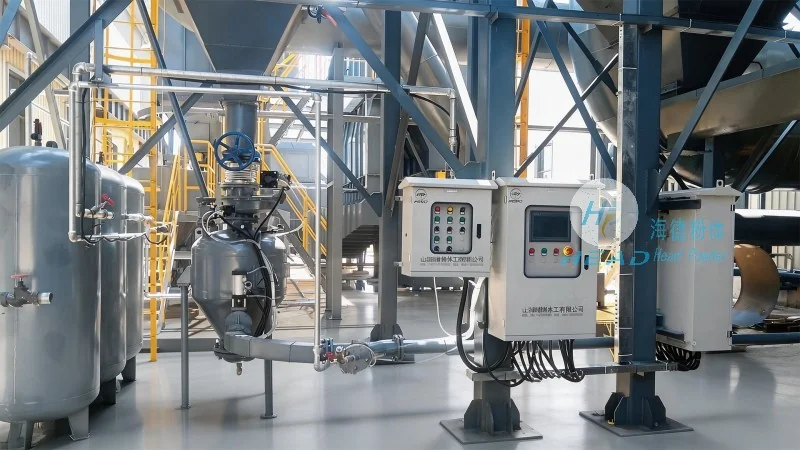
The effectiveness of a cocoa powder pneumatic conveying system largely depends on its well-designed components. The system typically consists of a hopper for material storage, a conveyor line that transports the powder, and a dust collector to ensure environmental compliance. The hopper is equipped with a feeder that controls the flow of cocoa powder into the system, preventing overfilling and maintaining consistent pressure. The conveyor line may use positive or negative pressure depending on the specific requirements of the application, with positive pressure systems being common for short-distance transport and negative pressure systems for longer distances or where dust control is critical.
How the Pneumatic Conveying Process Works for Cocoa Powder
The operation of a cocoa powder pneumatic conveying system involves the use of air to move the powder through a pipeline. In a positive pressure system, a blower or compressor generates high-pressure air that pushes the cocoa powder from the hopper into the conveying line. The air and powder mixture travels through the pipeline to the destination, such as a silo or processing unit. The system is designed to maintain a consistent flow rate, ensuring that the powder reaches its destination without clogging or loss of material. The air velocity is carefully controlled to prevent particle separation and ensure the powder remains suspended in the air stream.
Key Features and Advantages of the System
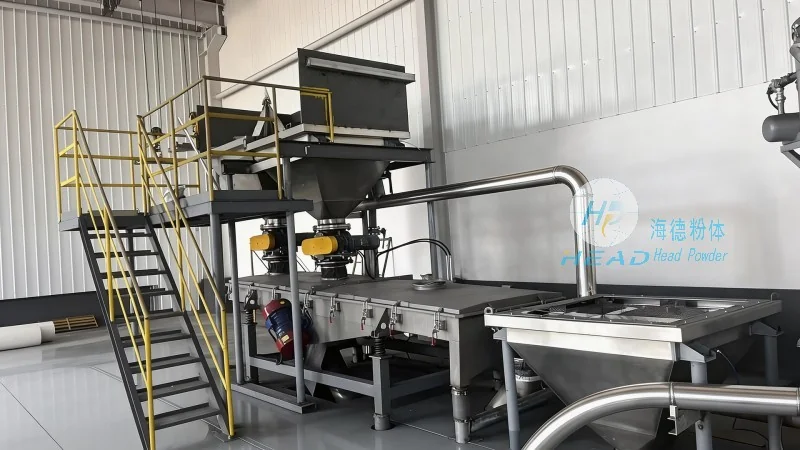
One of the primary advantages of the cocoa powder pneumatic conveying system is its ability to handle fine, abrasive materials like cocoa powder without causing damage or contamination. Unlike mechanical conveyors, which may use belts or screws that can break down the powder or introduce foreign particles, the pneumatic system uses air as the medium, preserving the integrity of the product. Additionally, the system offers flexibility in terms of layout, allowing for vertical, horizontal, or inclined transport paths, which is beneficial for facilities with limited space or complex layouts. The system also provides better dust control compared to other methods, as the enclosed pipeline prevents dust from escaping into the environment, reducing health risks for workers and maintaining compliance with environmental regulations.
Applications in the Cocoa Processing Industry
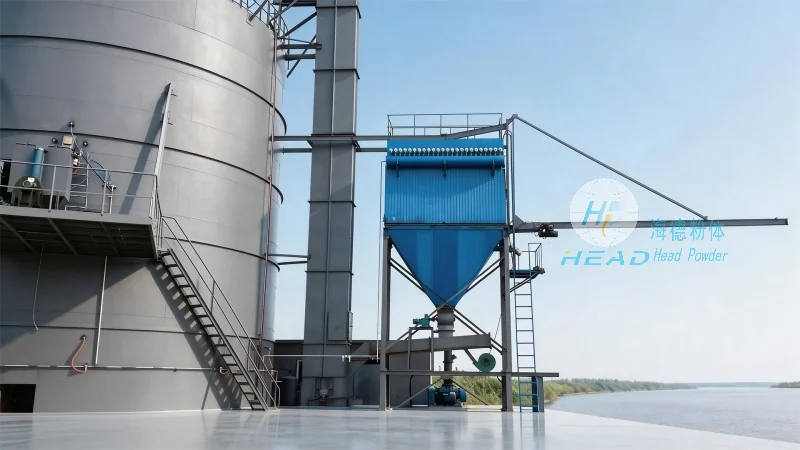
The cocoa powder pneumatic conveying system is widely used in various stages of cocoa processing, from raw material handling to finished product storage. In the initial stages, the system can transport cocoa beans or nibs from storage to grinding equipment. As the material is processed into cocoa liquor and then into powder, the pneumatic system efficiently moves the powder from the grinding mills to the packaging or storage areas. This ensures a smooth workflow and minimizes downtime, which is critical for maintaining production schedules. The system is also used in quality control processes, where samples of cocoa powder are taken and transported to testing laboratories for analysis.
Maintenance and Operational Considerations
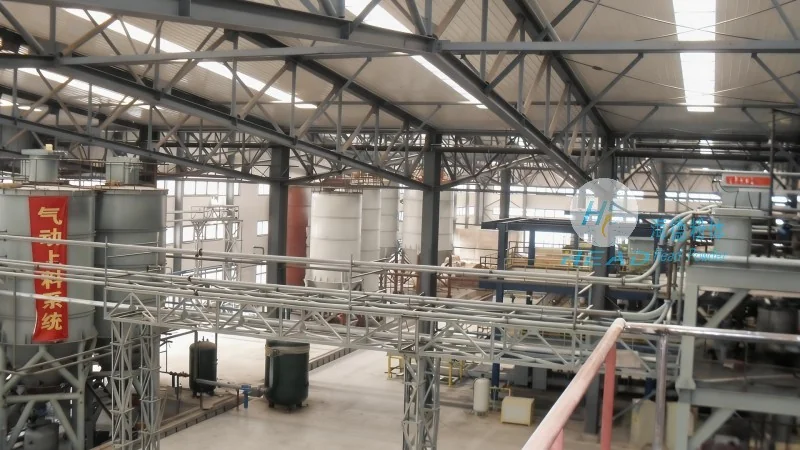
To ensure the longevity and efficiency of the cocoa powder pneumatic conveying system, regular maintenance is essential. The hopper and feeder need to be cleaned regularly to prevent clogging and ensure consistent material flow. The conveyor line and air filters should be inspected periodically to check for blockages or wear. The system's air pressure and flow rate should be monitored to maintain optimal performance. Additionally, the dust collector should be cleaned regularly to prevent dust buildup, which can affect the system's efficiency and compliance with environmental standards. Proper training for operators is also crucial to ensure they understand the system's operation and can respond to any issues that may arise.
Conclusion
The cocoa powder pneumatic conveying system is a highly effective solution for transporting fine powders in the cocoa processing industry. Its ability to handle the delicate nature of cocoa powder while maintaining product quality and operational efficiency makes it a preferred choice for many manufacturers. HeadPowder, with its headquarters in Shandong, China, provides comprehensive support and tailored solutions to meet the unique needs of each client. By investing in a well-designed pneumatic conveying system, cocoa processing facilities can enhance their operational efficiency, reduce maintenance costs, and ensure the consistent quality of their products.