

[AIRBORNE CONVEYING OF PHENOLIC POWDER: EFFICIENT AIR FLOW FOR BULK POWDER TRANSPORT]
Phenolic powder, a widely used material in various industrial applications, often requires reliable and efficient handling methods to ensure smooth production processes. Traditional methods like manual handling or mechanical conveyors may pose challenges such as dust exposure, material degradation, and operational inefficiencies. This is where pneumatic conveying systems, particularly those designed for phenolic powders, offer a superior solution. HeadPowder, a leading provider of material handling solutions, specializes in developing and implementing advanced pneumatic conveying systems tailored to the unique characteristics of phenolic powders.
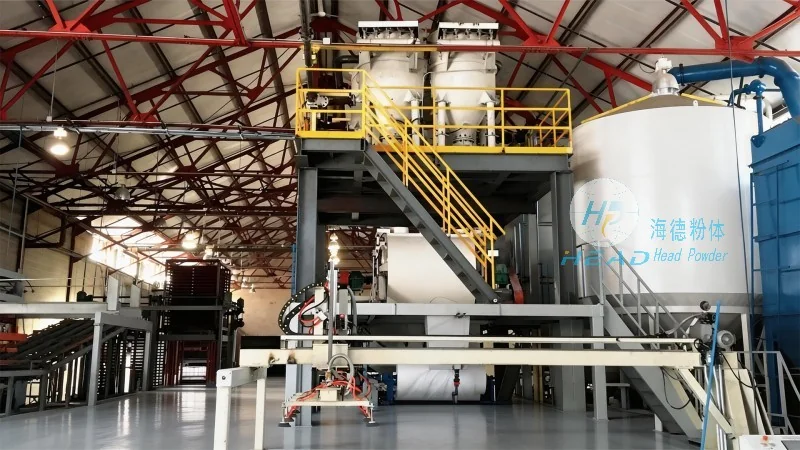
Understanding Phenolic Powder and Its Handling Challenges
Phenolic powder, also known as phenolic resin powder, is a type of thermosetting plastic powder commonly used in applications like adhesives, coatings, and molded parts. Its properties, including high density, hygroscopic nature, and potential for caking, make it challenging to handle using conventional methods. Traditional handling approaches may lead to issues like dust inhalation, material agglomeration, and increased maintenance costs. Pneumatic conveying systems address these challenges by utilizing air flow to transport the powder in a controlled and safe manner.
HeadPowder's Pneumatic Conveying Solutions for Phenolic Powders
HeadPowder, with its headquarters in Shandong, China, has established itself as a trusted name in the material handling industry. The company's expertise lies in designing customized pneumatic conveying systems that meet the specific needs of phenolic powder applications. Their solutions are engineered to handle the unique properties of phenolic powders, ensuring efficient transport while maintaining product integrity. The systems are equipped with features such as positive pressure or negative pressure operation, depending on the application requirements, and are designed to minimize dust generation and material degradation.
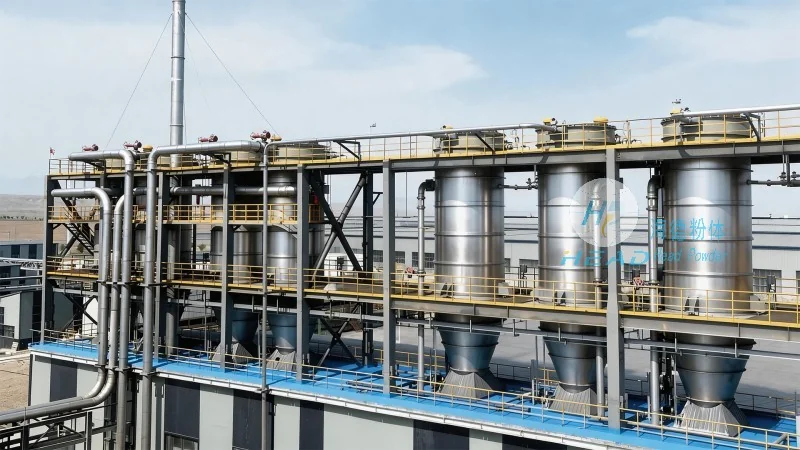
Key Features and Advantages of Pneumatic Conveying Systems
HeadPowder's pneumatic conveying systems for phenolic powders offer several key advantages. Firstly, they provide a dust-free environment, reducing health hazards and improving workplace safety. Secondly, the systems are highly efficient, allowing for continuous and automated material transport, which enhances production throughput. Thirdly, the technology minimizes material loss and degradation, preserving the quality of the phenolic powder. Additionally, the systems are easy to integrate into existing production lines and can be customized to fit various space constraints and operational needs.
Customization and Application Flexibility
HeadPowder understands that each industrial application has unique requirements. Therefore, their pneumatic conveying solutions are highly customizable. The company works closely with clients to understand their specific needs, such as the volume of powder to be transported, the distance of transport, and the desired speed of operation. Based on these requirements, they design and install systems that are optimized for performance and reliability. Whether it's a short-distance transport within a factory or a long-distance transfer between facilities, HeadPowder's systems can be tailored to meet the exact specifications.
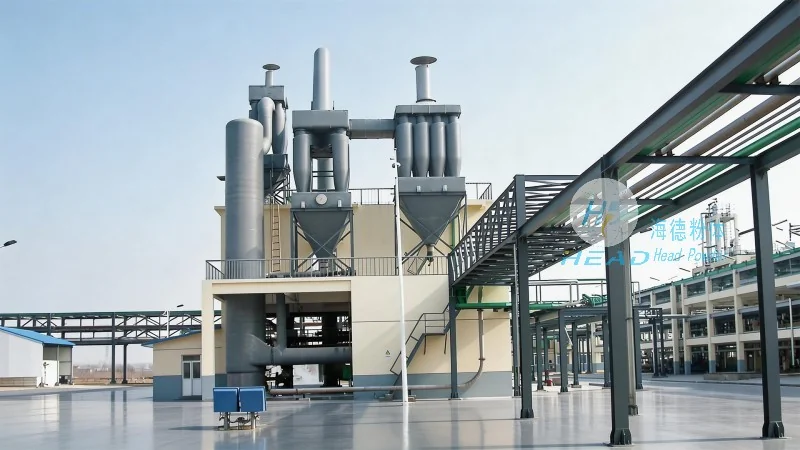
Ensuring Reliability and Durability
Reliability is a top priority for HeadPowder when developing pneumatic conveying systems. The company uses high-quality materials and components that are resistant to the corrosive and abrasive nature of phenolic powders. The systems are designed to withstand the rigors of continuous operation, ensuring long-term performance and minimal downtime. Regular maintenance and support services are also provided to ensure the systems operate at peak efficiency throughout their service life.
Conclusion: Efficient and Safe Handling of Phenolic Powders
For industries dealing with phenolic powders, pneumatic conveying systems from HeadPowder offer a reliable and efficient solution. By leveraging advanced technology and customization, these systems ensure the safe and effective transport of bulk powders, improving overall operational efficiency and product quality. With a strong presence in Shandong, China, HeadPowder continues to provide innovative material handling solutions that meet the evolving needs of industrial applications.