

Introduction to Cocoa Powder Conveying Systems: Structure and Working Principles
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer specializing in the design, development, and production of advanced powder conveying systems. With a focus on precision and efficiency, the company serves industries that require reliable and high-performance solutions for handling cocoa powder and other fine powders.
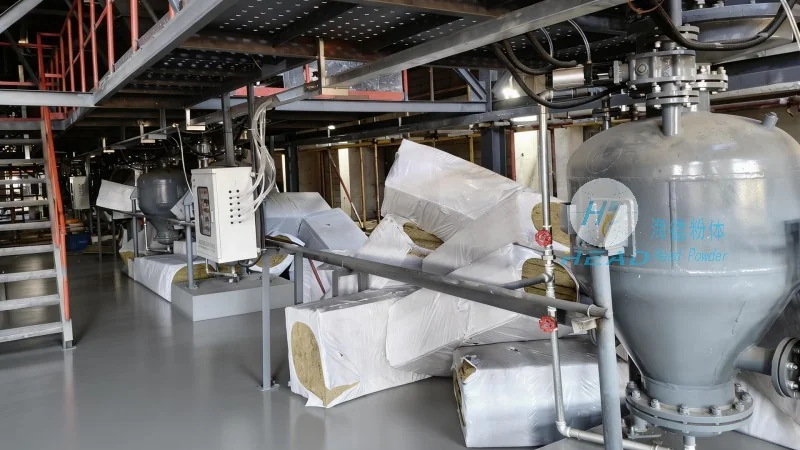
Overview of the Cocoa Powder Conveying System
The cocoa powder conveying system is engineered to address the unique challenges of transporting fine, cohesive, and potentially hygroscopic materials like cocoa powder. This system combines advanced mechanical design with intelligent control mechanisms to ensure smooth, dust-free, and efficient material handling. It is tailored to meet the demands of food processing, pharmaceutical, and chemical industries where product purity and operational safety are paramount.
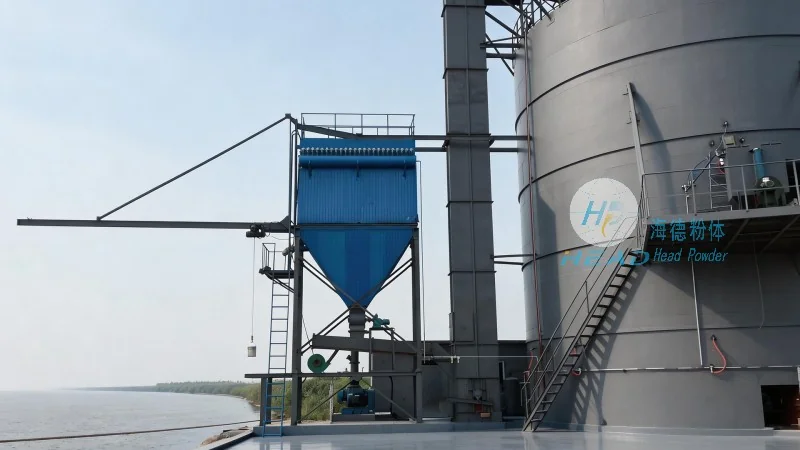
System Structure and Working Principles
The system typically consists of several key components that work in concert to achieve effective powder conveyance. The primary components include a feeding hopper, a screw conveyor or pneumatic duct, a control panel, and a discharge outlet. The feeding hopper is designed with a sloped bottom to facilitate uniform material flow and prevent clogging. The screw conveyor, made from high-quality stainless steel, features a helical screw that rotates to push the powder forward. This design minimizes friction and reduces the risk of material degradation. The pneumatic duct, when used, employs compressed air to create a pressure differential that draws the powder through the system. The control panel integrates sensors and a programmable logic controller (PLC) to monitor and adjust the conveying speed, pressure, and flow rate in real-time. This ensures consistent performance and adaptability to varying production needs.
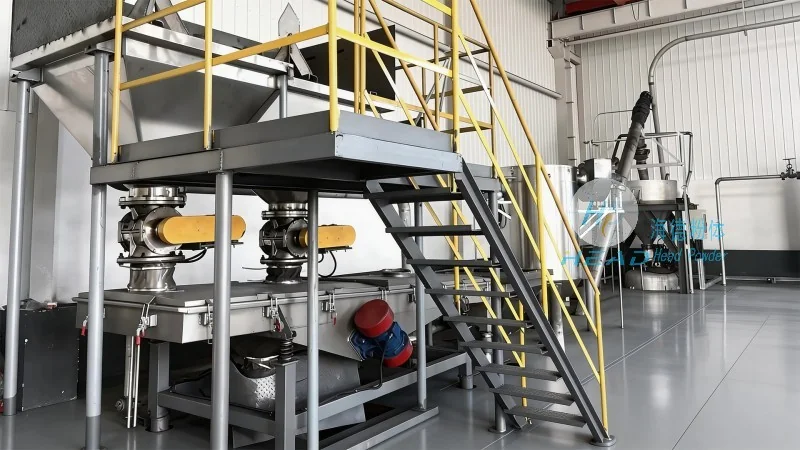
Technical Advantages and Performance Features
HeadPowder's cocoa powder conveying system offers several advantages that enhance operational efficiency and product quality. The stainless steel construction ensures hygiene compliance and resistance to corrosion, making it suitable for food-grade applications. The system's dust suppression features, such as sealed housings and integrated dust collection, maintain a clean working environment and comply with environmental regulations. The variable speed control allows for precise adjustment of the conveying rate, which is crucial for maintaining product consistency and preventing over-processing. Additionally, the system's low maintenance design reduces downtime and operational costs, providing long-term value to users.
Applications and Industry Use Cases
The cocoa powder conveying system is widely used in various industrial settings where fine powder handling is critical. In the food industry, it is employed in chocolate manufacturing, cocoa processing plants, and confectionery production lines to transport cocoa powder from storage to processing equipment. In the pharmaceutical sector, the system is utilized in the production of cocoa-based supplements and medicinal products, where contamination control and material purity are essential. The system's ability to handle hygroscopic materials also makes it suitable for chemical applications involving cocoa-derived compounds. By providing a reliable and efficient conveying solution, the system contributes to improved productivity and product quality across these industries.
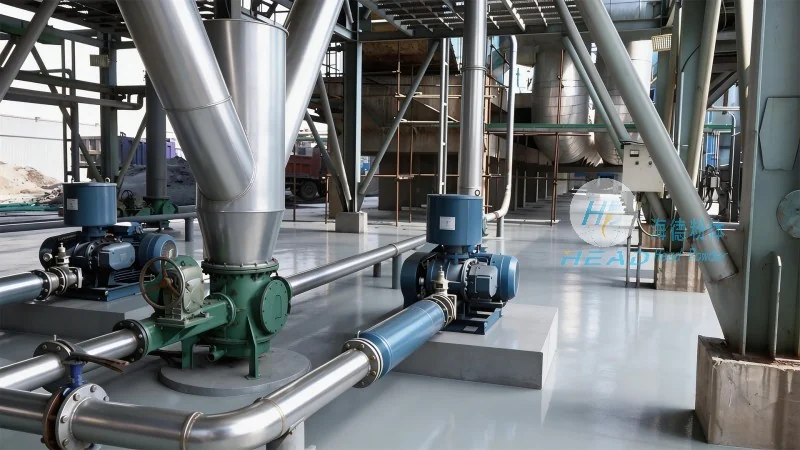
Company Commitment to Quality and Innovation
Shandong HeadPowder Engineering Co., Ltd. is committed to delivering high-quality, reliable, and innovative powder conveying solutions. The company adheres to strict quality control standards throughout the manufacturing process, ensuring that each system meets or exceeds industry specifications. Continuous research and development efforts focus on enhancing system performance, energy efficiency, and user-friendliness. HeadPowder's team of experienced engineers and technicians provides comprehensive support, from system design and installation to maintenance and troubleshooting. This commitment to excellence ensures that customers receive not only a superior product but also a trusted partner for their powder handling needs.