

Introduction to Coffee Pneumatic Conveying Systems: Structure and Working Principles
For coffee processing facilities, efficient and reliable material handling is crucial to maintaining product quality and operational efficiency. Coffee pneumatic conveying systems offer a sophisticated solution to transport coffee beans, grounds, or other related materials with precision and minimal contamination. This article provides an overview of the key components, operational principles, and benefits of coffee pneumatic conveying systems, with a focus on the engineering solutions provided by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field.
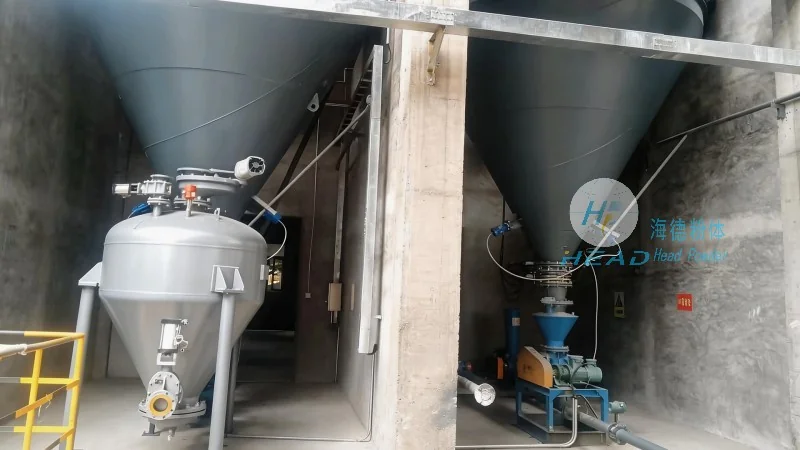
Core Components and Structural Design
The structure of a coffee pneumatic conveying system is engineered to ensure optimal performance and durability. Key components typically include a hopper for material storage, a rotary valve or feeder to control the flow of coffee, a conveying line (often equipped with bends and straight sections), a filter or separator to remove moisture or debris, and a receiver or discharge point for the material. The system may also incorporate a vacuum or pressure source, such as a blower or compressor, to generate the necessary airflow. The design emphasizes minimal pressure drops, smooth material flow, and easy maintenance, all of which are critical for consistent coffee processing.
Working Principles of Pneumatic Conveying
Coffee pneumatic conveying operates on the principle of using air to move solid particles. In a typical system, coffee is fed into the hopper and then discharged into the conveying line through a rotary valve. The air, supplied by a blower or compressor, creates a flow that lifts and transports the coffee particles through the system. The conveying process can be either vacuum-based (suction) or pressure-based (blow), depending on the application and material characteristics. The system’s efficiency depends on factors like air velocity, particle size, and the length of the conveying line. Proper design ensures that the coffee remains intact, avoiding breakage or damage that could affect flavor and quality.
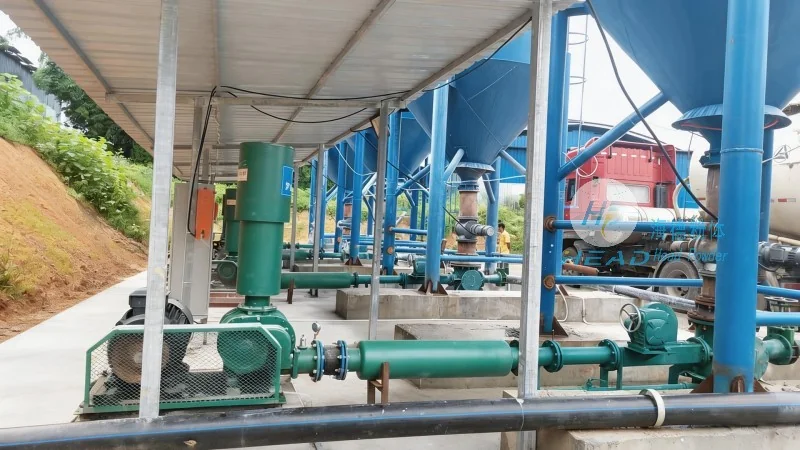
Benefits and Applications in Coffee Processing
Implementing a coffee pneumatic conveying system offers several advantages for coffee processing operations. These include reduced labor costs by automating material handling, minimized product contamination due to enclosed systems, and improved process control through precise flow regulation. The systems are particularly suitable for transporting coffee beans from storage to roasting equipment, or for moving ground coffee from grinding to packaging. Additionally, the compact design of modern pneumatic conveying systems allows for integration into existing coffee processing lines without significant space constraints. The technology also supports high-volume production, making it ideal for commercial coffee roasters and processing plants.
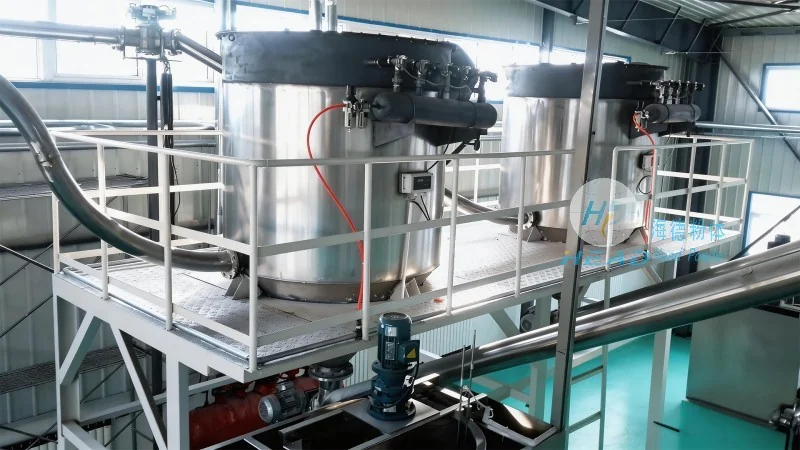
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a reputable manufacturer specializing in the design and production of pneumatic conveying systems for various industries, including coffee processing. With a focus on innovation and quality, the company has developed advanced solutions tailored to the unique needs of coffee production. HeadPowder’s engineering team leverages years of experience to create systems that meet international standards while ensuring durability and reliability. The company’s facilities in Shandong, China, are equipped with state-of-the-art technology and strict quality control measures to deliver products that enhance operational efficiency for coffee processing facilities worldwide.
Conclusion
Coffee pneumatic conveying systems represent a vital technology in modern coffee processing, offering efficient, clean, and reliable material handling solutions. By understanding the structural components and operational principles, coffee processing facilities can optimize their operations and maintain product quality. Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner in providing these advanced systems, combining expertise with cutting-edge engineering to support the coffee industry’s needs. For businesses seeking to enhance their coffee processing capabilities, investing in a well-designed pneumatic conveying system is a strategic decision that contributes to long-term success and efficiency.