

[BIN PUMP PNEUMATIC CONVEYING EQUIPMENT: INTRODUCTION AND STRUCTURAL PRINCIPLES]
Bin pump pneumatic conveying equipment is a specialized device widely used in industrial material handling applications. This equipment is designed to transport bulk materials such as powders, granules, and fine particles over long distances with high efficiency and minimal maintenance. The core of this system is the bin pump, which operates by creating a vacuum or pressure to move materials through a pipeline network.
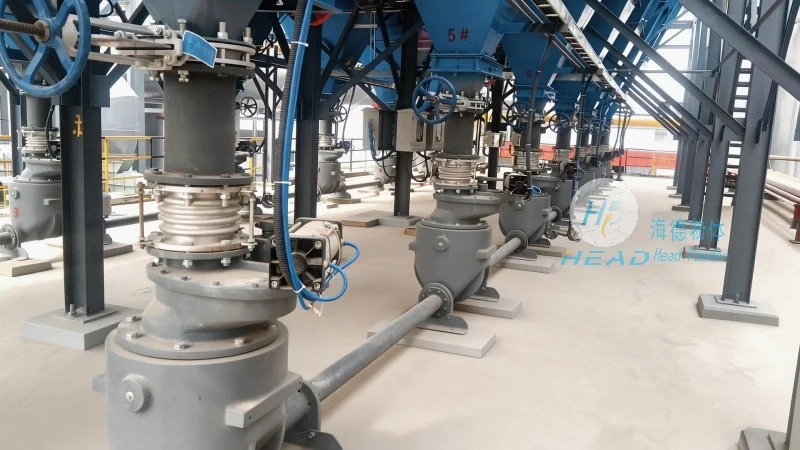
Overview of Bin Pump Pneumatic Conveying Systems
Bin pump systems are an essential part of modern material handling infrastructure, offering advantages over traditional methods like belt conveyors or screw conveyors. They are particularly effective for handling materials that are difficult to transport due to their physical properties, such as dustiness, abrasiveness, or sensitivity to moisture. The system typically consists of a hopper or storage bin, a bin pump unit, a conveying pipeline, and a discharge point. The bin pump acts as the central component, controlling the flow of material and the air pressure within the system.
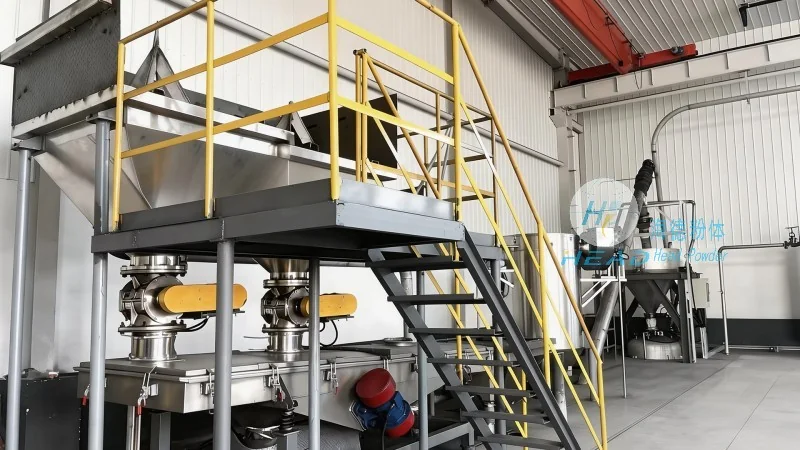
Structural Components of the Bin Pump
The bin pump, as the name suggests, is a vertical or horizontal cylinder that serves as the material storage and transport chamber. The main structural components include the pump body, which is usually made of high-quality steel or stainless steel to withstand the stresses of material handling. The pump features a hopper at the top for material feeding, a discharge valve at the bottom for material release, and an air inlet/outlet port for the pneumatic system. The design of the pump body is optimized to minimize material buildup and ensure smooth material flow. Additionally, the pump may include a pressure relief valve and a check valve to regulate pressure and prevent backflow.
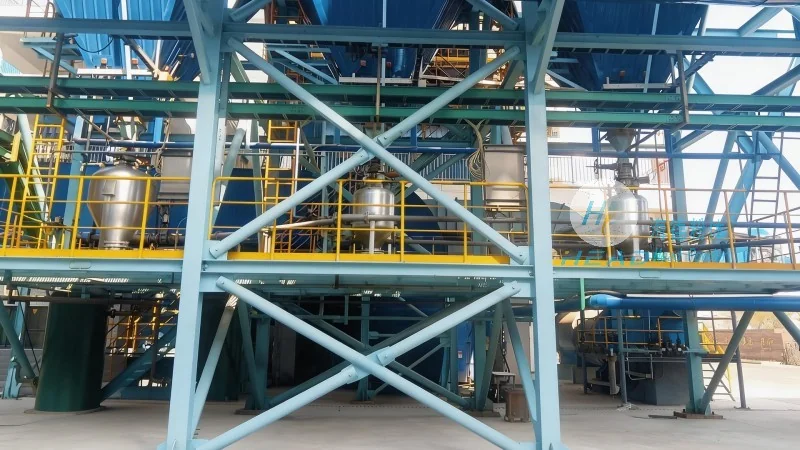
Working Principle of the Bin Pump System
The operation of a bin pump pneumatic conveying system is based on the principles of fluid dynamics and air pressure. The process begins with the material being fed into the hopper from a storage silo or hopper. The bin pump then creates a vacuum or pressure by controlling the air flow through the system. When the pump is in the suction mode, it draws air and material from the hopper into the pump chamber. The material is then accelerated and propelled through the conveying pipeline to the discharge point. The system can operate in either positive pressure or negative pressure modes, depending on the application requirements. The air flow is carefully controlled to ensure that the material is transported efficiently without clogging or degradation.
Key Advantages of Bin Pump Pneumatic Conveying
Bin pump systems offer several advantages over other material handling methods. They provide a closed system, which helps to contain dust and prevent environmental contamination. The system is also flexible, allowing for changes in material flow direction and distance without major modifications. Additionally, bin pumps are capable of handling a wide range of materials, from fine powders to coarse granules, with minimal maintenance. The energy efficiency of the system is another key benefit, as it uses less power compared to other conveying methods. The compact design of the bin pump also makes it suitable for installation in limited spaces.

About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a leading manufacturer of bin pump pneumatic conveying equipment. The company is headquartered in Shandong, China, and has established a strong reputation for producing high-quality, reliable equipment that meets the needs of various industrial sectors. HeadPowder specializes in designing and manufacturing customized bin pump systems tailored to the specific requirements of clients, ensuring optimal performance and efficiency. The company's commitment to quality and innovation has made it a trusted partner for businesses in the material handling industry.