

Introduction to Organic Fertilizer Pneumatic Conveying Systems: Structure and Working Principles
Organic fertilizer pneumatic conveying systems are advanced industrial solutions designed to efficiently transport bulk organic materials such as compost, manure, and other organic waste. These systems utilize air pressure or vacuum to move materials from one location to another, offering a clean, dust-free, and efficient method compared to traditional mechanical conveying methods. The technology is widely adopted in the agricultural and organic fertilizer production industries due to its ability to handle high volumes of material while maintaining product quality and reducing labor costs.
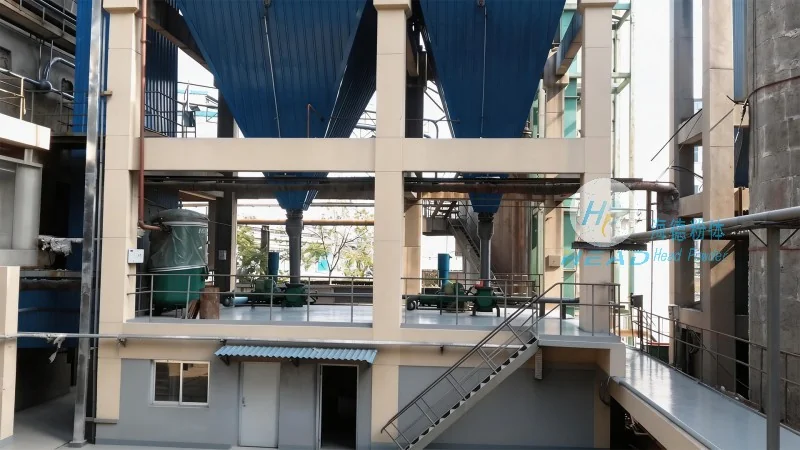
Key Components and Structural Design of the Pneumatic Conveying System
The organic fertilizer pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. comprises several critical components that work in tandem to ensure smooth operation. The main structural elements include the material hopper, air compressor or vacuum pump, conveying pipes, control valves, and material separation units. The material hopper is designed to store and feed the organic fertilizer into the system, ensuring a consistent flow of material. The air compressor or vacuum pump generates the necessary air pressure or vacuum to move the material through the pipes. The conveying pipes are typically made of durable materials like stainless steel or PVC to withstand the corrosive nature of organic fertilizers and ensure long-term durability. Control valves are used to regulate the air flow and material movement, allowing for precise control over the conveying process. Material separation units, such as cyclones or filters, are integrated to separate any fine particles or dust from the air, ensuring a clean discharge and protecting the system from clogging.
Working Principle of the Pneumatic Conveying System
The operation of the organic fertilizer pneumatic conveying system follows a systematic process. Initially, the organic fertilizer is loaded into the material hopper. The system then uses an air compressor to generate high-pressure air, which is introduced into the conveying pipes. As the air flows through the pipes, it carries the organic fertilizer particles along with it, creating a slurry-like mixture. The mixture is transported to the destination point, where it is deposited into the receiving container. The air, now containing fine particles, passes through the material separation unit, where the particles are separated from the air and returned to the system or disposed of appropriately. The clean air is then released back into the environment or recirculated if needed. This process ensures that the organic fertilizer is transported efficiently and without contamination, maintaining its quality and usability.
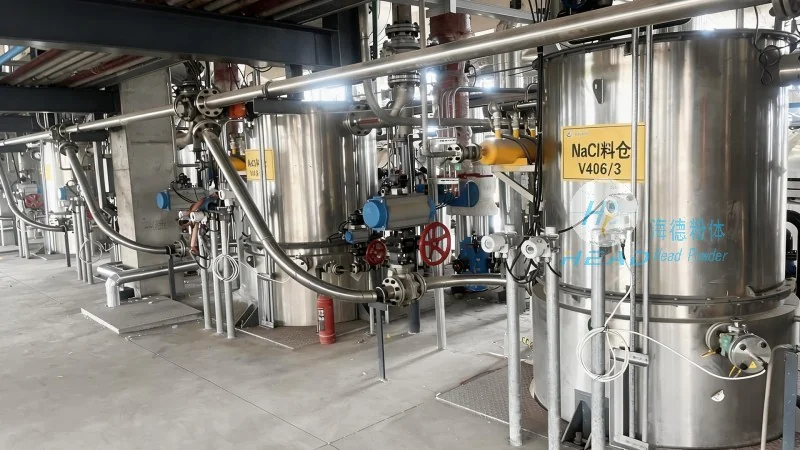
Advantages of Using Organic Fertilizer Pneumatic Conveying Systems
Implementing organic fertilizer pneumatic conveying systems offers numerous advantages over traditional conveying methods. Firstly, the system provides a dust-free and hygienic environment, which is crucial for organic fertilizer production as it helps maintain product quality and reduces the risk of contamination. Secondly, the system is highly efficient in terms of material handling, capable of transporting large volumes of organic fertilizer in a short period, thereby increasing production throughput. Thirdly, the system reduces labor costs as it minimizes the need for manual handling and reduces the risk of worker exposure to dust and other hazards. Additionally, the system is flexible and can be easily integrated into existing production lines, allowing for seamless expansion or modification of the production process. The durability of the components, such as the conveying pipes and control valves, ensures long-term operation with minimal maintenance, contributing to overall cost savings.
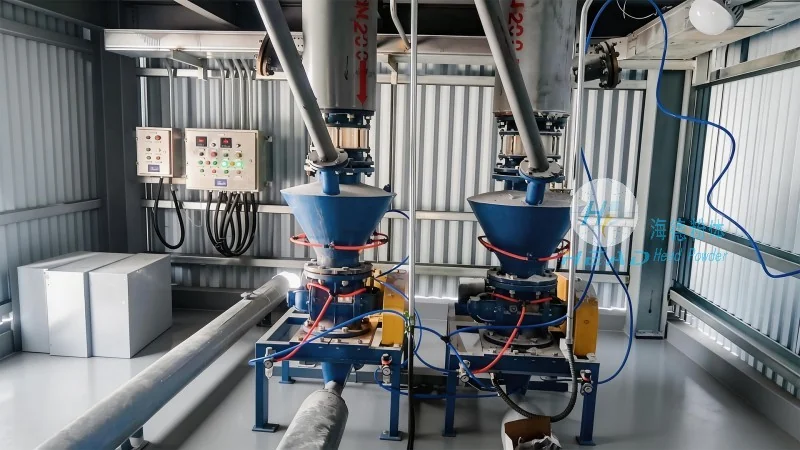
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial conveying systems, including organic fertilizer pneumatic conveying lines. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner in the agricultural and organic fertilizer industry. The company is headquartered in Shandong, China, and leverages advanced technology and engineering expertise to design and manufacture high-performance conveying systems tailored to the specific needs of its clients. HeadPowder's products are known for their reliability, efficiency, and durability, making them a preferred choice for businesses looking to enhance their material handling processes. The company's team of experienced engineers and technicians provides comprehensive support, from system design and installation to maintenance and after-sales service, ensuring that clients receive the best possible solutions for their conveying needs.
Conclusion
Organic fertilizer pneumatic conveying systems represent a significant advancement in material handling technology, offering efficient, clean, and cost-effective solutions for the agricultural and organic fertilizer sectors. The systems, as exemplified by those from Shandong HeadPowder Engineering Co., Ltd., combine advanced structural design with reliable working principles to deliver superior performance. By leveraging these systems, businesses can enhance their production capabilities, maintain product quality, and reduce operational costs. As the demand for organic fertilizers continues to grow, the adoption of such advanced conveying systems will play a crucial role in meeting the industry's needs and ensuring sustainable agricultural practices.