

Operation Process and Working Principle of Automatic Weighing Powder Pneumatic Conveying Machine
Automatic weighing powder pneumatic conveying machines are advanced industrial equipment designed to handle the precise and efficient transport of bulk powders. These systems integrate multiple functional components to ensure accurate material measurement and controlled pneumatic transport, making them essential in various industries such as food processing, pharmaceuticals, and chemical manufacturing. The following sections will detail the operational process and working principles of these machines, providing a comprehensive understanding of their functionality and benefits.
Key Components and Their Roles
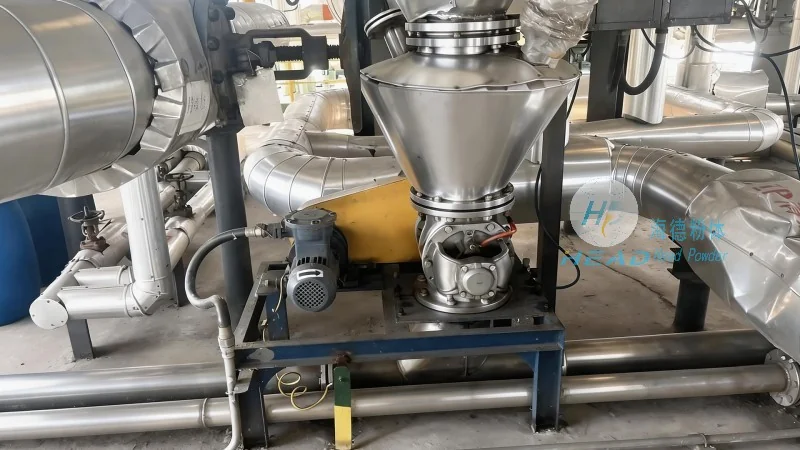
The operation of an automatic weighing powder pneumatic conveying machine relies on several critical components that work in tandem to achieve accurate material handling. The primary components include a hopper for material storage, a weighing scale to monitor the mass of the powder, a pneumatic conveying system with a blower or compressor to generate airflow, a control system to regulate the process, and a discharge outlet for transporting the material to the next stage of production. Each component plays a vital role in maintaining the system's efficiency and precision. For instance, the hopper ensures a consistent supply of powder, while the weighing scale provides real-time data on the quantity being conveyed. The pneumatic system, driven by the blower, creates the necessary pressure and airflow to move the powder through the pipeline, and the control system coordinates all actions to prevent overloading or underflow. This integration of components allows for seamless and automated operation, reducing human intervention and potential errors.
Operation Process: Step-by-Step Overview
The operational process of an automatic weighing powder pneumatic conveying machine can be broken down into several sequential steps that ensure the accurate and controlled transport of bulk powders. The process begins with the loading of the hopper with the target powder material. Once the hopper is filled, the control system activates the weighing scale to start measuring the mass of the powder. As the material is drawn from the hopper into the conveying line, the scale continuously monitors the weight, providing feedback to the control system. The control system then adjusts the airflow and conveying speed based on the real-time weight data to maintain the desired flow rate. When the target weight is reached, the control system signals the blower to stop, and the material is discharged from the system into the next processing unit. This step-by-step process ensures that the amount of powder conveyed is precisely controlled, minimizing waste and optimizing production efficiency. The system also includes safety features such as overload protection and air pressure monitoring to prevent equipment damage and ensure operational safety.
Working Principles: How It Works
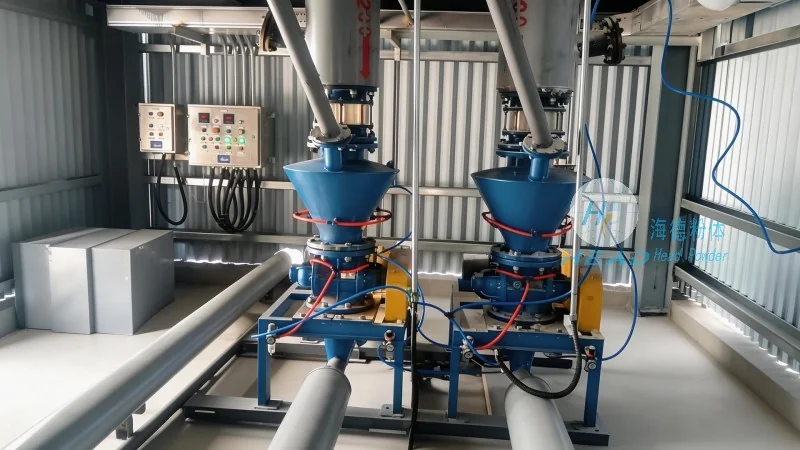
The working principle of an automatic weighing powder pneumatic conveying machine is based on the fundamental concept of pneumatic transport, where powders are conveyed through a pipeline using air pressure. The system operates by creating a pressure differential between the hopper and the discharge point. The blower or compressor generates high-pressure air that is introduced into the conveying line, creating a flow of air that carries the powder particles. The powder is suspended in the air stream and transported through the pipeline to the discharge outlet. The weighing scale is integrated into the system to monitor the mass of the powder being conveyed, ensuring that the amount delivered matches the set target. The control system uses this data to regulate the airflow and conveying speed, maintaining the desired flow rate. This closed-loop control system ensures that the operation is precise and efficient, adapting to changes in material properties or system conditions. The system also incorporates features such as air filtration and moisture control to maintain the quality of the conveyed powder, making it suitable for applications where material purity is critical.
Benefits and Applications
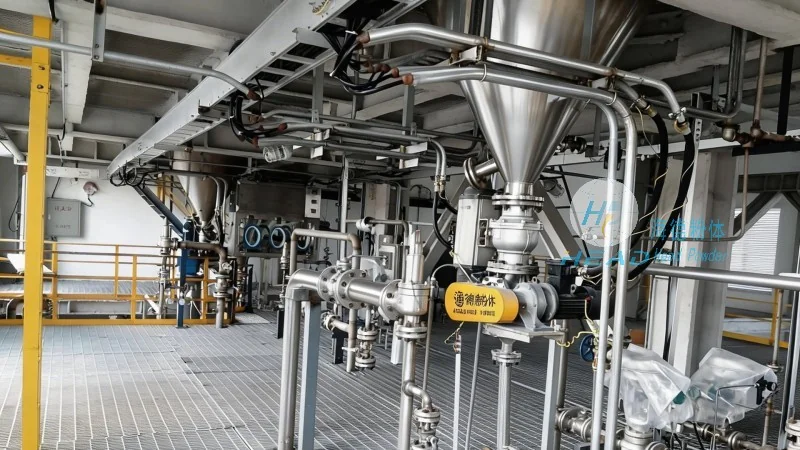
Automatic weighing powder pneumatic conveying machines offer numerous benefits that make them ideal for industries requiring precise material handling. These benefits include improved accuracy in material measurement, reduced labor costs due to automated operation, enhanced safety through integrated safety features, and increased production efficiency by minimizing downtime and waste. The system's ability to handle a wide range of powder types, from fine to coarse, makes it versatile for various applications. For example, in the pharmaceutical industry, these machines are used to transport active pharmaceutical ingredients (APIs) with high precision, ensuring that the correct dosage is delivered. In the food industry, they are used to convey ingredients such as flour, sugar, and spices, maintaining product quality and consistency. In the chemical industry, they handle raw materials like powders for manufacturing processes, ensuring that the correct proportions are mixed. The versatility and reliability of these machines make them a valuable asset in modern industrial operations.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of advanced powder handling equipment. With a focus on innovation and quality, the company specializes in designing and manufacturing automatic weighing powder pneumatic conveying machines tailored to meet the specific needs of various industries. Headpowder's products are known for their precision, efficiency, and reliability, making them trusted solutions for material handling challenges. The company's headquarters is located in Shandong, China, where it has established a strong presence in the industry with a commitment to customer satisfaction and technological advancement. Headpowder's team of experts works closely with clients to understand their operational requirements and provide customized solutions that enhance productivity and reduce costs. By leveraging advanced technology and rigorous quality control, Headpowder ensures that its equipment meets the highest standards, delivering long-term value to its customers.