

Operation Process and Working Principle of Corn Granule Material Handling System Equipment
For agricultural and food processing industries, efficient handling of corn granules is crucial for maintaining production efficiency and product quality. The corn granule material handling system, developed by Shandong HeadPowder Engineering Co., Ltd. (referred to as HeadPowder), is designed to address these needs through advanced engineering and reliable operation. This system integrates various components to ensure smooth and continuous transport of corn granules from storage to processing or packaging stages, leveraging the expertise of HeadPowder in material handling technology.
Key Components of the Material Handling System
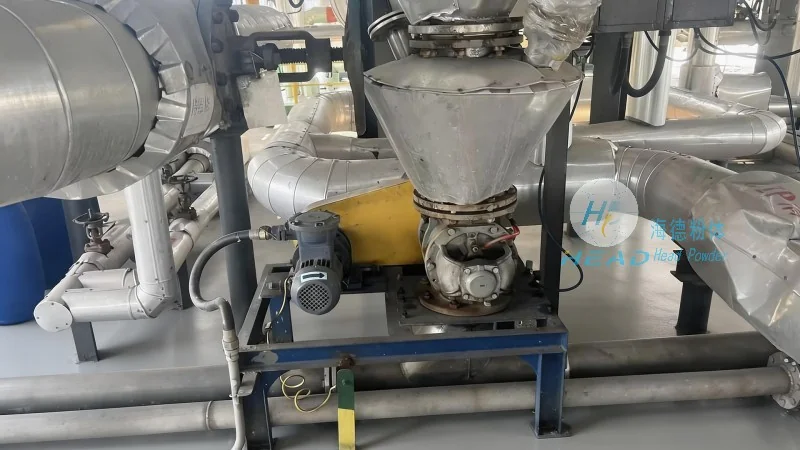
The corn granule material handling system consists of several key components that work in tandem to achieve optimal performance. These include feeders, conveyors, storage silos, and control systems. Each component is carefully selected and integrated to handle the specific characteristics of corn granules, such as their size, density, and moisture content. The feeders are responsible for evenly distributing the corn granules into the conveyor system, while the conveyors transport the material through the production line. Storage silos provide temporary storage capacity, allowing for buffer management during peak production periods. The control system monitors and regulates the entire process, ensuring consistent performance and minimizing downtime.
Operation Process of the System
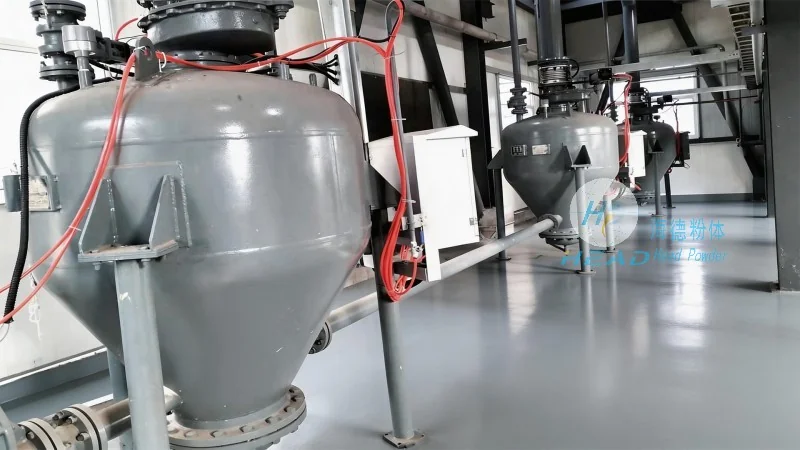
The operation process of the corn granule material handling system begins with the loading of corn granules into the storage silo. The silo is equipped with a level sensor to monitor the material level, which triggers the feeder to start when the level reaches a predetermined threshold. The feeder then discharges the corn granules into the conveyor belt, which transports the material to the next processing stage. The conveyor system may include multiple sections, such as a horizontal conveyor and a vertical lift, depending on the layout of the facility. The vertical lift is used to elevate the corn granules to a higher level, enabling them to be transported to different parts of the production line. At each stage, the system is equipped with sensors to detect any blockages or irregularities, ensuring that the process is interrupted only when necessary.
Working Principle of the System
The working principle of the corn granule material handling system is based on mechanical and pneumatic principles. The feeders use a screw or belt mechanism to move the corn granules, while the conveyors utilize a belt or chain system to transport the material. The storage silos are designed with a conical bottom to facilitate the discharge of the material, reducing the risk of clogging. The control system uses sensors and actuators to regulate the flow rate and pressure, ensuring that the material is transported at a consistent speed. The system is also equipped with safety features, such as emergency stop buttons and overload protection, to prevent accidents and damage to the equipment.
Advantages and Applications
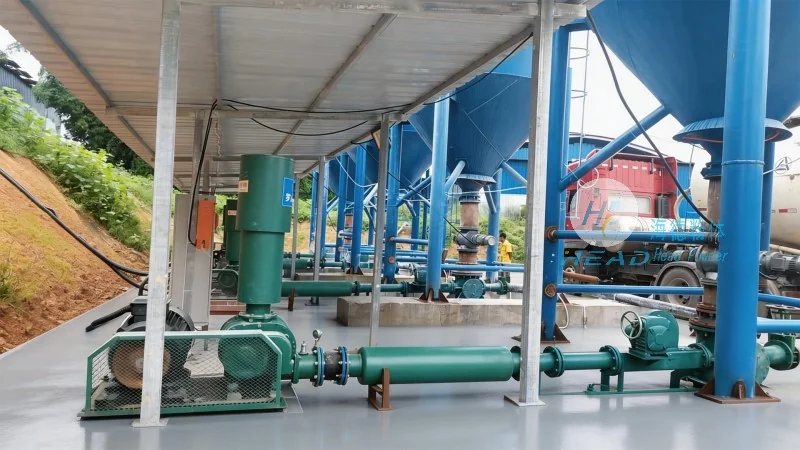
The corn granule material handling system developed by HeadPowder offers several advantages for agricultural and food processing industries. The system is designed to handle large volumes of corn granules efficiently, reducing labor costs and increasing production capacity. The components are made of high-quality materials, ensuring durability and long service life. The system is also easy to maintain and operate, with minimal downtime required for routine maintenance. The system is widely used in corn processing plants, feed mills, and food manufacturing facilities, where the efficient handling of corn granules is essential for maintaining product quality and meeting production demands.