

Operation Process and Working Principle of Ammonia Fertilizer Material Handling Equipment
Ammonia fertilizer is a critical input in modern agriculture, providing essential nitrogen to crops for improved growth and yield. The efficient handling and transportation of ammonia fertilizer from production facilities to distribution centers or farms are vital for maintaining supply chain reliability and operational efficiency. This article explores the operation process and working principle of specialized equipment designed for ammonia fertilizer material handling, detailing key components, operational steps, and technical aspects that ensure safe and effective material transport.
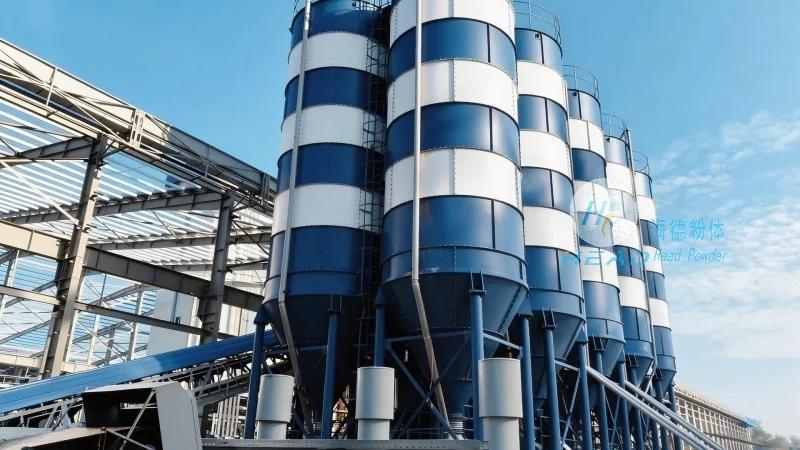
Overview of Ammonia Fertilizer Handling Equipment
Ammonia fertilizer handling equipment, including pneumatic conveyors, screw conveyors, and bulk material handling systems, is engineered to manage the unique properties of ammonia fertilizer. These systems are designed to handle the material's corrosive nature, high vapor pressure, and the need for precise temperature and pressure control. The equipment typically comprises feed hoppers, conveying pipes, control valves, and safety mechanisms to ensure compliance with industrial safety standards and environmental regulations.
Key Components and Their Functions
The core components of ammonia fertilizer handling equipment include feed hoppers (for storing and feeding fertilizer), conveying mechanisms (e.g., screw or pneumatic systems for material transport), control valves and regulators (to manage pressure and flow rates), and safety devices (such as pressure relief valves and gas detectors). Each component plays a vital role in maintaining material integrity and ensuring safe operation. For example, the feed hopper ensures consistent material flow, while the conveying system transports it through pipelines. Control valves regulate pressure and flow to prevent over-pressurization or blockages, and safety devices protect against leaks or explosions.
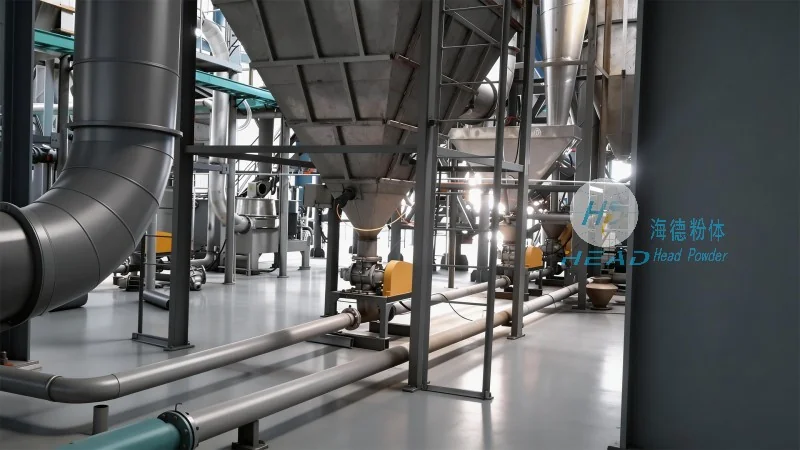
Operation Process: Step-by-Step Breakdown
The operation process of ammonia fertilizer handling equipment begins with loading fertilizer into the feed hopper. The hopper is equipped with a level sensor to monitor material volume, ensuring an even feed rate. Once filled, the material is discharged into the conveying system. In pneumatic systems, fertilizer is mixed with air and transported via pressure. Screw conveyors use rotating screws to push material forward. The conveying system moves fertilizer to a storage silo or loading station. At the destination, material is discharged into a receiving vessel, and the system prepares for the next batch. A central control system monitors pressure, flow rate, and temperature, adjusting operations as needed for optimal performance.
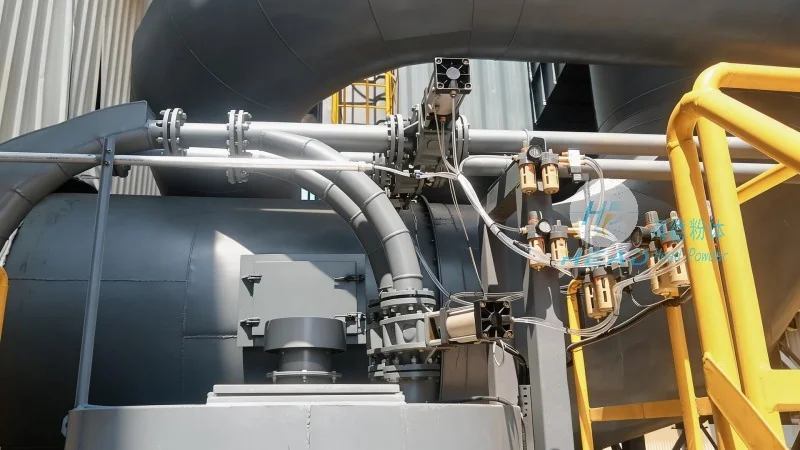
Working Principle: How the Equipment Functions
The working principle of ammonia fertilizer handling equipment is based on fluid dynamics and mechanical transport. Pneumatic systems suspend fertilizer in air streams, using pressure differentials to move material. Screw conveyors operate via rotating screws, creating positive displacement to push material forward. Both systems rely on precise pressure, flow, and temperature control to prevent degradation or blockages. The conveying speed and screw pitch are adjusted to regulate flow and prevent buildup, ensuring safe and efficient transport.
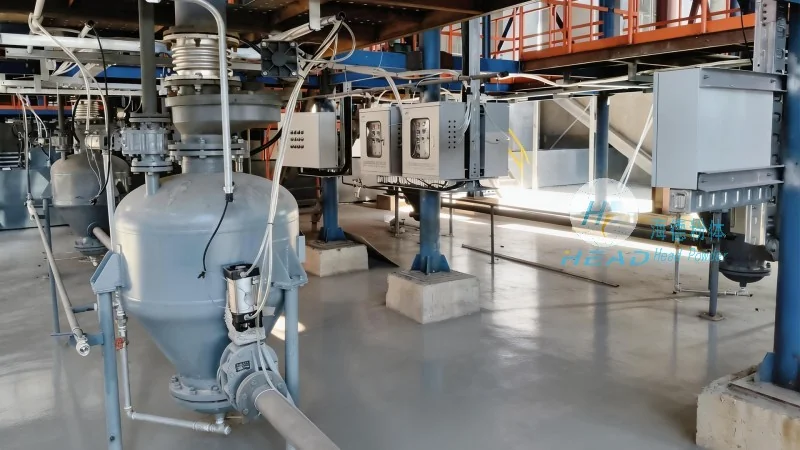
Safety and Maintenance Considerations
Due to ammonia fertilizer's hazardous nature, safety is paramount. Regular maintenance is essential to ensure reliable and safe operation. This includes checking for leaks in the conveying system, inspecting control valves and regulators, and verifying safety device functionality. Routine maintenance schedules prevent equipment failure and ensure industry compliance. Operators must be trained on proper equipment use and emergency procedures. By adhering to strict safety protocols and maintenance practices, the risk of accidents and material loss is minimized, ensuring smooth fertilizer handling.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of specialized equipment for ammonia fertilizer and bulk material handling. The company focuses on innovation and quality, designing equipment that meets high industrial standards. HeadPowder's products address ammonia fertilizer's unique challenges, including corrosive properties and precise control needs. HeadPowder's headquarters is in Shandong, China, with a team of experienced engineers and technicians dedicated to developing cutting-edge solutions for the agricultural and chemical sectors. The company's commitment to customer satisfaction and product excellence has established it as a trusted partner for businesses in these industries.