

Operation Process and Working Principle of Nitrogen Circulation Powder Conveying Machine
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in providing advanced powder handling solutions. The company’s expertise lies in the design and production of nitrogen circulation powder conveying machines, which are essential for industries requiring precise and controlled powder transport under inert gas environments. These systems are engineered to ensure safety, efficiency, and reliability in applications such as pharmaceuticals, food processing, and chemical manufacturing.
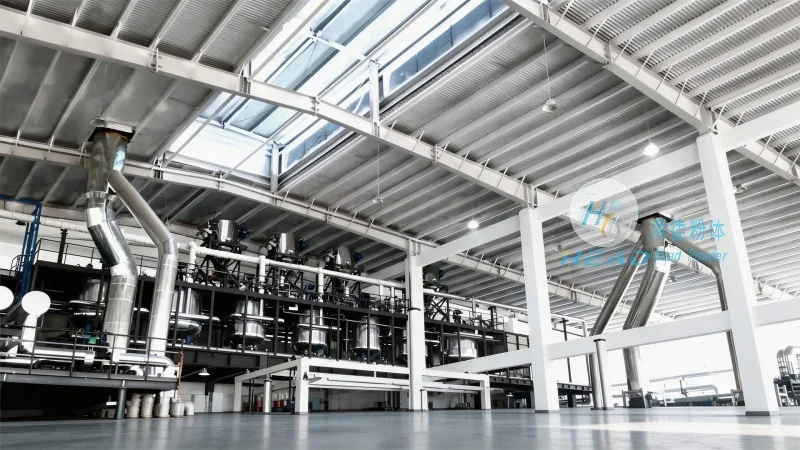
Key Features of the Nitrogen Circulation Powder Conveying Machine
The nitrogen circulation powder conveying machine by HeadPowder is designed with several key features that enhance its performance and adaptability. It incorporates a closed-loop nitrogen system that maintains an inert atmosphere throughout the conveying process, preventing oxidation and contamination of sensitive powders. The machine utilizes positive displacement technology, which ensures consistent and uniform powder flow, even for fine or cohesive powders. Additionally, the system is equipped with adjustable speed controls and pressure monitoring, allowing operators to optimize conveying parameters based on the specific characteristics of the material being handled. The robust construction and modular design make it suitable for various industrial applications, from small-scale laboratory use to large-scale production lines.
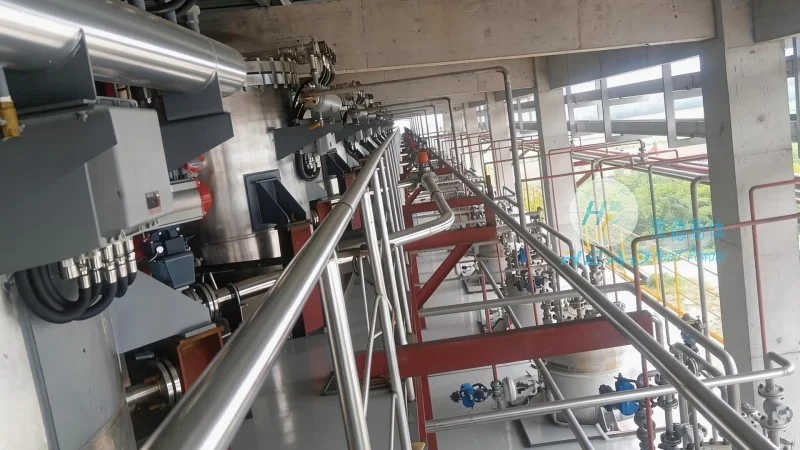
Operation Process of the Nitrogen Circulation Powder Conveying Machine
The operation of the nitrogen circulation powder conveying machine involves a series of steps to ensure smooth and efficient powder transport. First, the system is prepared by connecting the inlet and outlet hoses to the powder source and destination, respectively. The nitrogen gas is then pressurized and circulated through the system, creating a stable inert environment. Next, the conveying pump is activated, which draws the powder from the source and transports it through the pipeline under the pressure of the nitrogen gas. The speed of the pump and the pressure of the nitrogen are adjusted to control the flow rate of the powder, ensuring that the material is conveyed at the desired rate without clogging or degradation. During operation, the system continuously monitors the pressure and flow parameters, providing real-time feedback to the operator. The process continues until the target amount of powder has been transferred, at which point the pump is stopped, and the nitrogen flow is reduced to maintain the inert atmosphere. Finally, the system is cleaned and maintained to prepare it for the next cycle.
Working Principle of the Nitrogen Circulation Powder Conveying Machine
The working principle of the nitrogen circulation powder conveying machine is based on the principles of gas-solid two-phase flow and inert gas protection. The system operates by creating a closed loop where nitrogen gas is continuously circulated and pressurized. The powder is introduced into the system at the inlet, where it is mixed with the nitrogen gas and carried through the pipeline by the pressure differential. The positive displacement pump, typically a rotary lobe or screw pump, provides the necessary pressure to move the powder mixture. The nitrogen gas acts as a carrier, preventing the powder from coming into contact with air and thus avoiding oxidation or moisture absorption. The system maintains a constant pressure and temperature, which helps to preserve the quality of the powder and ensure consistent conveying performance. The control system regulates the flow of nitrogen and the speed of the pump, allowing for precise control over the conveying process. This design ensures that the powder is transported safely and efficiently, meeting the stringent requirements of industries that handle sensitive materials.
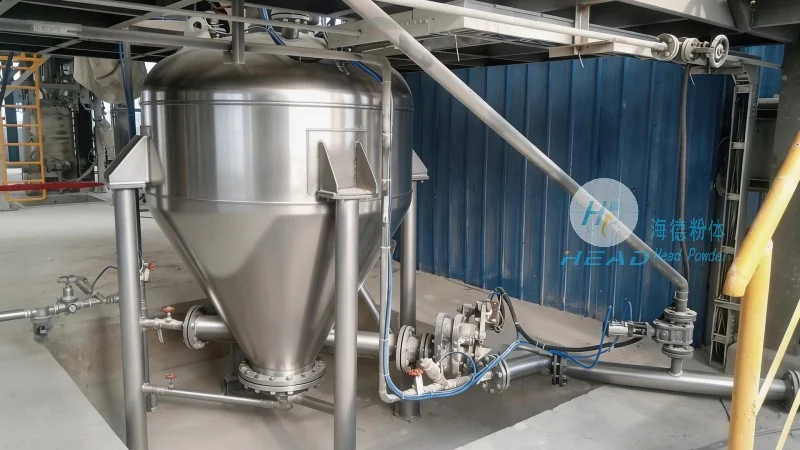
Applications and Benefits of the Nitrogen Circulation Powder Conveying Machine
The nitrogen circulation powder conveying machine is widely used in industries that require the transport of powders in an inert environment. In the pharmaceutical industry, it is used to convey active pharmaceutical ingredients (APIs) and excipients, ensuring that the materials remain stable and free from contamination. In the food processing industry, it is used to transport food powders such as sugar, flour, and spices, maintaining the freshness and quality of the products. In the chemical industry, it is used to handle reactive powders and chemicals, preventing reactions with air and ensuring safety. The benefits of using this machine include improved product quality, reduced waste, and enhanced safety. The closed-loop system minimizes the risk of dust explosions and contamination, while the precise control of conveying parameters ensures that the powder is handled with minimal degradation. Additionally, the machine is energy-efficient and easy to maintain, making it a cost-effective solution for powder handling needs.