

Operation Process and Working Principle of Corn Kernels Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced corn kernels pneumatic conveying systems. These systems are engineered to efficiently transport corn kernels and other granular materials with precision and reliability. Understanding the operation process and working principle of such equipment is crucial for optimizing material handling in agricultural and food processing industries.
Working Principle of Pneumatic Conveying Systems
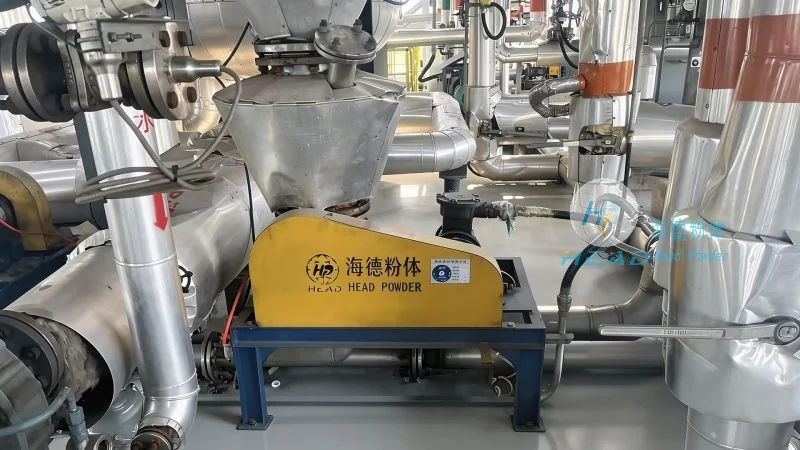
The core of a corn kernels pneumatic conveying system lies in its ability to use air pressure to move materials. The system typically consists of a hopper, a conveyor line, a control valve, and a receiver. The process begins with the corn kernels being fed into the hopper. As air is introduced into the system, it creates a low-pressure zone within the conveyor line. This pressure differential draws the corn kernels into the air stream, allowing them to be transported through the pipeline to the receiver. The control valve plays a critical role in regulating the air flow and material discharge, ensuring smooth and controlled operation.
Operation Process Step-by-Step
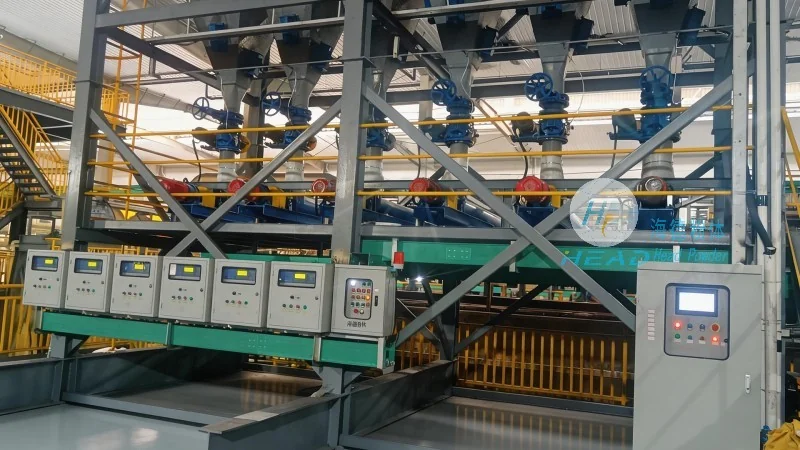
The operation of a corn kernels pneumatic conveying system involves several key steps. First, the corn kernels are loaded into the hopper. The system then activates the air compressor, which generates the necessary air pressure. The control valve opens, allowing air to enter the conveyor line. Simultaneously, the corn kernels are drawn into the air stream as the pressure differential is established. The material travels through the pipeline to the receiver, where it is collected. The control valve then adjusts the air flow to maintain the desired conveying rate. This process is continuous and can be automated to handle large volumes of corn kernels efficiently.
Key Components and Their Functions
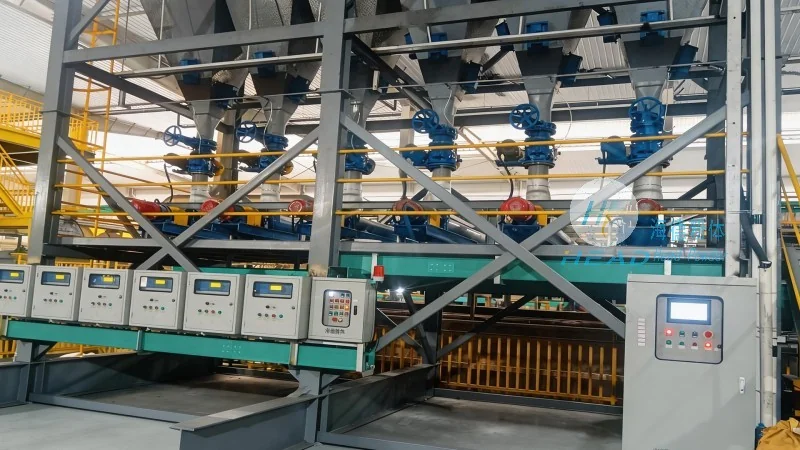
Several components work together to ensure the effective operation of the corn kernels pneumatic conveying equipment. The hopper serves as the storage and feeding unit, providing a consistent supply of corn kernels to the system. The air compressor generates the high-pressure air required to create the pressure differential. The conveyor line, often made of stainless steel or other corrosion-resistant materials, transports the corn kernels through the system. The control valve regulates the air flow and material discharge, preventing blockages and ensuring smooth operation. The receiver collects the conveyed corn kernels and can be designed for easy unloading. Each component is critical to the overall performance and efficiency of the system.
Advantages of Corn Kernels Pneumatic Conveying Equipment
Using pneumatic conveying systems for corn kernels offers several advantages over traditional methods. These systems are highly efficient in terms of material handling, as they can transport large volumes of corn kernels with minimal labor. They also provide a hygienic and clean environment, which is essential for food processing applications. The equipment is designed to minimize material degradation and loss, ensuring high product quality. Additionally, the systems are flexible and can be adapted to different production requirements, making them suitable for various industrial settings.
Applications in the Agricultural and Food Industry
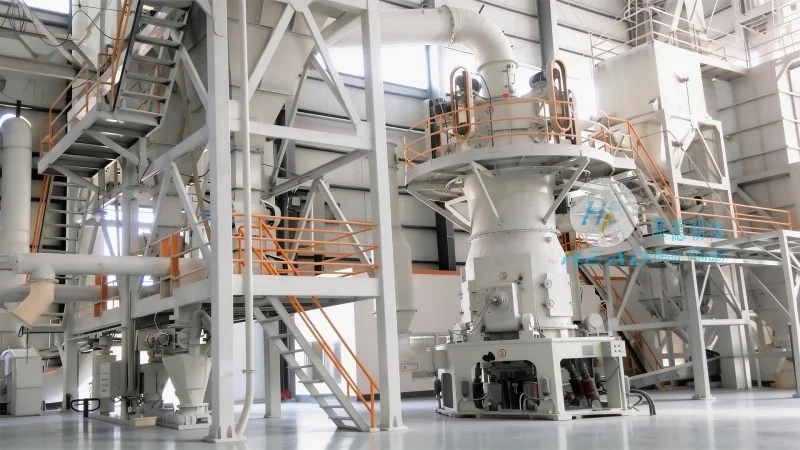
Corn kernels pneumatic conveying equipment is widely used in the agricultural and food processing sectors. In grain storage facilities, these systems are used to transfer corn kernels from storage silos to processing plants. In food processing industries, they are employed to move corn kernels to milling or grinding operations. The equipment is also used in feed manufacturing, where it helps in the efficient handling of raw materials. The reliability and efficiency of these systems make them a preferred choice for businesses looking to optimize their material handling processes.