

Principle and Application Scenarios of Pneumatic Conveying Systems for Ash Storage Materials
Efficient material handling is a critical aspect of industrial operations, particularly in facilities that manage ash storage and related processes. The pneumatic conveying system for ash storage materials, developed by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated solution designed to optimize the transport of bulk materials within industrial environments. This system combines advanced engineering principles with practical application, ensuring reliable and efficient material movement from storage silos to processing or disposal areas.
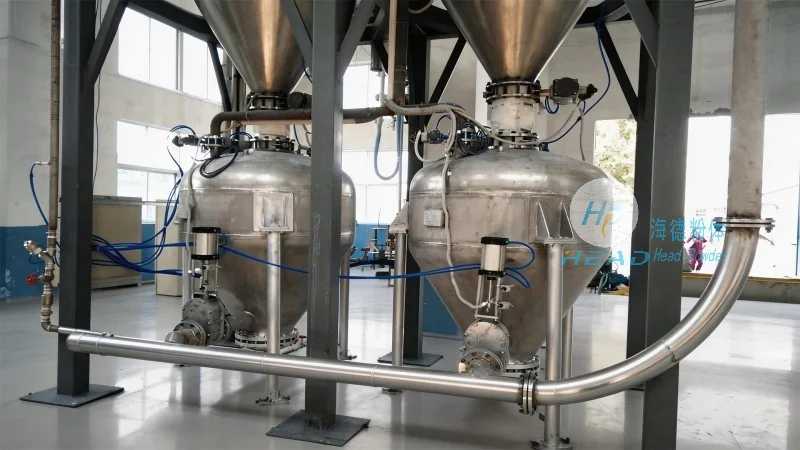
Understanding the Principle of Pneumatic Conveying for Ash Storage Materials
The core of the pneumatic conveying system lies in its ability to transport dry bulk materials, such as fly ash or other ash byproducts, using a pressurized or vacuum air stream. Unlike traditional mechanical conveying methods, which rely on belts, buckets, or screws, pneumatic systems utilize air to move materials through pipelines. For ash storage applications, this approach offers several advantages, including reduced equipment wear, minimal material degradation, and the ability to handle materials with high moisture content or fine particle sizes. The system typically operates under positive pressure, where air is forced through the pipeline, carrying the ash particles forward. Alternatively, negative pressure systems can be employed, drawing materials into the pipeline using a vacuum. The choice of pressure type depends on the specific characteristics of the ash, the distance to be conveyed, and the overall system layout. In ash storage scenarios, positive pressure systems are often preferred due to their ability to handle larger volumes and maintain consistent material flow, while minimizing the risk of dust emissions and ensuring compliance with environmental regulations.
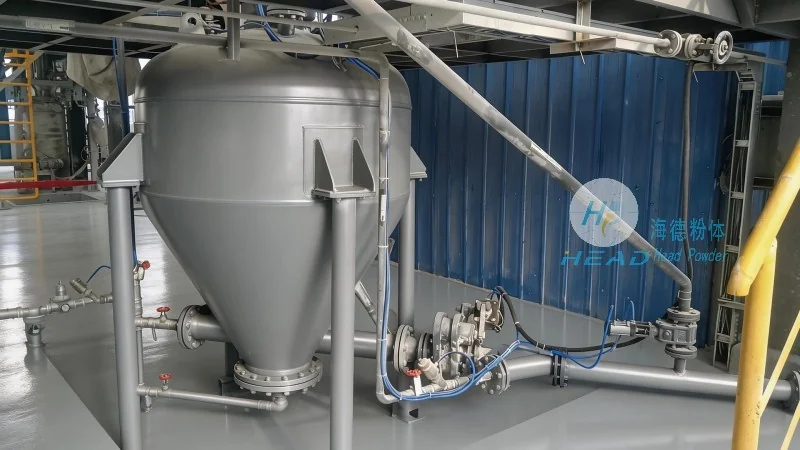
Key Features and Technical Advantages of the System
Shandong HeadPowder Engineering Co., Ltd. has integrated several key features into their pneumatic conveying system for ash storage materials to enhance performance and reliability. One of the primary advantages is the system's adaptability to varying ash properties. The design allows for the handling of ash with different particle sizes, moisture levels, and bulk densities, ensuring consistent conveying efficiency regardless of material variations. Additionally, the system incorporates advanced control mechanisms that monitor air pressure, flow rate, and material level in real-time. These controls help maintain optimal operating conditions, prevent blockages, and adjust the conveying rate based on demand. The use of high-quality materials for the pipeline and components further enhances durability, reducing maintenance requirements and extending the system's service life. The system also features integrated dust collection and filtration components, which are essential for maintaining air quality and meeting environmental standards in industrial settings. By combining these technical features, the pneumatic conveying system provides a robust and efficient solution for ash storage facilities, ensuring smooth material transfer while minimizing operational costs.
Application Scenarios and Operational Benefits
The pneumatic conveying system for ash storage materials is widely applicable across various industrial sectors, including power plants, cement factories, and waste management facilities. In power plants, for example, the system efficiently transports fly ash from storage silos to ash handling units or disposal sites, supporting the plant's operational efficiency and reducing the need for manual handling. The system's ability to handle large volumes of ash at high speeds minimizes downtime and improves overall plant productivity. In cement factories, the system aids in the transport of ash as a supplementary cementitious material, contributing to the production of high-quality cement while optimizing material usage. The system's flexibility also makes it suitable for waste management facilities, where it can transport ash from incineration processes to storage or recycling facilities. Operational benefits of the system extend beyond material transport efficiency. By reducing the reliance on traditional mechanical conveying methods, the system lowers maintenance costs and equipment wear. The minimal dust generation and effective filtration systems also contribute to a safer working environment and compliance with environmental regulations. Furthermore, the system's modular design allows for easy integration into existing industrial setups, reducing installation time and complexity. These benefits make the pneumatic conveying system a preferred choice for facilities seeking to enhance their material handling capabilities while maintaining operational efficiency and environmental responsibility.
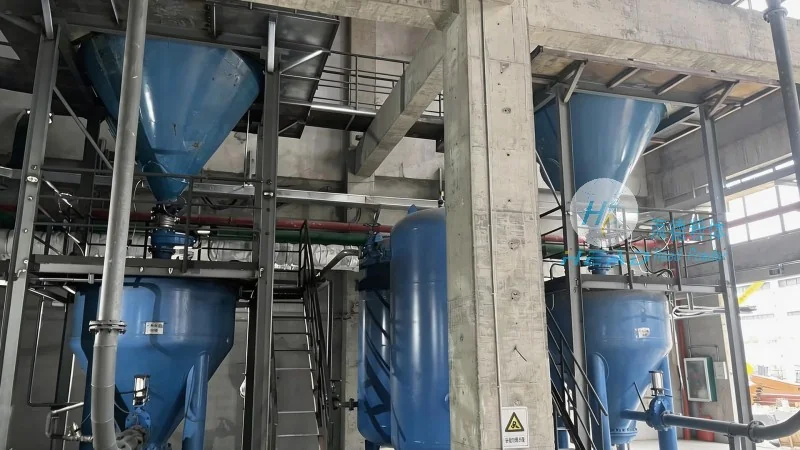
Company Background and Expertise in Pneumatic Conveying Solutions
As a leading manufacturer in the field of bulk material handling, Shandong HeadPowder Engineering Co., Ltd. has established itself as a trusted provider of pneumatic conveying systems for ash storage materials. With years of experience in industrial engineering and material handling, the company has developed a deep understanding of the challenges faced by facilities managing ash and other bulk materials. HeadPowder's expertise lies in designing customized solutions that address the specific needs of each client, ensuring optimal performance and reliability. The company's team of engineers and technicians works closely with clients to assess their operational requirements, material characteristics, and environmental constraints, tailoring the pneumatic conveying system to meet their unique needs. This customer-centric approach has enabled HeadPowder to build a strong reputation for delivering high-quality, efficient, and reliable systems that enhance industrial productivity. The company's commitment to innovation and continuous improvement is reflected in its use of advanced materials, control technologies, and design methodologies. By staying at the forefront of industrial trends and technological advancements, HeadPowder ensures that its pneumatic conveying systems remain cutting-edge and capable of meeting the evolving demands of the industry. This expertise and dedication to quality have made HeadPowder a preferred partner for facilities seeking to optimize their ash storage and material handling processes.