

Principle and Working Scene Characteristics of Automatic Weighing Material Pneumatic Conveying Machi
Automatic weighing material pneumatic conveying machines represent a sophisticated solution in material handling, integrating advanced pneumatic technology with precise weighing mechanisms to ensure efficient and accurate material transport across various industrial applications. These systems are designed to handle a wide range of bulk materials, from fine powders to granules, while maintaining high levels of operational efficiency and product integrity.
Working Principle of Pneumatic Conveying Technology
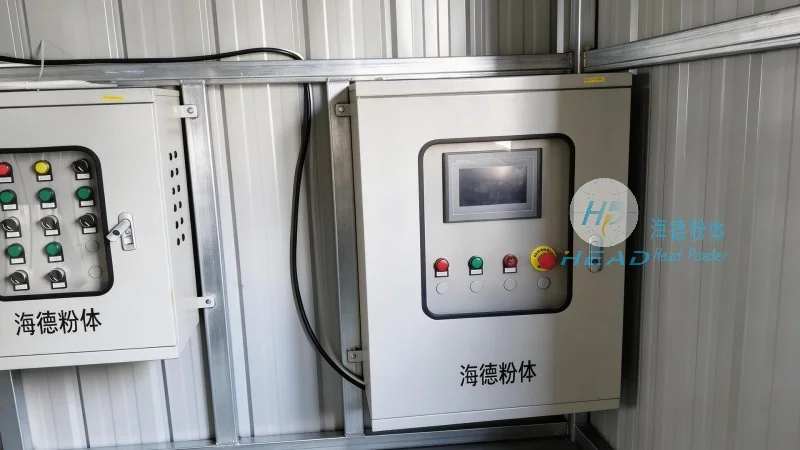
The core principle of pneumatic conveying involves using compressed air or vacuum to transport materials through a pipeline system. In an automatic weighing configuration, this process is enhanced with integrated load cells or sensors that continuously monitor the weight of the material being conveyed. The system typically operates by drawing material from a hopper or storage bin into a conveying line, where it is propelled by air pressure or suction. As the material moves through the pipeline, the weighing unit calculates the mass flow rate, allowing for real-time monitoring and control of the material quantity. This integration ensures that the conveying process is not only efficient but also highly accurate, minimizing material loss and optimizing production throughput.
Key Working Scene Characteristics
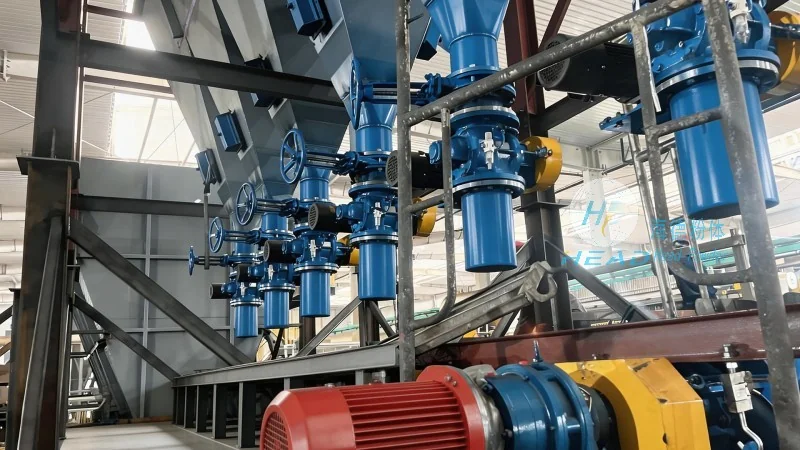
The working scene characteristics of automatic weighing pneumatic conveying machines are tailored to meet the specific demands of diverse industrial environments. These systems are particularly suited for applications where material purity, hygiene, and precise dosing are critical. For instance, in the food and pharmaceutical industries, the equipment is often constructed from stainless steel and equipped with sanitary design features to prevent contamination. In contrast, in the chemical and mining sectors, the machines may be built to withstand harsher conditions, such as corrosive materials or high temperatures. The adaptability of these systems allows them to operate in both continuous and batch mode, making them versatile for different production schedules and operational needs.
Application Scenarios and Industry Adaptability
Automatic weighing material pneumatic conveying machines find extensive applications across multiple industries, demonstrating their versatility and reliability. In the chemical industry, they are commonly used to transport raw materials like powders and granules to reactors or storage tanks, ensuring consistent feed rates for chemical processes. The food processing sector utilizes these systems for handling ingredients such as flour, sugar, and spices, where accurate weighing is essential for maintaining product quality and meeting regulatory standards. The pharmaceutical industry also relies on such equipment for the transport of active pharmaceutical ingredients (APIs) and excipients, where precision and contamination control are paramount. Furthermore, in the mining and mineral processing industries, these machines are employed to convey ore and other bulk materials from processing plants to storage or further treatment facilities, enhancing operational efficiency and reducing manual handling risks.
Technical Advantages and Company Overview
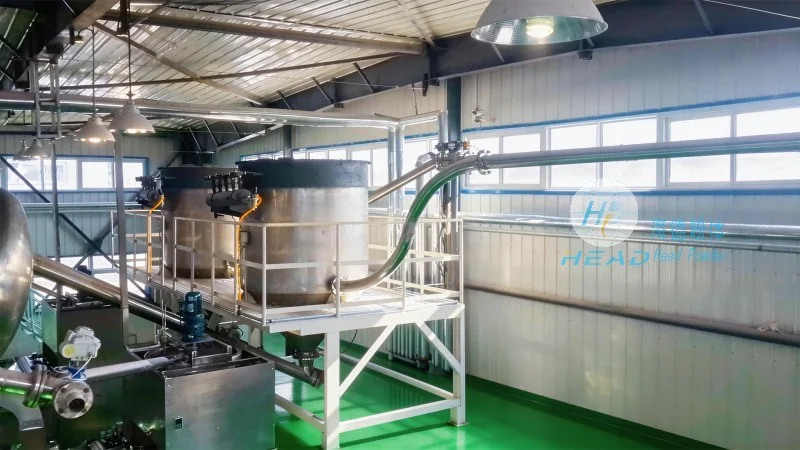
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems. The company's products are engineered to deliver superior performance, with features including high-precision weighing sensors, robust air handling units, and user-friendly control interfaces. HeadPowder's commitment to innovation is evident in its integration of modern technologies, such as digital control systems and real-time data monitoring, which enhance operational visibility and allow for quick adjustments to production parameters. As a company rooted in Shandong, China, HeadPowder leverages local expertise and manufacturing capabilities to deliver reliable, cost-effective solutions tailored to the needs of global clients. The company's focus on quality and customer satisfaction has established it as a trusted partner in the material handling industry, providing durable and efficient automatic weighing pneumatic conveying machines that meet the highest standards of performance and safety.