

Principle and Working Scene Characteristics of a Pneumatic Conveying System for Carbon Black and Coa
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for carbon black and coal powder materials. This article delves into the fundamental principles behind such systems and highlights the key characteristics of their operational environments.
Principle of Pneumatic Conveying Systems
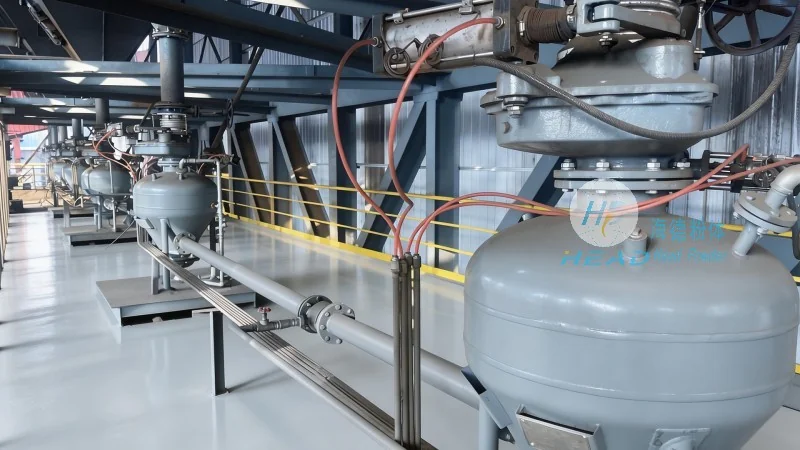
The core principle of a pneumatic conveying system for carbon black and coal powder involves the use of compressed air or gas to transport bulk materials through a pipeline network. The system typically comprises a feeding unit, a conveying line, a control system, and a discharge unit. The material is introduced into the pipeline at a controlled rate, and the air flow propels the particles forward. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and operational costs while ensuring a clean and efficient transfer process.
Working Scene Characteristics
The operational environments for these systems vary based on the specific application and material properties. For carbon black, which is often used in the rubber and plastic industries, the system must handle fine, abrasive particles that can cause wear on equipment. The conveying system is designed with materials resistant to abrasion, such as stainless steel or special alloys, to ensure longevity. In coal powder applications, the system may need to manage larger particle sizes and higher moisture content, requiring adjustments in air pressure and flow rate to maintain consistent performance. The working scenes may include industrial plants, manufacturing facilities, or processing plants where the material is transported from storage to processing units or between different production stages.
System Components and Their Functions
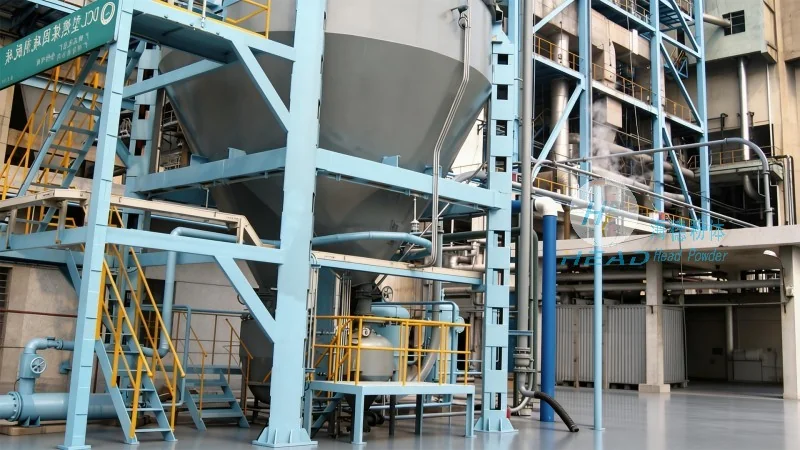
Key components of a pneumatic conveying system for carbon black and coal powder include the material feeder, which controls the flow rate and consistency of the material entering the pipeline; the air compressor or blower, which generates the necessary pressure and volume of air; the conveying pipeline, which transports the material and air mixture; and the control unit, which monitors and adjusts the system parameters in real-time. The discharge unit, often equipped with a cyclone separator or filter, separates the material from the air stream, allowing for clean material collection and air recycling or release.
Advantages of Pneumatic Conveying for Carbon Black and Coal Powder
Compared to traditional mechanical conveying methods, pneumatic systems offer several advantages for handling carbon black and coal powder. These include reduced material degradation due to minimal contact with equipment, improved safety by eliminating the need for manual handling of bulk materials, and enhanced process efficiency through automated control. The systems are also adaptable to varying material characteristics, allowing for customization based on particle size, density, and moisture content. This flexibility makes them suitable for a wide range of industrial applications, from small-scale laboratory operations to large-scale production lines.
Application Examples
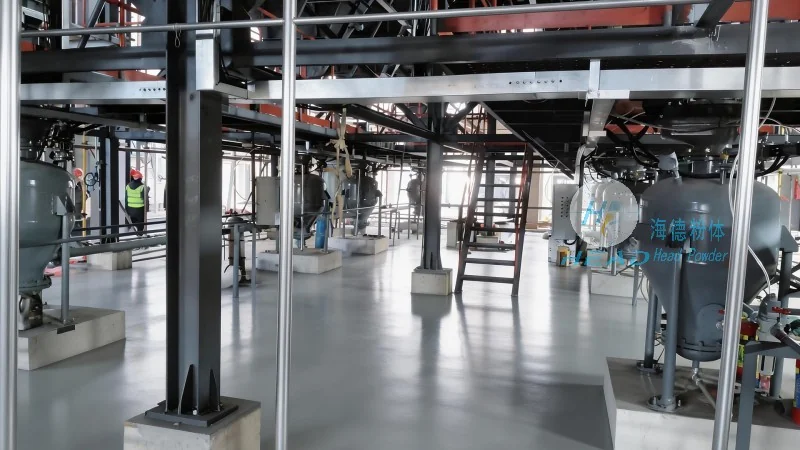
HeadPowder's pneumatic conveying systems are widely used in various industries. In the rubber industry, carbon black is conveyed from storage silos to mixing machines, ensuring consistent color and quality in the final products. In coal-fired power plants, coal powder is transported from coal bunkers to boilers, optimizing fuel usage and reducing operational downtime. Additionally, in chemical processing facilities, coal or carbon black powders are moved between processing stages, supporting continuous production processes and maintaining product integrity.
Conclusion
HeadPowder Engineering Co., Ltd., based in Shandong, China, provides comprehensive solutions for pneumatic conveying systems tailored to the unique needs of carbon black and coal powder materials. By leveraging advanced engineering principles and robust system design, these systems offer efficient, reliable, and cost-effective material transport solutions for industrial applications. The company's expertise in material handling and process optimization ensures that clients receive systems that meet their specific operational requirements, enhancing productivity and reducing maintenance costs.