

Principle and Working Scene Characteristics of Bin Pump Powder Pneumatic Conveying Equipment
Bin pump pneumatic conveying equipment serves as a pivotal technology in modern bulk material handling and transport systems. This equipment is engineered to efficiently move powders through a pipeline network by utilizing compressed air or other gases as the driving force. At the heart of this system is the bin pump, which functions as a positive displacement pump, generating a pressure differential to transport powders from a storage bin to the designated discharge point.
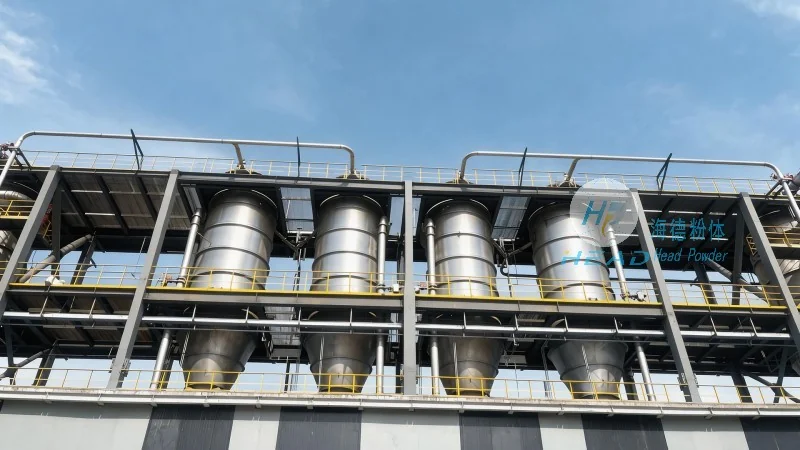
Working Principle of Bin Pump Pneumatic Conveying Systems
The operation of a bin pump system involves sequential steps. Initially, powders are fed into the pump chamber from a storage bin. As the pump's impeller or rotor rotates, it creates a vacuum within the chamber, drawing the powder into the pump. Concurrently, compressed air is introduced into the pump, which then forces the powder through the conveying line to the discharge location. This cycle repeats continuously, ensuring a steady flow of material. The bin pump's versatility allows it to handle a wide spectrum of powder types, from fine powders to bulk materials, making it suitable for diverse industrial applications.
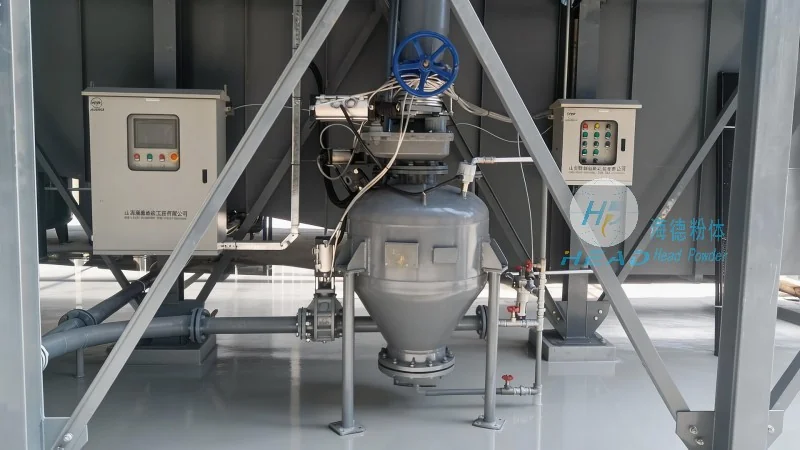
Key Working Scene Characteristics
Bin pump pneumatic conveying systems are widely adopted across various industrial settings due to their distinctive operational advantages. A primary characteristic is their capability to perform long-distance and high-rise conveying, making them ideal for applications requiring material transport over significant distances or vertically. Another notable feature is the system's adaptability to different powder properties, including varying particle sizes, moisture content, and flowability. This flexibility enables seamless integration into existing production lines without substantial modifications.
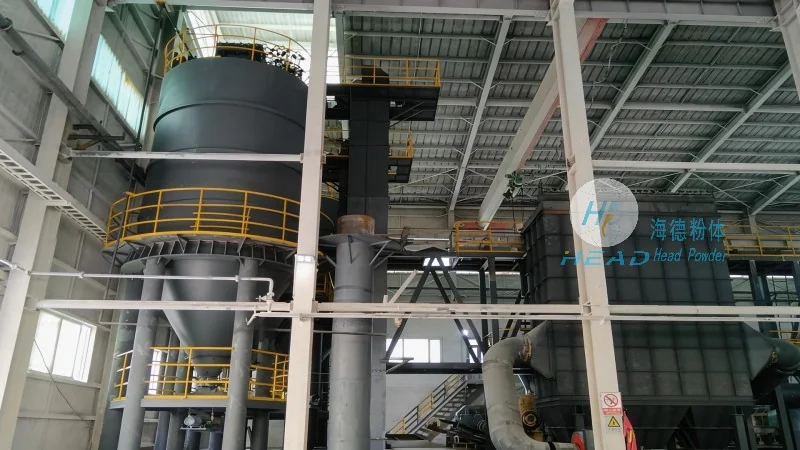
Application Scenarios and Industry Use Cases
Bin pump systems are commonly utilized in industries such as pharmaceuticals, food processing, chemical manufacturing, and mining. In pharmaceutical applications, the equipment ensures sterile and dust-free powder handling, which is critical for maintaining product quality and safety standards. In the food industry, the system is employed for conveying ingredients like flour, sugar, and spices, where hygiene and contamination control are paramount. In chemical manufacturing, the equipment efficiently transports raw materials and finished products, enhancing production efficiency and reducing labor costs. Additionally, in mining operations, bin pumps are utilized to transport ore and other bulk materials from storage silos to processing facilities, improving operational throughput.
Advantages and Technical Specifications
Bin pump pneumatic conveying equipment offers several advantages over traditional conveying methods. One significant benefit is the ability to handle abrasive and corrosive materials without causing wear or damage to system components. The system also provides a closed-loop operation, minimizing dust emissions and environmental contamination, which is essential for compliance with environmental regulations. From a technical perspective, the equipment can operate at pressures ranging from low to high, depending on the conveying distance and material properties. The pump's capacity can be adjusted to meet specific flow rate requirements, ensuring optimal performance for different applications.
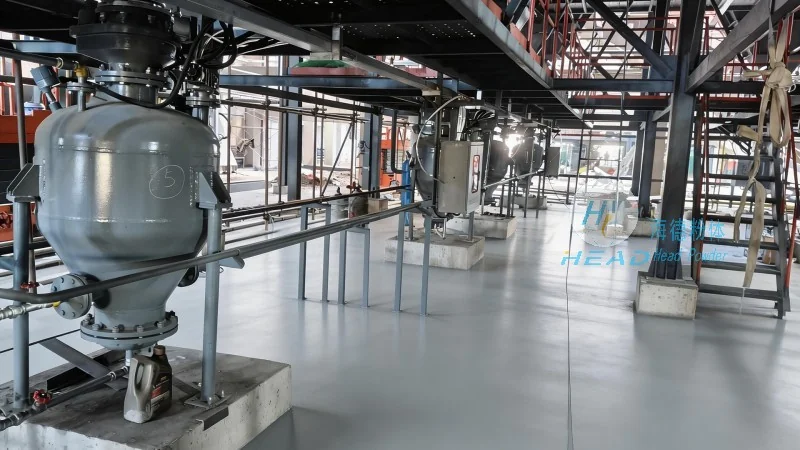
About HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd., a leading manufacturer of bin pump pneumatic conveying systems, is committed to delivering high-quality and reliable equipment for industrial applications. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the powder handling industry. HeadPowder's products are designed to meet the diverse needs of various industries, offering robust solutions that enhance operational efficiency and product quality. The company's headquarters is located in Shandong, China, where it leverages advanced manufacturing techniques and a skilled workforce to produce state-of-the-art conveying equipment.