

Principles and Working Scene Characteristics of Large-Scale Material Handling Conveyors
Large-scale material handling conveyors represent a pivotal technology in contemporary industrial operations, serving as the backbone for efficient material transportation across various sectors. These systems are engineered to move substantial volumes of materials, including powders, granules, and bulk solids, over extended distances with minimal human intervention. The primary objective of such conveyors is to enhance operational efficiency by streamlining material flow, reducing labor costs, and minimizing downtime in industrial processes. By integrating advanced mechanical and control systems, large-scale conveyors provide a reliable solution for industries that demand consistent and high-throughput material movement.
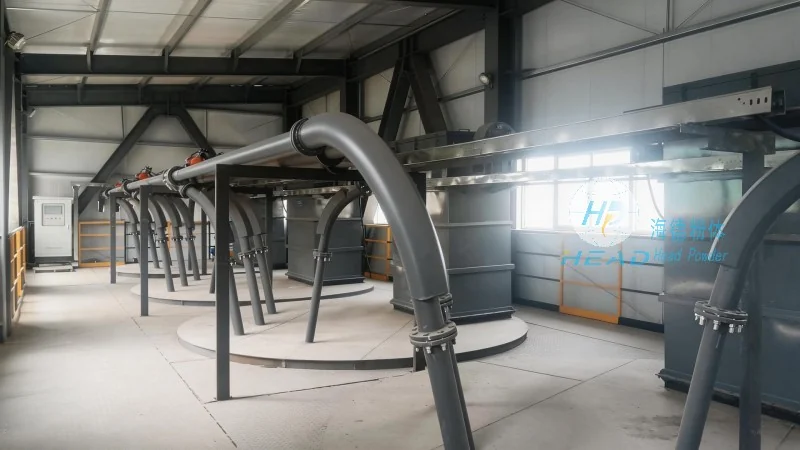
Principles of Operation for Large Material Handling Conveyors
The fundamental principle underlying large-scale material handling conveyors is the conversion of mechanical energy into motion to transport materials. These systems typically employ conveyor belts, which are supported by a series of rollers or idlers, and are driven by electric motors. The drive mechanism, often located at one end of the conveyor, rotates the drive pulley, which in turn pulls the belt and moves the material placed on it. The speed of the conveyor can be adjusted to match the processing requirements, allowing for precise control over material flow rates. Additionally, load sensors and safety switches are integrated into the system to prevent overloading and ensure operational safety. The structural design of the conveyor, including the frame, supports, and drive components, is engineered to handle heavy loads and maintain stability under continuous operation, ensuring long-term reliability and minimal maintenance.
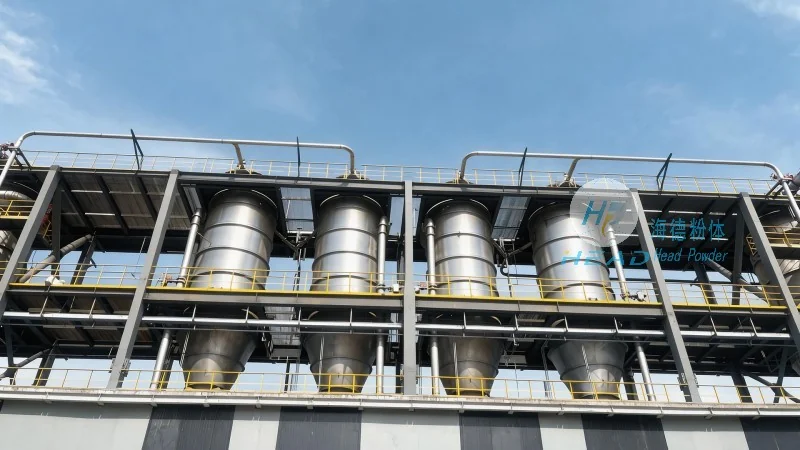
Working Scene Characteristics of Large Material Handling Conveyors
Large material handling conveyors are deployed in a wide range of industrial environments, each characterized by specific operational demands and material types. In manufacturing facilities, these conveyors are crucial for transporting raw materials to production lines and finished products to packaging or storage areas. For example, in automotive manufacturing plants, conveyors move components like metal parts or plastic parts from assembly stations to the next stage of production. In the food processing industry, conveyors are used to transport raw ingredients, such as grains or fruits, to processing lines and finished products to packaging areas, ensuring hygienic and efficient material flow. In logistics and warehousing, large conveyors facilitate the movement of goods between different storage zones, improving inventory management and reducing handling time. The versatility of these systems allows them to adapt to various working conditions, including indoor and outdoor applications, and to handle materials with different properties, such as abrasive or fragile items.
Key Features and Advantages of Large Material Handling Conveyors
Large-scale material handling conveyors offer several key features that contribute to their effectiveness in industrial settings. One of the primary advantages is high throughput capacity, which allows for the continuous movement of large volumes of materials, reducing bottlenecks in production lines. The systems are also designed for durability and longevity, with robust components that can withstand heavy loads and harsh operating conditions. Additionally, modern conveyors incorporate advanced control systems, including programmable logic controllers (PLCs) and sensors, enabling real-time monitoring and adjustment of operational parameters. This integration enhances operational efficiency and allows for predictive maintenance, minimizing downtime and maintenance costs. The flexibility of these systems also allows for customization to meet specific client requirements, such as varying conveyor lengths, widths, and incline angles, ensuring optimal performance in diverse applications.
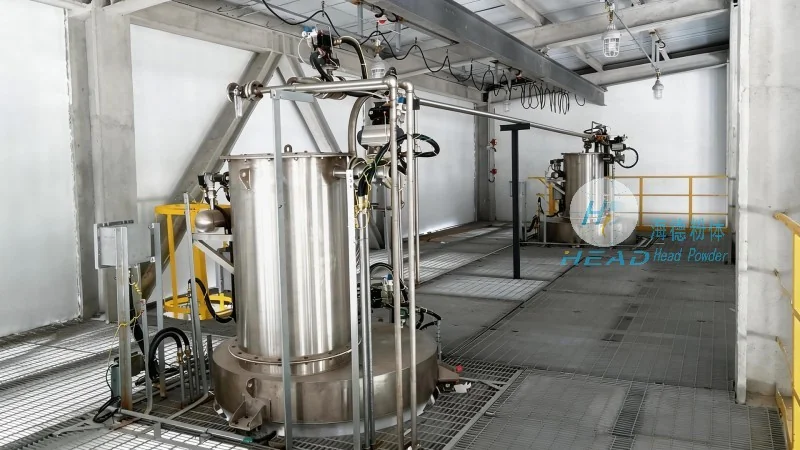
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of advanced material handling solutions. The company specializes in the design, development, and installation of large-scale material handling conveyors tailored to the needs of various industries. With a strong commitment to innovation and quality, headpowder leverages cutting-edge technology to create efficient and reliable conveyor systems that enhance operational productivity. The company's team of experienced engineers and technicians provides comprehensive support, from initial consultation and system design to installation and after-sales service. HeadPowder's products are engineered to meet international standards and comply with safety regulations, ensuring that clients receive high-quality solutions that deliver long-term value. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced production equipment and quality control systems.