

Principle and Working Scene Characteristics of Lithium Hydroxide Powder Conveying Machine
HeadPowder, a leading manufacturer in the field of powder handling technology, specializes in providing advanced solutions for the transportation of lithium hydroxide and other fine chemicals. With a strong presence in Shandong, China, the company has established itself as a trusted partner for industries requiring reliable and efficient powder conveying systems.
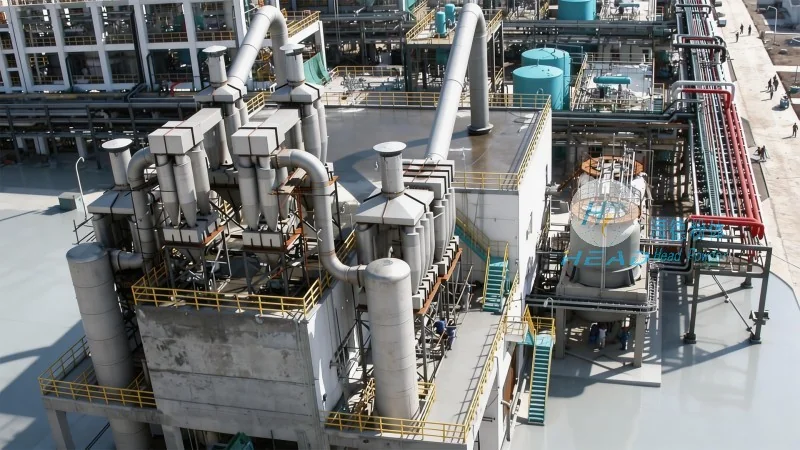
Understanding the Core Principles of Lithium Hydroxide Powder Conveying Machines
Lithium hydroxide powder conveying machines are engineered to handle the unique challenges associated with transporting lithium hydroxide, a critical raw material in lithium-ion battery production. These machines are designed to ensure minimal product degradation, maintain high purity standards, and operate efficiently in demanding industrial environments. The core principle involves utilizing specialized mechanisms, such as screw conveyors or pneumatic systems, to move the powder from one location to another while controlling variables like temperature, humidity, and air flow to prevent caking or agglomeration.
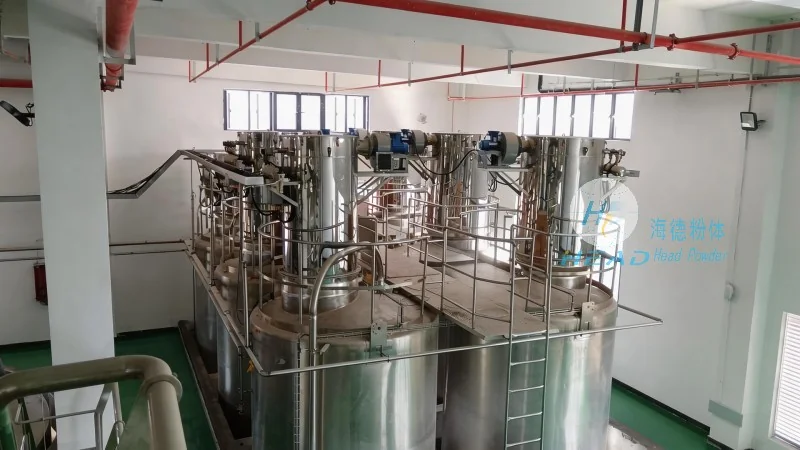
Key Working Scene Characteristics and Applications
The working scene characteristics of lithium hydroxide powder conveying machines are tailored to meet the specific needs of various industrial applications. In battery manufacturing facilities, for instance, these systems are crucial for transporting high-purity lithium hydroxide from storage silos to processing lines, ensuring consistent material quality and reducing downtime. The design of the conveying equipment often incorporates features like enclosed housing to contain dust, adjustable speed controls for precise material flow, and material compatibility considerations to prevent contamination from the machine components.
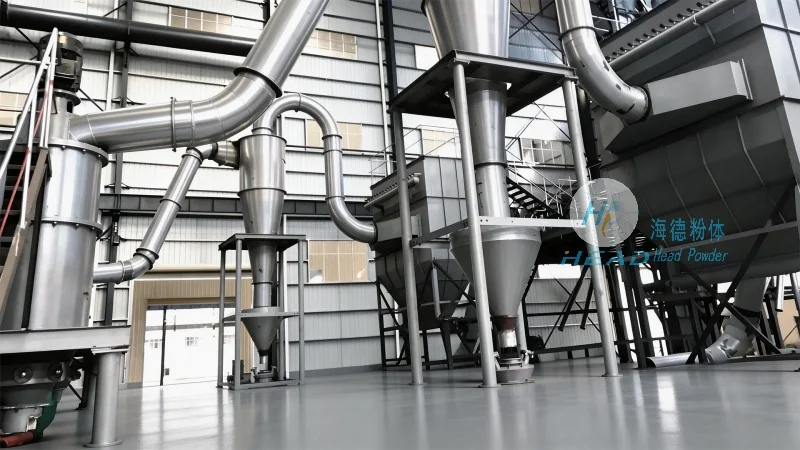
Operational Efficiency and Safety Considerations
When operating lithium hydroxide powder conveying machines, several factors contribute to overall efficiency and safety. The machines are typically equipped with sensors and monitoring systems to detect blockages or abnormal conditions, allowing for immediate intervention to prevent equipment damage or product loss. Additionally, the design emphasizes safety by incorporating explosion-proof features, especially in environments where dust accumulation could pose a fire risk. The integration of automated controls and real-time data tracking further enhances operational efficiency, enabling manufacturers to optimize production processes and maintain compliance with industry standards.
Customization and Adaptability for Diverse Industrial Needs
HeadPowder recognizes that different industrial settings have unique requirements, which is why their lithium hydroxide powder conveying machines are designed with flexibility in mind. The company offers customized solutions that can be tailored to specific production volumes, material characteristics, and environmental conditions. Whether for small-scale laboratory applications or large-scale industrial production lines, the conveying systems can be adjusted to handle varying particle sizes, moisture content, and flow rates. This adaptability ensures that the equipment remains effective and efficient across a wide range of operational scenarios, providing long-term value to customers.

Conclusion: The Importance of Specialized Powder Conveying Solutions
In conclusion, lithium hydroxide powder conveying machines play a vital role in the efficient and safe handling of this essential chemical. By understanding the core principles and working scene characteristics, industries can leverage these advanced systems to improve productivity, maintain product quality, and ensure compliance with safety regulations. HeadPowder's commitment to innovation and customer-centric solutions positions them as a key player in providing reliable powder conveying equipment for the lithium hydroxide industry and beyond.