

Principle and Working Scene Characteristics of Inorganic Salt Powder Conveyors
Inorganic salt powder conveyors are specialized equipment designed to efficiently transport dry, free-flowing inorganic salts across various industrial applications. These systems are engineered to maintain product integrity, ensure consistent flow rates, and operate reliably in diverse working environments. Understanding their core principles and typical operational scenarios is essential for industries that rely on bulk powder handling, such as chemical manufacturing, mining, food processing, and agriculture. The following content explores the fundamental mechanisms of these conveyors and highlights their key working scene characteristics, providing a comprehensive overview of their functionality and practical advantages.
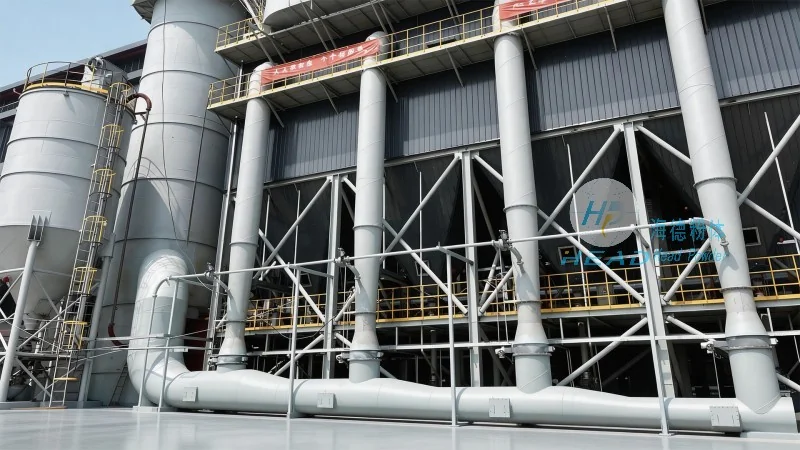
Core Working Principle of Inorganic Salt Powder Conveyors
The operational principle of inorganic salt powder conveyors centers on mechanical or pneumatic systems that facilitate the movement of dry powders. Unlike traditional bulk material handling methods, these conveyors are optimized to minimize particle degradation, prevent agglomeration, and avoid segregation of the salt particles. The primary components include a storage hopper, a conveyor mechanism (e.g., screw, belt, or pneumatic), and control systems for regulating speed and direction. The design emphasizes low friction surfaces and gentle handling to preserve the chemical properties and quality of the inorganic salts. This approach ensures that materials like sodium chloride, potassium chloride, or other industrial salts remain in their original state, ready for downstream processing. The control systems enable precise adjustments to accommodate varying material densities and flow rates, enhancing operational flexibility and efficiency.
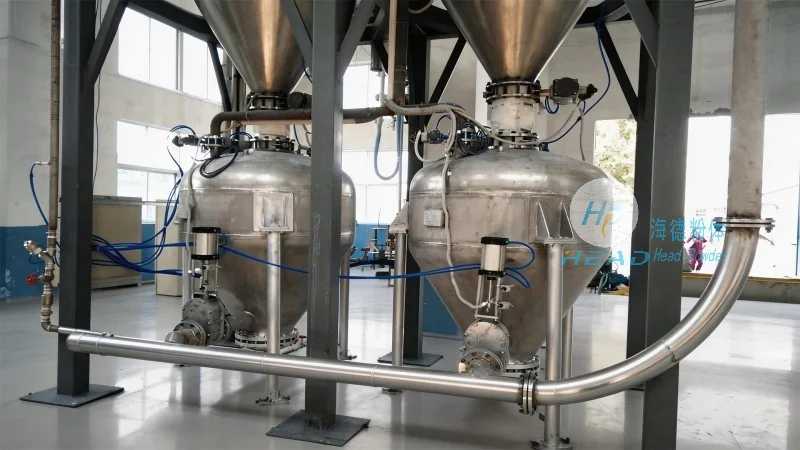
Key Working Scene Characteristics
Inorganic salt powder conveyors are deployed across multiple industrial sectors, each with distinct operational requirements. The working scene characteristics are tailored to meet the specific demands of these environments, ensuring optimal performance and safety. In chemical manufacturing plants, these conveyors are used to transport raw salts to processing units, where they are further refined or combined with other chemicals. The controlled indoor environment necessitates conveyors with high precision and minimal contamination risk. In mining operations, the conveyors handle mined salts from extraction sites to processing facilities, often operating in harsh outdoor conditions. The robust construction, including corrosion-resistant materials and durable components, makes them suitable for such demanding settings. Additionally, in food processing industries, where inorganic salts are used as flavor enhancers or preservatives, the conveyors must adhere to strict hygiene standards. Features like easy cleaning, non-stick surfaces, and compliance with food safety regulations are critical. The working scene characteristics thus vary based on the industry, but all prioritize efficient, safe, and reliable powder transport.
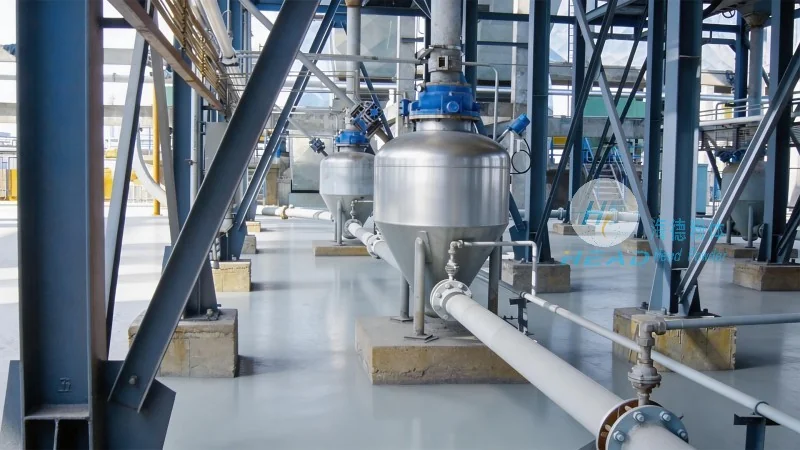
Application Examples and Operational Benefits
Real-world applications of inorganic salt powder conveyors span several industries, demonstrating their versatility and effectiveness. In the pharmaceutical sector, these conveyors transport raw inorganic salts that are key components in drug formulations. Precision and cleanliness are paramount to avoid contamination and maintain product purity. Similarly, in agriculture, inorganic salts are used as fertilizers, and the conveyors efficiently distribute these materials to farms. The ability to handle large quantities and maintain consistent flow rates is essential for meeting agricultural demands. The operational benefits of these conveyors extend beyond transport efficiency. By reducing material handling time and minimizing waste, they enhance overall productivity. Modern designs also prioritize energy efficiency, reducing operational costs and contributing to sustainability goals. The combination of these advantages makes inorganic salt powder conveyors a preferred solution for bulk powder handling in various sectors.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer specializing in advanced powder handling equipment. HeadPowder focuses on innovation and quality, serving as a trusted partner for industries requiring reliable bulk material transport solutions. The company’s inorganic salt powder conveyors are engineered to meet diverse client needs, offering customized designs that enhance operational efficiency and product quality. HeadPowder’s headquarters is located in Shandong, China, where local expertise and resources support the development of cutting-edge technologies. By adhering to international standards and implementing rigorous quality control measures, HeadPowder ensures its products are durable, reliable, and perform optimally in various working environments. The company’s commitment to customer satisfaction and continuous improvement has established its reputation for excellence in the powder handling equipment industry.