

The Principle and Working Scene Characteristics of Quartz Stone Powder Conveying Equipment
Quartz stone powder conveying equipment is a specialized device designed to handle and transport fine powder materials, particularly quartz stone powders, in industrial settings. The efficient operation of such equipment is crucial for maintaining production efficiency and ensuring product quality in various manufacturing processes. This article delves into the fundamental principles behind quartz stone powder conveying machines and highlights the key characteristics of their working environments.
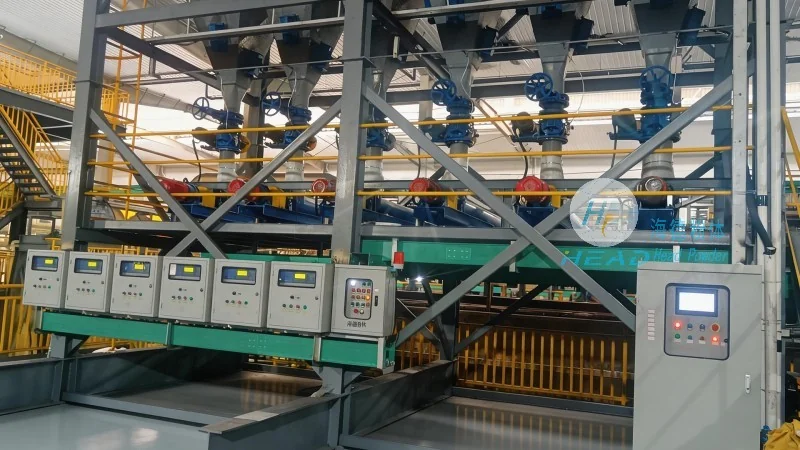
Understanding the Core Principles of Quartz Stone Powder Conveying Equipment
The operation of quartz stone powder conveying machines is based on several mechanical and pneumatic principles that enable the reliable transport of fine powders. One of the primary mechanisms is the use of air pressure or vacuum to move the powder through a pipeline system. This method, known as pneumatic conveying, utilizes compressed air to create a flow that carries the powder particles from the source to the destination. The equipment typically includes components such as a hopper for material storage, a conveyor line, and a control system to regulate the flow rate and pressure. The design of these components is critical to ensure minimal particle degradation and consistent performance.
Another important principle involves the use of mechanical conveyors, such as screw conveyors or belt conveyors, which are often integrated with pneumatic systems to enhance efficiency. These mechanical components help in handling bulk materials and can be particularly useful in scenarios where the powder has a tendency to settle or clog. The combination of pneumatic and mechanical systems allows for versatile handling of quartz stone powders, adapting to different production requirements and material properties. For instance, the equipment can be configured to handle dry or slightly moist powders, ensuring that the material remains in a stable state throughout the conveying process.
Key Working Scene Characteristics of Quartz Stone Powder Conveying Equipment
The working environment of quartz stone powder conveying equipment is characterized by specific conditions that impact its performance and longevity. One of the primary characteristics is the need for a clean and controlled atmosphere to prevent contamination of the powder. This is especially important in industries where the powder is used for high-purity applications, such as in the production of quartz-based materials or in pharmaceutical manufacturing. The equipment is often housed in enclosed systems to minimize exposure to dust and airborne particles, ensuring that the product remains free from impurities.
Another significant characteristic is the requirement for precise control over the conveying process. This includes maintaining consistent air pressure, flow rates, and temperature to prevent issues like clogging or material degradation. The control systems in these machines are typically equipped with sensors and automation features that allow for real-time monitoring and adjustment. This level of control is essential for maintaining product quality and preventing downtime in production lines. For example, in a quartz stone processing plant, the conveying equipment must be able to handle varying particle sizes and densities without compromising the overall efficiency of the process.
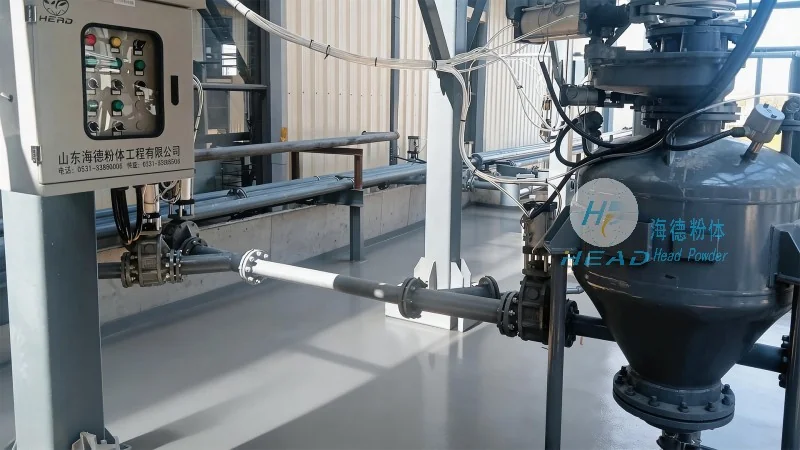
The working scene also involves considerations related to space and layout. Quartz stone powder conveying equipment is often integrated into existing production facilities, requiring careful planning to ensure that the system fits within the available space and does not interfere with other machinery. The design of the equipment, including the length and diameter of the conveyor lines, is tailored to the specific layout of the plant. This integration is crucial for optimizing the workflow and minimizing the need for manual handling of the powder, which can be hazardous and inefficient.
Applications and Industries Utilizing Quartz Stone Powder Conveying Equipment
Quartz stone powder conveying equipment is widely used across various industries that rely on the consistent and efficient transport of fine powders. One of the primary applications is in the manufacturing of quartz-based products, such as glass, ceramics, and electronic components. In these industries, the purity and consistency of the powder are critical to the quality of the final product. The conveying equipment ensures that the powder is transported without contamination or degradation, maintaining the high standards required for these applications.
Another key industry is the pharmaceutical and food processing sectors, where the handling of fine powders requires strict adherence to hygiene and safety standards. The equipment used in these sectors is designed to meet stringent regulatory requirements, including the ability to be cleaned and sanitized easily. This is achieved through the use of materials that are resistant to corrosion and contamination, such as stainless steel, and through the implementation of closed systems that prevent cross-contamination.
In addition, the equipment is utilized in the chemical and mineral processing industries, where quartz stone powders are used as raw materials for various products. The conveying systems in these industries are often part of larger production lines that involve multiple processing steps. The efficiency of the conveying equipment directly impacts the overall productivity of the plant, making it a critical component in the production process.
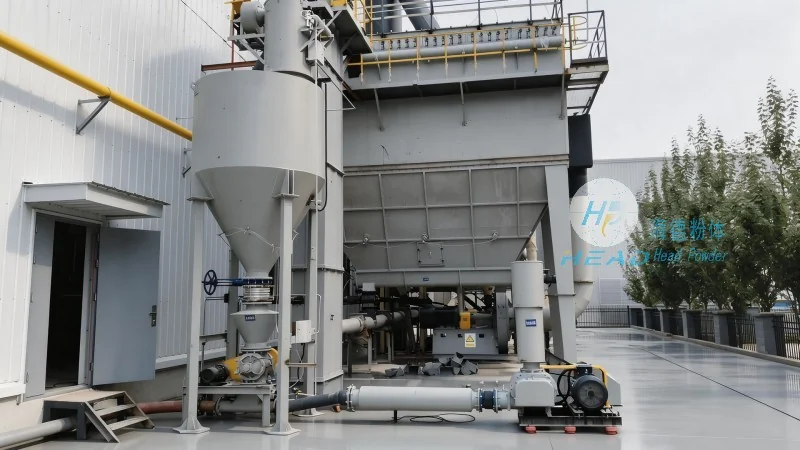
Advantages of Quartz Stone Powder Conveying Equipment
There are several advantages associated with the use of quartz stone powder conveying equipment in industrial applications. One of the main benefits is the ability to handle fine powders efficiently and safely. Unlike traditional methods of manual handling, which are prone to dust exposure and material loss, the conveying equipment provides a closed system that minimizes these risks. This not only improves worker safety but also reduces material waste, leading to cost savings for the company.
Another advantage is the versatility of the equipment. It can be adapted to handle different types of powders, including those with varying particle sizes and moisture content. This flexibility allows manufacturers to use the same equipment for multiple production lines, reducing the need for specialized machinery and simplifying inventory management. The equipment can also be integrated with other processing equipment, such as mixers and grinders, to create a seamless production workflow.
The use of quartz stone powder conveying equipment also contributes to improved product quality and consistency. By maintaining a controlled environment and precise control over the conveying process, the equipment ensures that the powder is delivered in a uniform state, free from clumps or agglomerates. This consistency is crucial for downstream processes, such as mixing and molding, where the quality of the powder directly impacts the final product's properties. Additionally, the equipment helps in reducing the risk of product contamination, which is essential for industries that require high-purity materials.
Conclusion
In conclusion, quartz stone powder conveying equipment plays a vital role in the efficient and safe handling of fine powder materials, particularly in industries that require high-purity and consistent products. The principles behind these machines, combined with their working scene characteristics, make them an essential component in modern manufacturing processes. The equipment's ability to handle various material properties and integrate with other production systems ensures its continued relevance in the industry. As technology advances, the design and functionality of these machines are likely to improve, further enhancing their performance and versatility. For companies operating in industries that rely on quartz stone powders, investing in reliable conveying equipment is a strategic decision that can lead to improved productivity, product quality, and overall operational efficiency.