

Principle and Application Characteristics of Limestone Powder Pneumatic Conveying Equipment
Limestone powder pneumatic conveying equipment is a critical component in industrial material handling, designed to efficiently transport limestone powder through a pneumatic system. This technology offers a reliable solution for moving bulk powders over varying distances, ensuring minimal product degradation and operational efficiency. The equipment operates by utilizing air pressure to move the powder through a network of pipes, making it suitable for applications in mining, cement production, and chemical processing industries.
Principle of Pneumatic Conveying for Limestone Powder
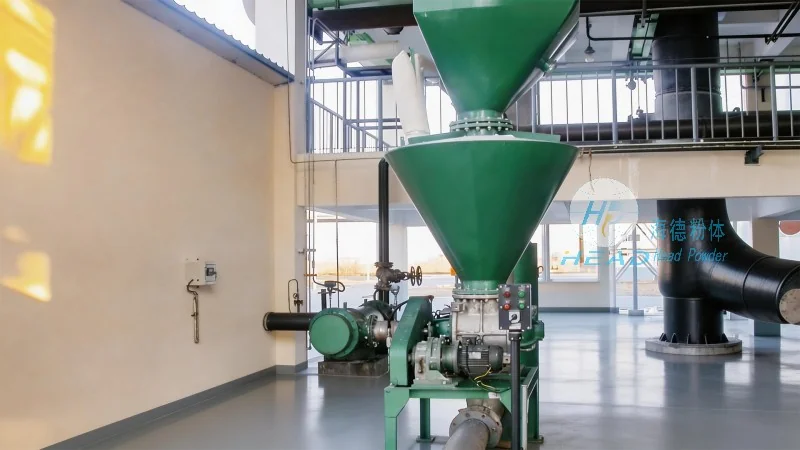
The core principle of limestone powder pneumatic conveying involves the use of compressed air to create a flow that transports the powder particles. The system typically consists of a hopper for material storage, a blower or compressor to generate the air flow, and a pipeline network that delivers the powder to the destination. The conveying process can be categorized into two main types: dilute phase and dense phase, each tailored to different material characteristics and distance requirements. Dilute phase conveying uses higher air velocities to suspend the powder particles, while dense phase employs lower velocities to form a slurry-like flow, reducing the risk of blockages and ensuring smooth operation.
Key Components and Their Functions
Several key components work in tandem to ensure the effective operation of limestone powder pneumatic conveying equipment. The material hopper is the initial storage unit, where limestone powder is fed into the system. A rotary valve or feeder then controls the flow rate of the powder into the pipeline, preventing overloading and maintaining consistent material supply. The blower or air compressor generates the necessary air pressure, with adjustable settings to match the conveying requirements. The pipeline network, often made of stainless steel or other corrosion-resistant materials, transports the powder from the source to the destination. Additionally, filters and cyclones are used to separate the powder from the air, ensuring that the material is delivered in a clean state and the air is returned to the system or released safely.
Application Characteristics in Different Work Scenarios
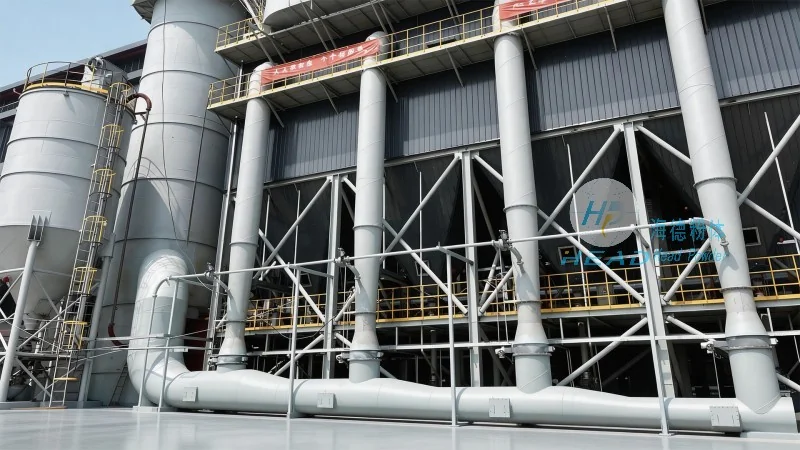
The application characteristics of limestone powder pneumatic conveying equipment vary based on the specific work scenarios and operational needs. In mining operations, the equipment is used to transport limestone from storage silos to processing plants, ensuring a continuous supply of raw material. The system's ability to handle large volumes and maintain consistent flow rates makes it ideal for high-throughput applications. In cement production, limestone powder is a primary raw material, and the pneumatic conveying system ensures that it is delivered to the grinding mills without degradation. The equipment's design allows for integration with existing production lines, minimizing downtime and enhancing overall efficiency. In chemical processing, the system is used to transport limestone powder to reactors or storage tanks, where it is used as a filler or raw material. The flexibility of the pneumatic system allows for adjustments in flow rates and pressure, adapting to the varying demands of chemical processes.
Advantages of Using Limestone Powder Pneumatic Conveying Equipment
There are several advantages to utilizing limestone powder pneumatic conveying equipment in industrial settings. One of the primary benefits is the reduction in material handling costs, as the system eliminates the need for manual or mechanical loading and unloading. The equipment also minimizes product contamination and degradation, as the powder is transported in a closed system, preventing exposure to moisture, dust, or other environmental factors. Additionally, the system offers high efficiency in terms of energy consumption, with adjustable air pressure and flow rates that optimize performance. The compact design of the equipment allows for easy installation in limited spaces, making it suitable for both new and existing facilities. Furthermore, the system provides a safe and reliable method of transporting powders, reducing the risk of dust explosions and other safety hazards associated with traditional material handling methods.
Operational Considerations and Maintenance
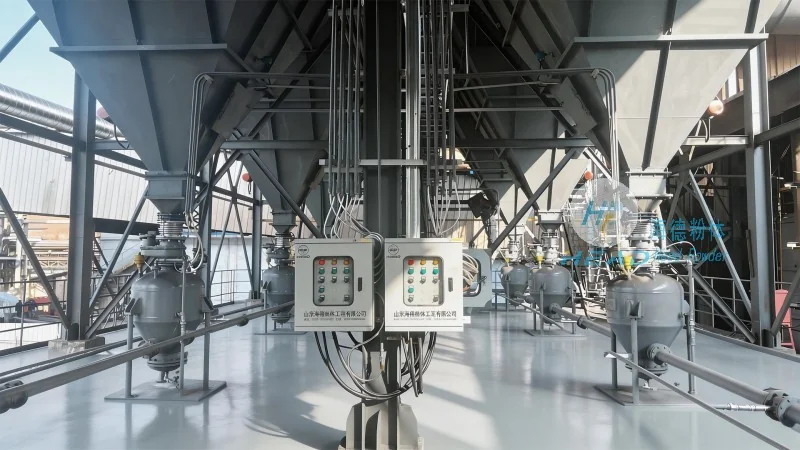
Proper operation and maintenance of limestone powder pneumatic conveying equipment are crucial for ensuring long-term performance and reliability. Regular inspection of the pipeline network is necessary to check for blockages or leaks, which can affect the conveying efficiency. The filters and cyclones should be cleaned or replaced regularly to maintain optimal performance and prevent clogging. The blower or compressor should be checked for proper air pressure and flow rates, with adjustments made as needed to maintain consistent operation. The material hopper and feeder should be inspected for wear and tear, and replaced or repaired as necessary to prevent material leakage or overloading. Additionally, the system should be operated within the recommended parameters, as exceeding the design limits can lead to equipment damage or reduced performance. By following these operational considerations and maintenance procedures, the equipment can provide reliable and efficient service for years.
Conclusion
Limestone powder pneumatic conveying equipment is a vital technology in the industrial sector, offering a reliable and efficient method for transporting bulk powders. The equipment's design and operation are tailored to the specific needs of limestone powder, ensuring minimal degradation and consistent flow rates. With proper operation and maintenance, the system can provide long-term performance and cost savings for industrial applications. As a leading provider of such equipment, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality pneumatic conveying systems that meet the diverse needs of its clients. The company's commitment to quality and customer satisfaction has made it a trusted partner in the industry, providing reliable solutions for material handling challenges.