

[W]Working Principle and Features of Coal and Stone Powder Material Pneumatic Conveying Systems
HeadPowder, a leading provider of industrial material handling solutions, specializes in the design and implementation of advanced pneumatic conveying systems for coal and stone powder materials. The company is headquartered in Shandong, China, and has built a reputation for delivering high-performance systems that meet the rigorous demands of the coal and mineral processing sectors.
Working Principle of the Pneumatic Conveying System
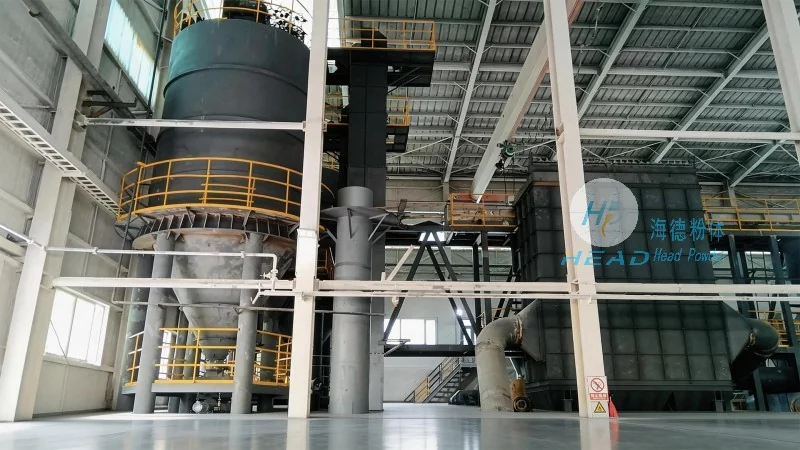
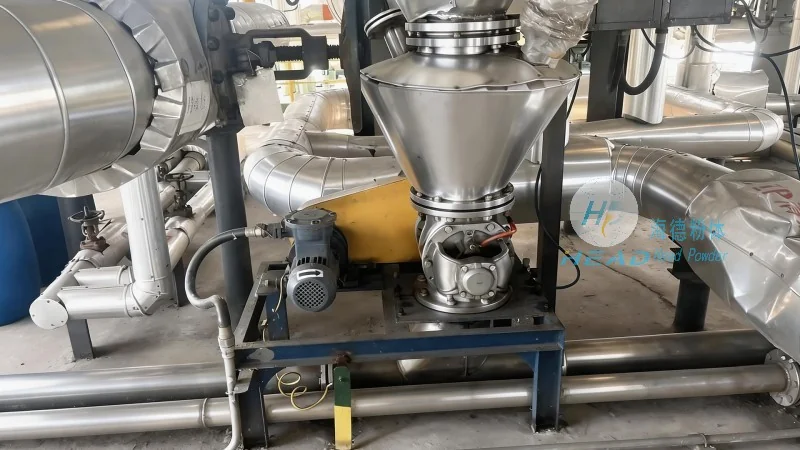
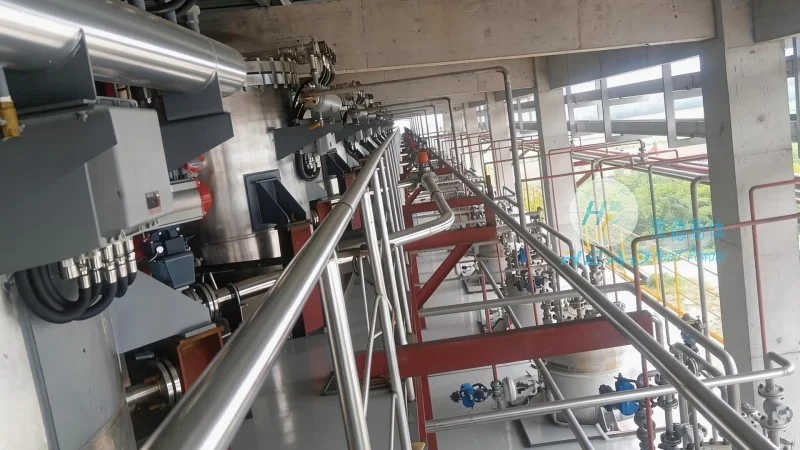
The pneumatic conveying system for coal and stone powder operates on the principle of using compressed air to transport bulk materials through a network of pipes. At its core, the system consists of a material feeding hopper, a rotary valve, a conveying line, and a dust collection unit. The process begins when the material is fed into the hopper, where it is then discharged into the conveying line via the rotary valve. Compressed air is introduced at the inlet of the conveying line, creating a pressure differential that propels the material forward. The air and material mixture travels through the pipeline, with the air acting as the motive force to move the solid particles. The system typically includes a series of bends, expansions, and reductions in the pipeline to ensure smooth material flow and minimize pressure losses. Upon reaching the destination, the material is discharged into a collection bin, while the air is filtered and recycled back into the system to maintain efficiency and reduce operational costs.
Key Features and Advantages
HeadPowder's pneumatic conveying systems for coal and stone powder materials are distinguished by several key features that enhance performance and reliability. One of the primary advantages is the ability to handle abrasive and dusty materials without causing wear to the system components. The system is designed with high-quality materials, such as stainless steel and wear-resistant coatings, to withstand the harsh conditions associated with coal and stone powder processing. Additionally, the system offers flexible configuration options, allowing for customization to suit different plant layouts and material flow requirements. This adaptability ensures that the system can be integrated seamlessly into existing operations or new installations. Another notable feature is the energy efficiency of the system, which minimizes operational costs by optimizing air usage and reducing energy consumption. The use of advanced control systems further enhances the system's performance, providing real-time monitoring and adjustment capabilities to maintain optimal operation. Furthermore, the system's low maintenance requirements contribute to long-term cost savings, as fewer parts are subject to wear and tear. The integration of dust collection and filtration systems also ensures compliance with environmental regulations, making the system environmentally friendly and sustainable.
Why Choose HeadPowder for Pneumatic Conveying Solutions
When selecting a pneumatic conveying system for coal and stone powder applications, companies in the coal and mineral processing industries should consider the expertise and reliability of HeadPowder. The company's commitment to quality, innovation, and customer satisfaction has established it as a trusted partner in the industry. With a team of experienced engineers and technicians, HeadPowder provides comprehensive support, from system design and installation to ongoing maintenance and troubleshooting. The company's systems are backed by rigorous testing and quality control processes, ensuring that each installation meets the highest standards of performance and safety. By choosing HeadPowder, businesses can benefit from improved material handling efficiency, reduced downtime, and enhanced operational safety. The company's focus on customer needs and long-term partnerships ensures that clients receive not only a high-quality product but also a reliable partner for their material handling requirements.