

Working Principle and Characteristics of Bulk Bag Unloading Station for Powder Pneumatic Conveying
HeadPowder, a leading provider in the field of bulk material handling solutions, specializes in advanced systems for efficient powder handling. This article explores the working principle and key characteristics of the bulk bag unloading station for pneumatic conveying, a critical component in modern industrial material processing. The company, based in Shandong, China, offers tailored engineering solutions that enhance operational efficiency and safety in various industrial applications.
Introduction to Bulk Bag Unloading Station for Powder Pneumatic Conveying
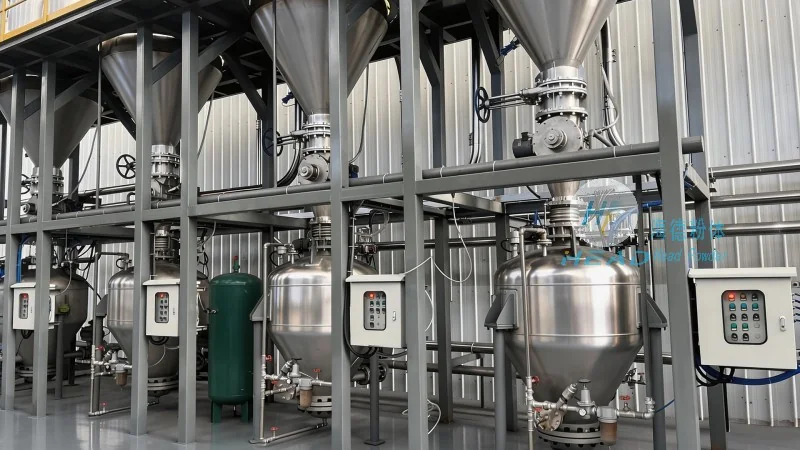
The bulk bag unloading station is a specialized system designed to handle the transfer of powders and granules from bulk bags (also known as FIBCs) into a pneumatic conveying system. This process is essential in industries such as pharmaceuticals, chemicals, food processing, and mining, where bulk materials need to be transported from storage to processing units. The system combines mechanical and pneumatic technologies to ensure a safe, efficient, and controlled transfer of materials, minimizing dust exposure and product contamination.

Working Principle of the Bulk Bag Unloading Station
The operation of a bulk bag unloading station for powder pneumatic conveying involves several key steps. First, the bulk bag is securely positioned on a discharge frame, which is equipped with a discharge spout or valve. The system then uses a combination of vacuum or pressure to create a flow of air that pulls the material from the bag and into the conveying line. The process typically includes pre-conditioning the bag to ensure uniform flow, followed by the actual discharge operation. The air flow is carefully controlled to maintain a consistent material velocity, preventing blockages and ensuring smooth transfer. The system may also incorporate features such as bag emptying aids, like vibration or agitation mechanisms, to facilitate the complete removal of material from the bag. After the bag is emptied, the system can automatically reset for the next bag, enhancing operational efficiency.
Key Characteristics and Advantages
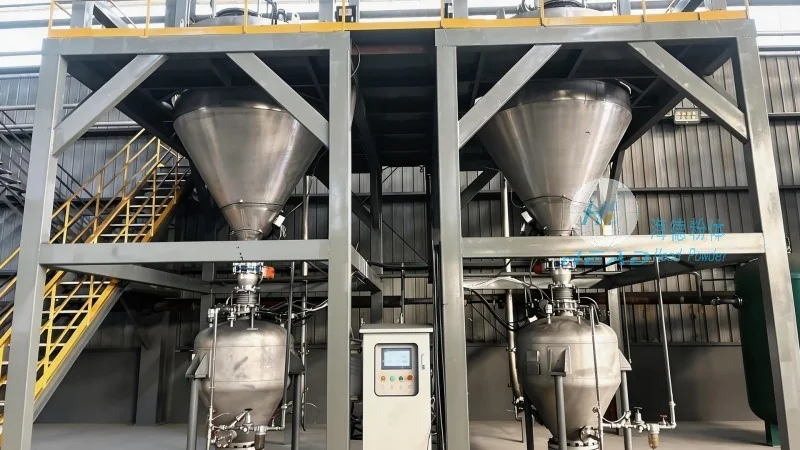
The bulk bag unloading station for powder pneumatic conveying offers several distinct characteristics that make it a preferred choice in industrial applications. One of the primary advantages is its ability to handle a wide range of powder types, from fine powders to coarse granules, without causing segregation or degradation. The system is designed to minimize dust generation, which is crucial for maintaining a safe working environment and complying with environmental regulations. Additionally, the station provides high transfer efficiency, with minimal material loss and consistent flow rates, which helps in reducing operational costs and improving overall productivity. The modular design of the system allows for easy integration with existing pneumatic conveying networks, making it a flexible solution for various plant layouts. Another key characteristic is the enhanced safety features, including automatic shut-off valves and dust collection systems, which protect operators from exposure to hazardous materials. The system also offers user-friendly controls, allowing operators to monitor and adjust the discharge process with ease, ensuring optimal performance under different operational conditions.
Application and Industry Impact
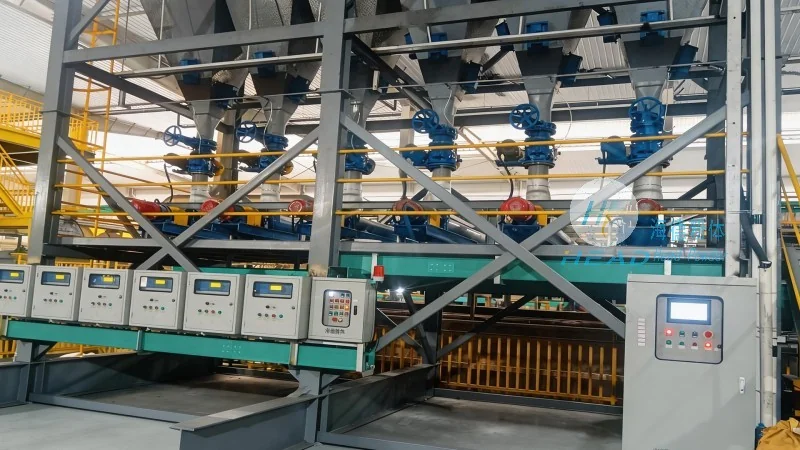
The bulk bag unloading station for powder pneumatic conveying is widely used in industries where bulk materials are stored and processed. In the pharmaceutical industry, for example, the system ensures that powders are transferred under sterile conditions, maintaining product quality and safety standards. In the chemical industry, the system handles various chemicals, including hazardous materials, with precision and safety. The food processing industry benefits from the system's ability to handle food-grade powders, ensuring compliance with food safety regulations. The mining industry uses the system to transfer raw materials from bulk bags to processing equipment, improving the efficiency of material handling operations. Overall, the bulk bag unloading station plays a vital role in enhancing the productivity and safety of industrial material handling processes, contributing to the overall efficiency of manufacturing operations.
Conclusion
HeadPowder's bulk bag unloading station for powder pneumatic conveying is a sophisticated solution that combines advanced engineering with practical design to meet the demands of modern industrial applications. By understanding the working principle and key characteristics of this system, industries can make informed decisions about implementing efficient material handling solutions. The system's ability to handle diverse materials, maintain high transfer efficiency, and ensure safety makes it an essential component in various industrial settings. As a leading provider, HeadPowder continues to innovate and develop solutions that enhance operational performance and support the growth of industrial sectors worldwide.