

Working Principle and Features of Large-Scale Powder Conveyors
Large-scale powder conveyors are essential equipment in various industrial sectors, including pharmaceuticals, chemicals, food processing, and mining. These systems are designed to efficiently transport bulk powders over long distances with minimal product degradation. Understanding the working principle and key features of such machinery is crucial for optimizing operational efficiency and ensuring product quality.
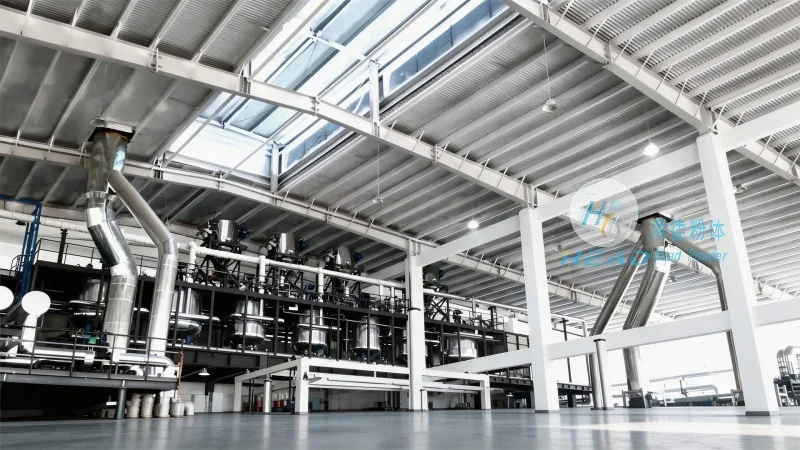
Working Principle of Large-Scale Powder Conveyors
The operation of large-scale powder conveyors typically involves several core components and mechanisms. The primary working principle revolves around the use of a continuous conveying medium, such as a belt, screw, or pneumatic system, to move powders from the source to the destination. In many industrial applications, these conveyors employ a combination of mechanical and pneumatic forces to achieve effective material handling.
For instance, in a belt conveyor system, the powder is fed onto a moving belt, which transports it through the system. The belt is driven by a motor, and the speed can be adjusted to control the flow rate. This method is particularly effective for transporting dry, free-flowing powders without causing excessive particle breakage. In contrast, screw conveyors use a rotating screw to push the material forward, making them suitable for handling cohesive or sticky powders. Pneumatic conveyors, on the other hand, utilize compressed air to transport powders in a sealed pipeline, which is ideal for dusty or hazardous materials.
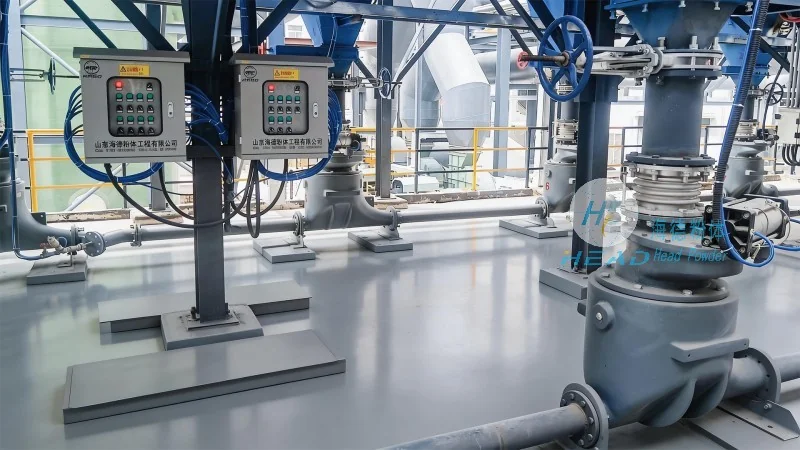
Key Features of Large-Scale Powder Conveyors
Large-scale powder conveyors are characterized by several key features that enhance their performance and adaptability. One of the most significant features is their ability to handle high volumes of material with consistent throughput. This is achieved through robust construction and efficient drive systems, ensuring reliable operation even under heavy load conditions. Additionally, these conveyors are designed for durability, with components made from corrosion-resistant materials to withstand harsh industrial environments.
Another important feature is the flexibility in system configuration. Modern large-scale powder conveyors can be customized to suit specific process requirements, including vertical or inclined transport, multiple transfer points, and integration with other processing equipment. This adaptability allows for seamless integration into existing production lines, minimizing downtime and maximizing productivity. Furthermore, advanced control systems are often incorporated into these conveyors, enabling precise control over speed, pressure, and material flow, which is critical for maintaining product quality and preventing contamination.
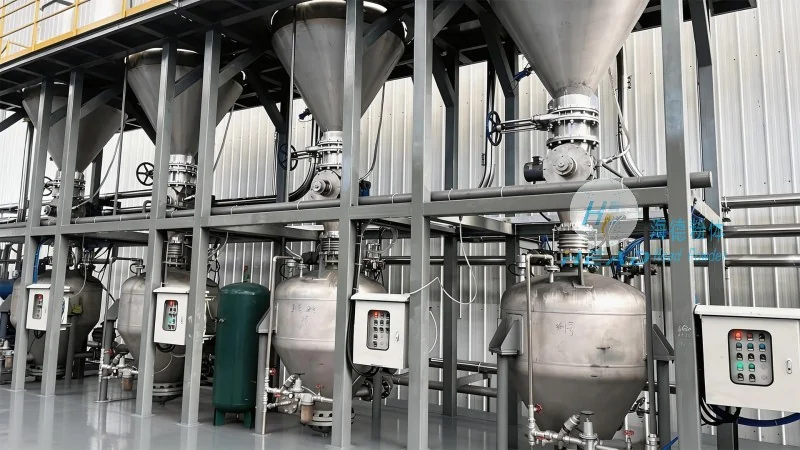
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer of large-scale powder handling systems, specializes in providing high-quality, customized conveyor solutions. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner in the industry. HeadPowder's products are engineered to meet the stringent requirements of various applications, ensuring reliable performance and long service life. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled personnel.
Applications and Benefits of Large-Scale Powder Conveyors
Large-scale powder conveyors find extensive applications across multiple industries. In the pharmaceutical sector, they are used for transporting active pharmaceutical ingredients (APIs) and excipients with strict contamination control measures. In the chemical industry, these systems handle various powders, including raw materials and intermediates, ensuring safe and efficient processing. The food processing industry also relies on large-scale powder conveyors for handling ingredients like flour, sugar, and spices, maintaining hygiene standards and preventing cross-contamination. In mining operations, these conveyors are used to transport ore and other bulk materials from extraction sites to processing facilities, improving operational efficiency and reducing labor costs.
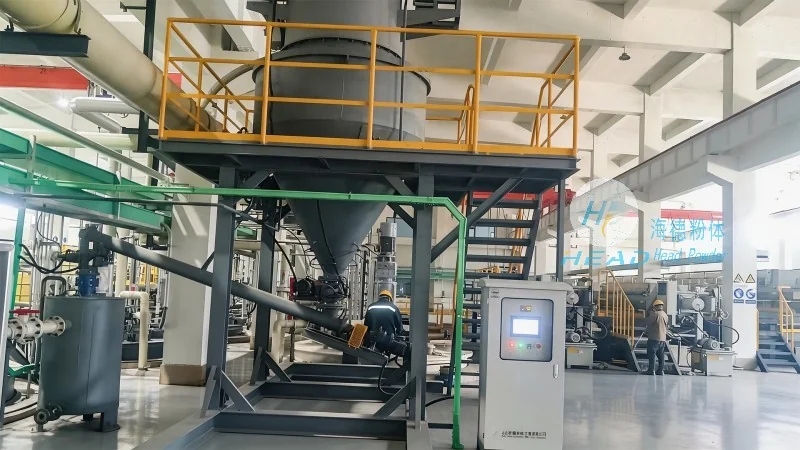
The benefits of using large-scale powder conveyors extend beyond just material transport. These systems contribute to improved safety by reducing manual handling of powders, which minimizes the risk of dust explosions and occupational health hazards. Additionally, they enhance process efficiency by automating material movement, allowing for continuous production without interruptions. The consistent flow of materials also helps in maintaining product quality by preventing segregation and ensuring uniform composition. Furthermore, the energy efficiency of modern large-scale powder conveyors reduces operational costs, making them a cost-effective solution for long-term industrial use.
Conclusion
In conclusion, large-scale powder conveyors are sophisticated systems that play a vital role in modern industrial operations. Their working principle, which combines mechanical and pneumatic forces, enables efficient and reliable transport of bulk powders. The key features, including high capacity, durability, flexibility, and advanced control, make these conveyors suitable for diverse applications. As a leading manufacturer, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide tailored solutions that meet the evolving needs of the industry. By understanding the working principle and features of such machinery, businesses can optimize their operations, enhance product quality, and achieve greater efficiency in their production processes.