

Working Principles and Features of Dust-Free Powder Handling Systems
Efficient and safe powder handling is crucial in industries such as pharmaceuticals, food processing, and chemical manufacturing. Dust-free powder transport systems, like those offered by Shandong HeadPowder Engineering Co., Ltd., utilize advanced technology to ensure minimal particle release and maintain a clean environment. This article explores the working principles and key characteristics of these systems, providing insights into their operational efficiency and practical applications.
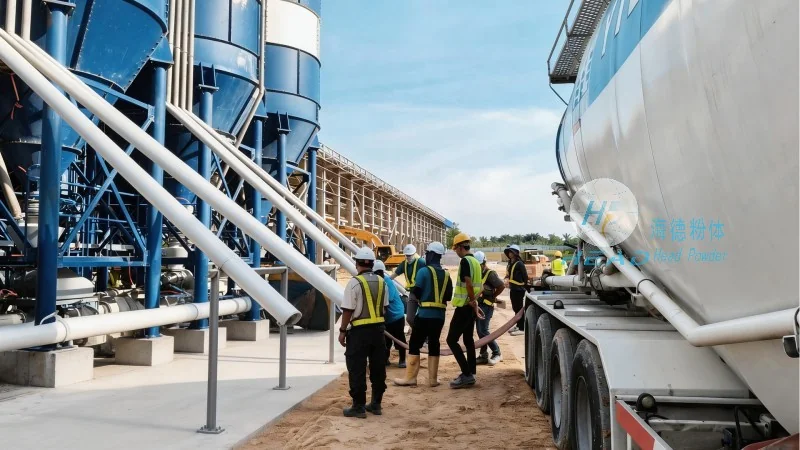
Company Introduction: HeadPowder
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized equipment for powder handling and transportation. With a strong focus on innovation and quality, the company has established itself as a trusted partner in industries requiring stringent cleanliness standards. HeadPowder’s solutions are designed to meet the unique demands of various applications, ensuring reliable and efficient powder movement while maintaining a dust-free environment.
Working Principles of Dust-Free Powder Transport
The core of dust-free powder handling systems lies in the principles of air-assisted transportation. These systems typically operate on one of two main mechanisms: positive pressure (blow) and negative pressure (suction). Positive pressure systems use compressed air to push powder through a sealed pipeline, while negative pressure systems draw powder into the system using a vacuum. Both methods are engineered to minimize particle dispersion and maintain a controlled airflow, preventing dust from escaping into the surrounding environment.
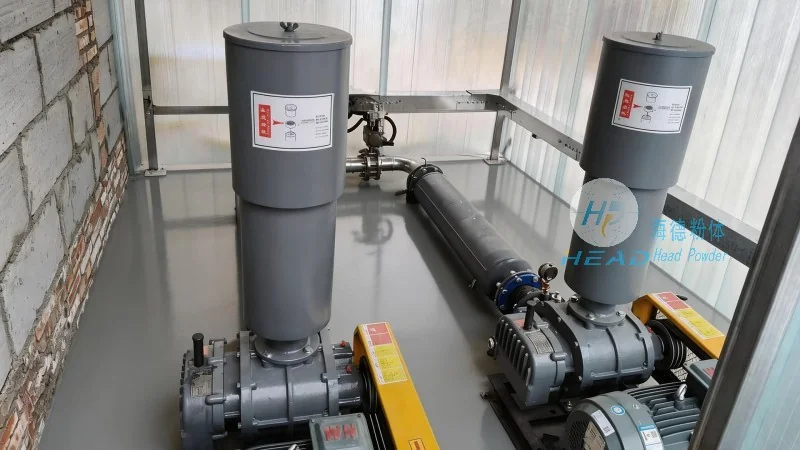
In a typical positive pressure setup, a blower or compressor supplies compressed air to a hopper or storage container. The air then forces the powder through a series of pipes, often equipped with special valves and elbows to ensure smooth flow. This method is ideal for applications where the powder needs to be transported over longer distances or through complex layouts. Negative pressure systems, on the other hand, use a vacuum pump to create a low-pressure zone that draws powder from the source into the system. The powder is then carried by the induced airflow through the pipeline to the destination. Both approaches rely on precise control of air pressure and flow rates to maintain consistent performance and prevent system blockages.
Key Features of Dust-Free Powder Handling Systems
Dust-free powder transport systems from HeadPowder are characterized by several distinct features that enhance their performance and reliability. One of the most significant advantages is the ability to maintain a clean environment, which is critical in industries where contamination can have severe consequences. The sealed design of these systems prevents dust particles from escaping, reducing the risk of inhalation or environmental contamination. Additionally, the systems are designed for high efficiency, with minimal energy consumption and low maintenance requirements.
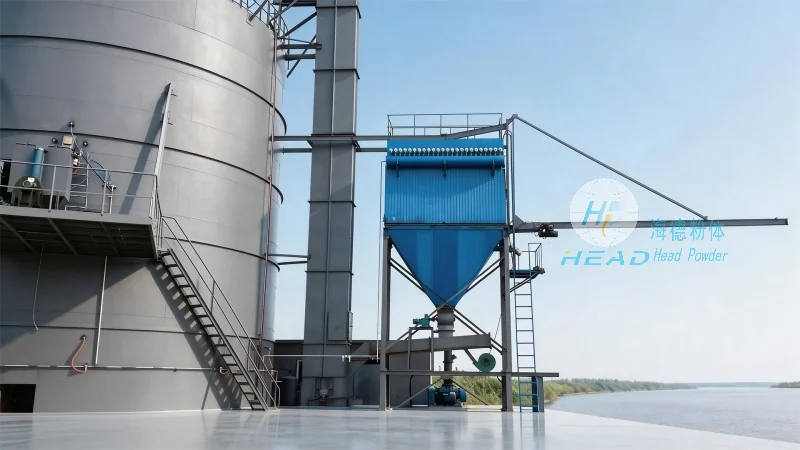
Another key feature is the versatility of the equipment. HeadPowder’s systems can handle a wide range of powder types, from fine powders like pharmaceuticals to bulk materials such as chemicals. The adjustable airflow and pressure settings allow for customization to suit different powder characteristics and application requirements. This flexibility makes the systems suitable for various processes, including mixing, dosing, and packaging. Furthermore, the robust construction of the components ensures durability and long-term operation, even in demanding industrial environments.
Operational Advantages and Applications
The implementation of dust-free powder handling systems offers numerous operational advantages. By eliminating the need for manual handling and reducing the risk of dust exposure, these systems improve workplace safety and compliance with regulatory standards. The automated nature of the process also increases productivity and reduces labor costs. In addition, the consistent flow of powder ensures stable production processes, minimizing downtime and product variability.
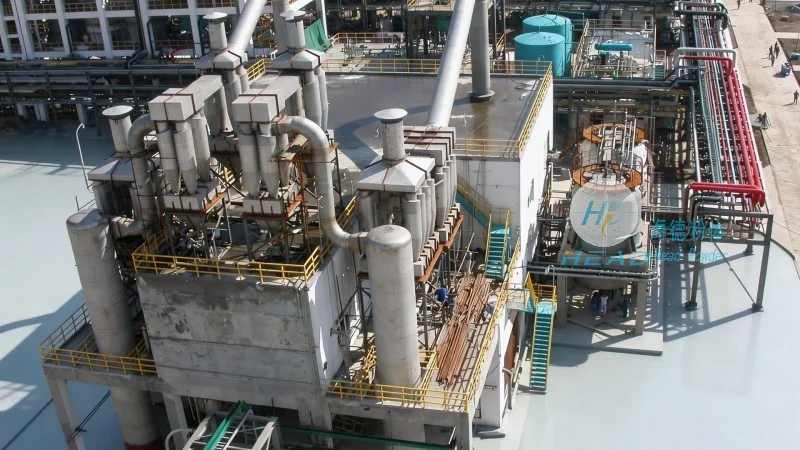
HeadPowder’s dust-free powder transport solutions are widely used in pharmaceutical manufacturing, where the purity of powders is paramount. The systems help maintain the integrity of active pharmaceutical ingredients (APIs) and prevent cross-contamination between different batches. In the food industry, these systems ensure that powders like spices and flavorings are handled hygienically, meeting strict food safety regulations. Similarly, in chemical and material processing, the systems enable the safe and efficient transport of hazardous powders, reducing the risk of accidents and environmental impact.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides advanced dust-free powder handling systems that combine efficient working principles with robust features to meet the demands of modern industries. By leveraging air-assisted transportation and maintaining a sealed environment, these systems ensure safe, clean, and reliable powder transport. With their expertise and commitment to quality, HeadPowder continues to be a leading provider of solutions that enhance operational efficiency and compliance in powder handling applications.